
Custom CNC Fabrication Essentials for High-Quality Parts at Lower Cost
Ten decisions that set the price of a machined part, in the order they affect it. Written for design engineers and sourcing teams who need to hold tolerance without paying for tolerance nobody uses.
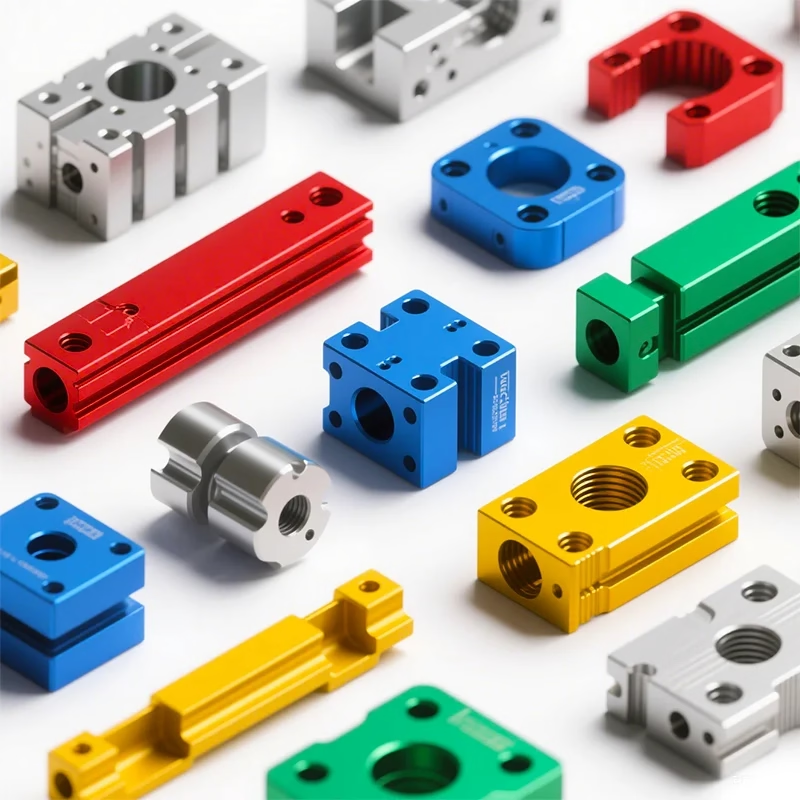
Where the money actually goes
Cost is decided on the drawing, not on the machine. These ten essentials are ordered by how much each one moves the final price.
Spend tolerance where it functions, then simplify the geometry
A drawing where every dimension carries ±0.005 mm tells the shop nothing about intent. It also forces slow passes, extra setups and more scrap on features that never mattered. Mark the functional surfaces instead: sealing faces, bearing seats, mating interfaces, dowel bores. Those earn the tight band. Outer shells, clearance holes and non-mating pockets can usually sit at ±0.1 mm or wider.
The saving is not in the tight feature. It is in everything around it. When the shop knows the hinge pocket needs ±0.01 mm and the housing wall does not, it can rough the wall with a large cutter and finish only the pocket. Cycle time drops, and so does the scrap rate.
Design for manufacturability is the second essential and it works the same way. Replace deep narrow cavities with two shallower parts. Use standard drill sizes and standard thread depths so no custom tool has to be ground. Round internal corners to a radius the cutter can actually reach.
A bracket with several undercuts is a common example. Machined as one piece it needs five-axis work and a long-reach tool. Split into two plates that bolt together, it becomes a three-axis job with shorter tools and fewer setups. The assembly adds two fasteners and removes a large share of the machining cost.
- 1Tight only where it seals or locatesFunctional faces get ±0.005–0.01 mm; the rest can breathe.
- 2Corner radius ≥ cutter radiusSharp internal corners need EDM or a much smaller tool.
- 3Standard drills and threadsNo custom tooling, no extra setup, no waiting.
Pick material by requirement, not by habit, and choose the right axis count
Material choice shows up twice in the quote: once as stock cost, once as machining time. 6061-T6 covers most brackets, housings and fixtures. Moving to 7075 only pays when the strength or the fatigue life is needed. In stainless, 303 machines faster than 304, and 304 faster than 316. If the part never sees chlorides or a wash-down environment, 316 is money spent for nothing.
Titanium and Inconel cut slowly, wear tooling and need rigid setups. They are correct for high-temperature or weight-critical parts and wrong as a default. The same logic applies to plastics: ABS and POM machine cleanly and hold decent tolerance, while PEEK is reserved for high temperature or aggressive chemistry.
Axis count follows the geometry. A part with features on four faces of a prismatic block belongs on a four-axis mill or a mill-turn center, where one setup finishes several faces. Contoured surfaces, impeller blades, deep angled ports and organic housings belong on simultaneous five-axis, where the tool stays normal to the surface and hand finishing disappears.
Do not put a three-axis part on a five-axis machine out of caution. The setup is longer and the hourly rate is higher. Match the machine to the feature, and split the part into two operations if that is cheaper than one complex setup.
- 1Aluminium 6061-T6Default for housings, brackets, fixtures, heat sinks.
- 2Aluminium 7075Use when strength or fatigue life is the constraint.
- 3Stainless 303 vs 316303 for speed; 316 only when corrosion demands it.
- 4Titanium and InconelSlow feeds, short tool life, higher cost per part.
Material and machine pairing for common part types
A starting point, not a rule. The final call depends on load, environment and finish.
| Part type | Typical material | Suggested setup |
|---|---|---|
| Enclosure, bracket, cover | Aluminium 6061-T6 | 3-axis or 4-axis, ±0.05 mm |
| Bearing housing, seal seat | Aluminium 6082, steel 1045 | Mill-turn, ±0.01 mm on bores |
| Impeller, blade, duct | Aluminium 7075, Ti-6Al-4V | Simultaneous 5-axis |
| Valve body, manifold | Stainless 316L, brass C36000 | 4-axis plus mill-turn |
| Chemical or high-temp part | PEEK, Inconel | 3-axis, slow feeds, Ra 1.6 μm |
| Long frame, rail, beam | Aluminium 5083, steel A36 | 3-axis up to 4,000 mm |
| Shaft with cross holes | Steel 4140, 17-4PH | Mill-turn, one setup |
| Thin-wall sensor body | Aluminium 6061, stainless 304 | 5-axis, light finishing passes |
Check the certifications, consolidate operations, prototype before you commit
Certification is not paperwork for its own sake. It tells you which control system the shop runs and whether your industry is already covered. ISO 9001:2015 covers general process control. IATF 16949:2016 is what automotive and EV programs expect. ISO 13485:2016 applies to medical devices, where traceability and validation records are part of the product. ISO 27001:2022 covers information security, which matters when you send CAD files and drawings across borders.
Consolidating operations removes handling, re-clamping and freight between vendors. When milling, turning, finishing and inspection sit in one plant, the datum from the first setup can be reused through the last step. We run 127 high-precision CNC machines across three wholly-owned plants in Dongguan and Singapore, with 16 simultaneous 5-axis machining centers and a maximum processing size of 4,000 mm.
Prototyping is the cheapest place to find a mistake. A first article in the production material and the production process exposes tool access, wall deflection, chatter and fixture problems before tooling is committed. We quote and return a free DFM analysis within 12 hours, and production can start within 24 hours once the design is fixed.
Keep the prototype honest. Machining a prototype from a different alloy, or with the tolerance widened, hides exactly the problems you were paying to find.
- 1Automotive and EVIATF 16949:2016 process control and traceability.
- 2Medical devicesISO 13485:2016 records and validation.
- 3Cross-border filesISO 27001:2022 information security controls.
Inspect in process, plan the finish early, and keep the chain under one roof
Final inspection alone catches bad parts after the time is already spent. In-process checks catch a drifting dimension while the part can still be corrected. Raw material verification, in-process monitoring and a final check before shipment are the three points that matter. We inspect 100% of parts before shipment and can supply reports on request.
Hold ±0.005 mm only on the features that need it, and verify those on the machine or on a CMM while the setup is still live. That is where a re-cut is still possible.
Surface finish belongs in the design review, not in a note added after machining. Bead blasting and tumbling round edges and can move a tight tolerance on a thin wall. Anodizing builds a layer and shifts dimensions on threads and bores. Hardcoat anodizing builds more than a cosmetic coat. If a bore must stay at size, mask it or cut it undersize before coating.
Laser marking has its own limit: minimum character height is 1.5 mm. Smaller text fills in and becomes unreadable, which matters for serial numbers and UDI marks.
A full-process chain manufacturer keeps all of this in one place. From one prototype to 10,000+ part runs, with no minimum order quantity, the part moves through machining, finishing and inspection without changing hands. Fewer handoffs means fewer chances for a datum to shift or a drawing revision to get lost.
- 1AnodizingBuilds a layer; mask or undersize bores and threads.
- 2Bead blasting and tumblingRounds edges; risky on thin walls and sharp tolerance.
- 3Laser markingMinimum character height 1.5 mm for legible marks.
Questions engineers ask before releasing a drawing
How tight a tolerance does custom CNC fabrication actually hold?
We hold ±0.005 mm (±0.0002 in) on features that are specified that way, and finishes down to Ra 0.2–0.8 μm when the surface is called out.
The practical limit depends on the material, the wall thickness and how far the feature sits from the datum. A thin wall in aluminium deflects more than a solid steel block, so the same callout can be routine on one part and difficult on another.
When should I use five-axis instead of three-axis?
Use five-axis when the part has contoured surfaces, features on many faces, or deep angled ports that a three-axis setup cannot reach without repeated re-clamping.
If the part is prismatic with features on two or three faces, a four-axis mill or a mill-turn center is usually faster and cheaper. We can quote both routes so you can compare.
Can I get parts without a minimum order quantity?
Yes. There is no minimum order quantity. We run from a single prototype up to 10,000+ part runs on the same process.
For prototype quantities we still machine in the production material unless you ask otherwise, so the first article reflects what the production part will do.
How do you handle confidential drawings?
Uploads are secure and confidential, and we sign an NDA on request. Our information security system is certified to ISO 27001:2022.
If your program needs restricted access, tell us at the quote stage and we will route the files and the communication accordingly.
What finishes can be applied after machining?
Anodizing in clear, colour, hardcoat and conductive types; electroless nickel, zinc, silver and gold plating; powder coating and black oxide; bead blasting, tumbling, brushing and polishing; laser marking and engraving.
Tell us the finish at the design review. Coatings that build thickness can move a bore or a thread out of tolerance if they are planned after the fact.
What lead time should I plan for?
Quotation and free DFM analysis come back within 12 hours. Production can start within 24 hours once the design is released, and parts ship in 3–5 days for standard work.
Complex five-axis parts and special finishes add time. Send the drawing and we will confirm the schedule with the quote.
Send a drawing and get a DFM read plus a price
Upload your CAD file and we will return a quotation and a free DFM analysis within 12 hours.
12-hour quote±0.005 mm100% inspectionNo MOQ









