GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Vacuum Casting Services

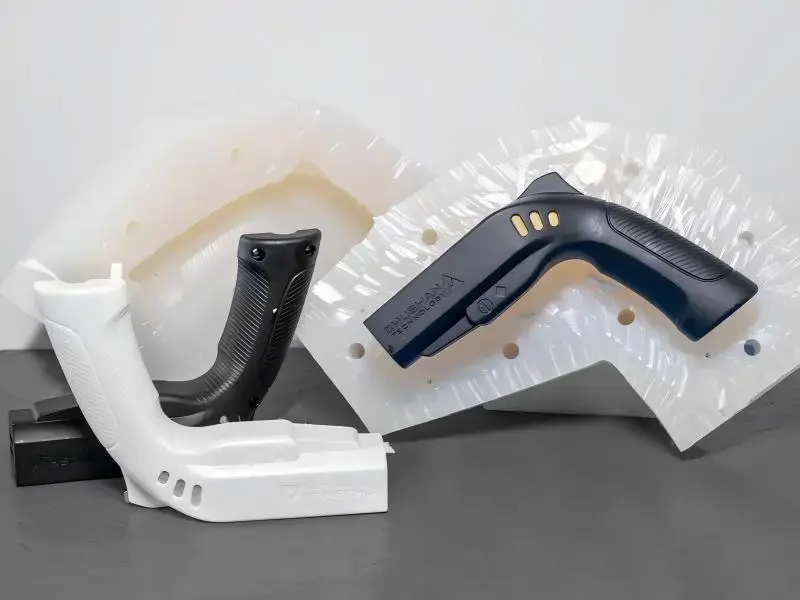
Vacuum Casting for Low-Volume Production Parts

We cast 25 to 50 copies from one silicone mold, using a CNC-machined or 3D printed master. Same two weeks, same batch, no steel tooling. Quote and DFM notes back within 12 hours.

25–50 parts per moldSilicone mold life 20–30 cyclesSTEP · STL · X_T uploadNo minimum order quantity
vacuum-casting-services1
±0.005 mmMachining tolerance on masters
15 yearsCasting and machining since 2011
7,600 m²Across 3 wholly-owned plants
98%+Historical on-time delivery
Where low-volume projects break down

Four Problems This Process Is Meant to Fix

If any of these sound familiar, the tooling route is probably the wrong route.

01

You need 30 units, not 3,000

Injection tooling only pays back above a few thousand parts. Below that, the steel cost sits on your books and the amortized piece price never looks right. A silicone mold spreads a few hundred dollars across a small batch instead.

02

The prototype passed, the pilot build did not

A single machined prototype hides process variance. Ten parts from one silicone mold show whether your fit, snap fits and assembly sequence survive a real batch. Finding that at 30 units is cheaper than finding it at 3,000.

03

The housing needs to look like the production part

Machined surfaces read as machined. Buyers and test users notice tool marks, stepped radii and visible layer lines. Cast urethane comes out of a silicone cavity with a matte or textured skin, so the parts in the room look like the parts you intend to ship.

04

Design is not frozen yet

Every week before design freeze, a steel tool is money at risk. If the rib thickness or the boss location changes, the tool is scrap. Soft tooling absorbs two or three revisions inside the same pilot phase, and the master is re-machined, not re-cut.

The process

How We Cast Urethane Parts in Silicone

A short run of copies pulled from one soft mold, with the master underneath controlling every dimension.

cnc-machining-hdpe
Step 1 and 2

Master Pattern, Then Silicone

The master is the part you already approved. We machine it from aluminium or ABS on our 5-axis centers to ±0.005 mm, or print it when the geometry is organic. Surface finish on the master transfers to every copy, so it gets sanded and sealed before anything else happens.

The master is suspended in a casting box and degassed silicone is poured around it. We cure the block, then cut it open along the parting line and pull the master out. What is left is a cavity that matches the master to a few hundredths of a millimeter.

  • 1
    Master optionsCNC aluminium, CNC ABS, or SLA/SLS printed and polished.
  • 2
    Mold life20 to 30 pulls before the silicone tears at thin features.
  • 3
    Cavity countOne to four cavities per mold, depending on part size.

Get Instant Quote

low volume manufacturing
Step 3 and 4

Casting Under Vacuum

Two-part polyurethane is mixed, degassed and poured into the closed mold inside a vacuum chamber. Pulling the air out before the resin gels is what keeps bubbles out of thick sections and sharp corners. Without the vacuum step, a 15 mm boss fill is where you find voids.

Cured parts come out in 24 to 48 hours depending on the resin, and we de-flash, sand, prime and paint them as a batch. Because every copy comes from the same cavity, part 1 and part 40 measure the same. Shrinkage runs about 0.15 to 0.25 percent, less than injection-molded plastics, so the master is scaled up before machining.

  • 1
    Resin choiceRigid, semi-rigid, rubber-like and transparent grades.
  • 2
    Batch size25 to 50 parts per mold; larger runs use more molds in parallel.
  • 3
    FinishingColor matching, texture, and over-molding onto inserts.

Talk to an Engineer

Choosing a route

Vacuum Casting Against the Alternatives

The right process depends on quantity, tolerance and how settled the design is.

RouteBest fitWhere it loses
Vacuum casting25–50 units, cosmetic covers, pilot buildsSoft mold wears out past 30 pulls
CNC machining1–10 units, tight tolerance, metal partsPiece cost stays high above 20 units
Injection molding3,000+ units, frozen designTool cost and lead time before first part
3D printing1–5 units, fit checks, complex geometryLayer lines, limited resin properties
What we run

Services Around the Casting Cell

Casting rarely travels alone. These are the services we keep in-house so the master, the copies and the finish stay on one schedule.

01

Vacuum Casting

Silicone molds and cast urethane parts, 25 to 50 per mold, in rigid and rubber-like resins.

02

Rapid Prototyping

CNC and printed masters for the casting cell, plus functional prototypes in production-like materials.

03

5 Axis CNC Machining

16 simultaneous 5-axis centers cutting masters and inserts to ±0.005 mm.

04

Custom 3D Printing

SLA, SLS and FDM masters when the geometry is organic or the wall thickness is under 1 mm.

05

Part Surface Finishing

Anodizing, plating, powder coating, bead blasting, polishing and laser marking.

06

Sheet Metal Fabrication

Brackets, housings and chassis so the cast cover arrives with something to bolt onto.

Capability

What the Casting Cell Can Hold

Numbers below come from our own equipment list and inspection records.

ItemRangeNote
Master tolerance±0.005 mmMachined on 5-axis centers
Shrinkage0.15–0.25%Master scaled up before cutting
Parts per mold25–50Thin features wear sooner
Mold life20–30 pullsSilicone, cut open and re-clamped
Cure time24–48 hoursDepends on resin and section
Max part size4,000 mmLimited by casting box and chamber
Surface finishRa 1.6–3.2 μmAs cast, before paint or texture
Inspection100%Dimensional report on request
Why GreatLight

Six Reasons Engineers Keep the Casting Order Here

15Y

Casting and machining since 2011

The same shop cuts the master and pours the mold. No handoff between a machinist and a caster, so the shrinkage factor gets applied once, by the person who measured the part.

±0.005

Masters cut to a real tolerance

16 simultaneous 5-axis centers hold ±0.005 mm on the master. That number is the floor for every copy that comes out of the cavity.

12H

Quote and DFM in 12 hours

Send STEP, STL or X_T files and get a price plus manufacturability notes inside 12 hours. Production can start within 24 hours of approval.

3–5D

Parts ship in 3 to 5 days

Standard cast and finished batches leave in 3 to 5 days. Historical late-delivery probability sits under 2 percent.

1→10K

No minimum order quantity

One prototype or a 10,000-part run, same intake. The route changes, the paperwork does not.

4×ISO

Four certifications in place

ISO 9001, IATF 16949, ISO 13485 and ISO 27001. Uploads stay confidential and an NDA is available on request.

127High-precision CNC machines
150Technicians on staff
3Wholly-owned plants
99.99%Qualification rate
What we deliver

Parts and Programs We Run

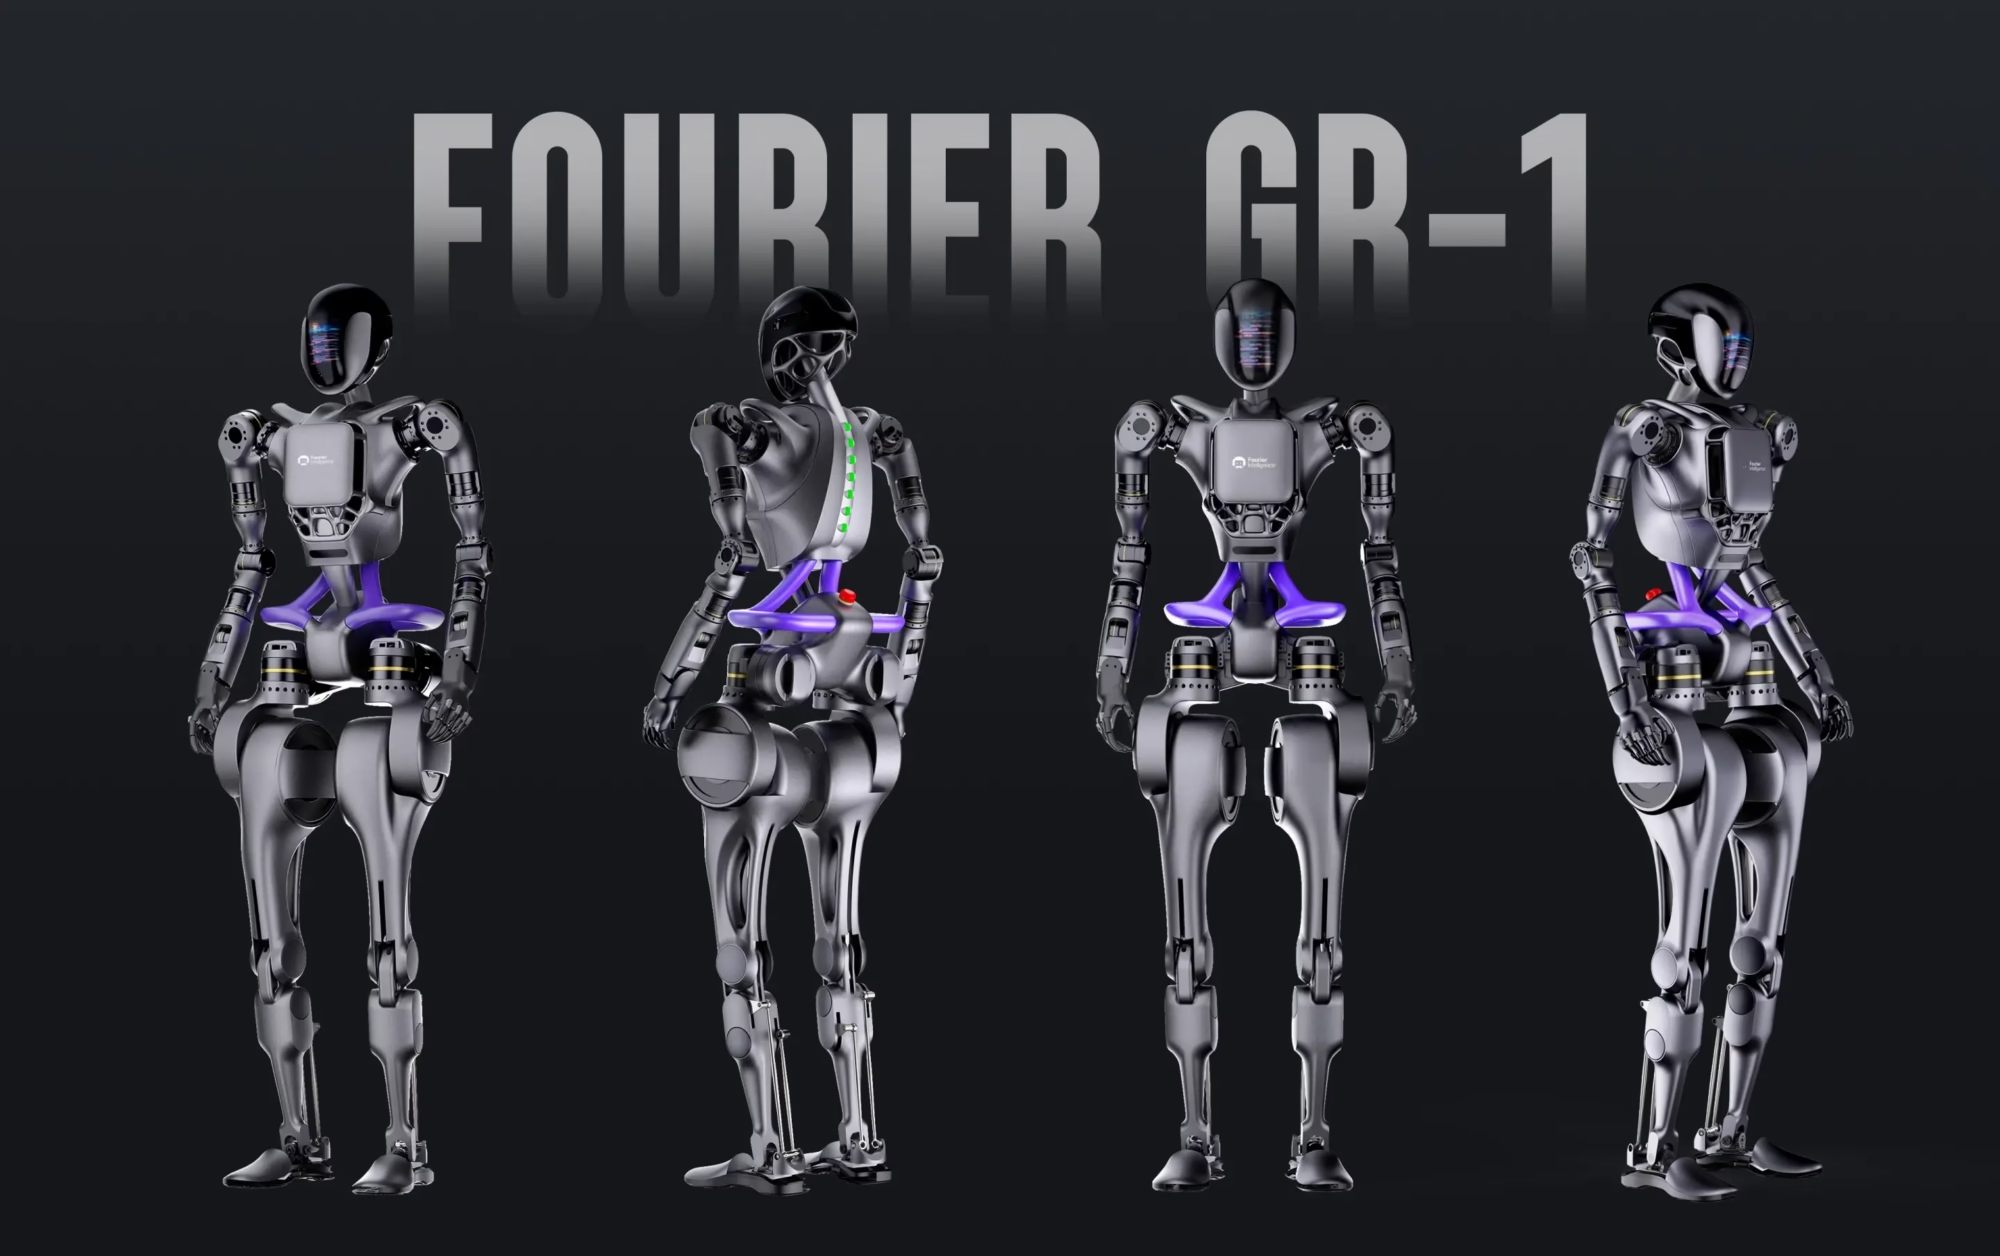
GreatLight Specializing In Humanoid Robot Components

Robotics covers

Cable-routed housings and joint covers cast in semi-rigid urethane, then painted to match the production color.

  • 25–50 per mold
  • Wall to 1.5 mm
  • Painted batch
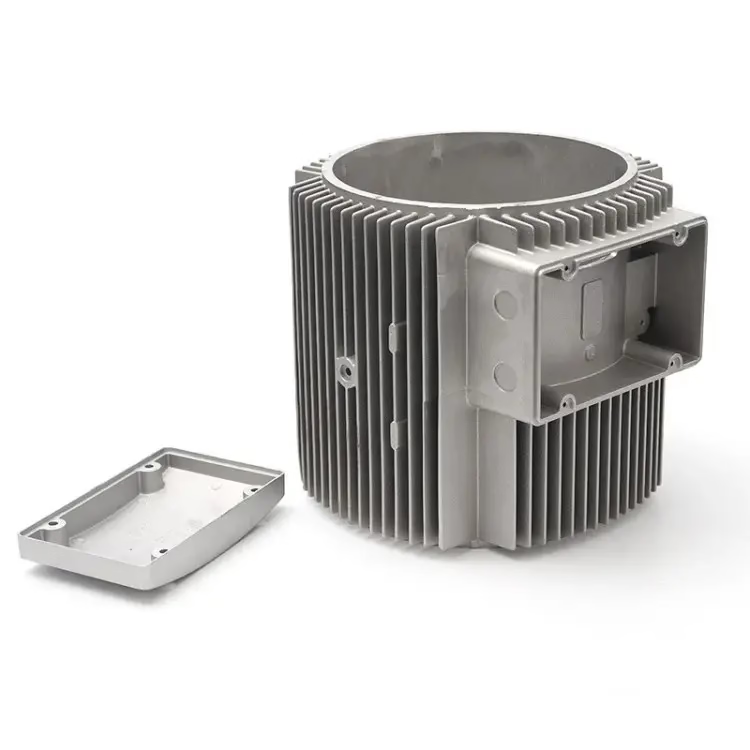
die-casting-technology

Automotive interior trim

Pilot-build bezels and clips cast from a CNC master, checked against the mating part before the batch is released.

  • 0.15% shrinkage
  • ±0.005 mm master
  • 100% inspection
GreatLight CNC Machining Factory

Medical device enclosures

Smooth, cleanable surfaces on small enclosures, molded over metal inserts so the threads are metal, not resin.

  • ISO 13485
  • Insert molding
  • Deburred and cleaned
GreatLight CNC Machining Compliance Center

Electronics housings

Thin-wall covers with molded standoffs, cast in a flame-rated resin and laser marked after finishing.

  • Thin walls
  • Laser marked
  • Batch matched
FAQs

Questions Engineers Ask Before Ordering

How many parts can one silicone mold produce?

Plan for 25 to 50 pulls. The limit is not the resin; it is the silicone tearing at sharp corners, thin ribs and deep bosses.

If your part has 1 mm walls or a 40 mm deep pocket, expect the lower end and budget a second mold for a 50-piece run.

What tolerance can the cast parts hold?

Dimensional tolerance tracks the master, which we machine to ±0.005 mm. Cast copies typically land within ±0.1 mm on stable features.

Long thin parts warp more than they shrink. If a 300 mm cover needs to stay flat, we add a fixture or cast it in a more rigid resin.

Which resins are available?

Rigid, semi-rigid, rubber-like and transparent polyurethanes, plus grades with higher heat deflection for under-hood or electronics use.

Tell us the service temperature and whether the part needs to flex. Resin selection matters more than mold design for drop performance.

How do I prepare my CAD for casting?

Send STEP, STL, X_T, IGES or native SolidWorks and we handle the rest. Draft of 1° to 2° on vertical faces helps release from the silicone.

Avoid undercuts that lock the part in the cavity. If they are functional, we cut the mold in more than two pieces.

Can you match a paint color or texture?

Yes. We prime and paint to a supplied color reference, and texture can be molded in from the master or added as a sprayed finish.

Send the reference with the order. Color matching on cast urethane is done by eye against your sample, not by a spectrophotometer reading.

How do cast parts compare to injection molding on cost?

Below a few hundred units, casting wins because there is no steel tool. Above a few thousand, injection molding wins because the piece price drops hard.

The crossover sits around 200 to 500 parts for most enclosure-sized geometry. We will tell you when the numbers flip.

What files and information do you need for a quote?

3D CAD, quantity, resin preference if you have one, surface finish, and any color or texture reference.

A drawing with critical dimensions speeds up the DFM notes. Without one, we quote on the model alone.

How do you handle confidentiality?

Uploads are secure and confidential, and we sign an NDA on request before files change hands.

ISO 27001 covers how we store and move customer data inside the company.

Send the Model, Get a Casting Quote in 12 Hours

Upload your CAD and we return a price plus DFM notes within 12 hours. No minimum order quantity, from one part to a full pilot batch.

12-hour quote100% inspectionNo minimum order quantityNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC