
01
Tooling eats the budget
A hard die or soft tool costs more than the parts themselves when you only need 200 pieces. That money never comes back if the design changes after the first fit check.
Run 1 to 10,000 parts on 127 CNC machines. No minimum order quantity, no soft-tool investment up front. Quotation and DFM analysis arrive within 12 hours.

These four failures show up again and again on pilot builds and bridge orders.
A hard die or soft tool costs more than the parts themselves when you only need 200 pieces. That money never comes back if the design changes after the first fit check.
The quote comes back with a 1,000-piece minimum, or a setup charge that doubles the unit price. Engineering builds stall while purchasing argues over volume.
Parts arrive dimensionally close but not on print. Slots run 0.1 mm tight, hole positions drift, and assembly needs hand rework to close.
A design change means a new tool, a new setup sheet and another two weeks of waiting. The schedule absorbs the hit, not the supplier.
Cut directly from billet or plate. No tool amortization, no volume threshold.
GreatLight runs 127 high-precision CNC machines across three wholly-owned plants, with 16 simultaneous 5-axis machining centers, 16 mill-turn centers and 12 four-axis mills. A single setup can reach five faces, so hole patterns, pockets and angled features stay in one coordinate frame instead of five.
Maximum processing size is 4,000 mm. Travel options cover 4,000 × 400 × 150 mm for long extrusions and rails, 750 × 1,150 × 550 mm for plate work, and 500 × 500 × 450 mm for compact housings. A Ø400 mm rotary table handles round parts that need continuous indexing.
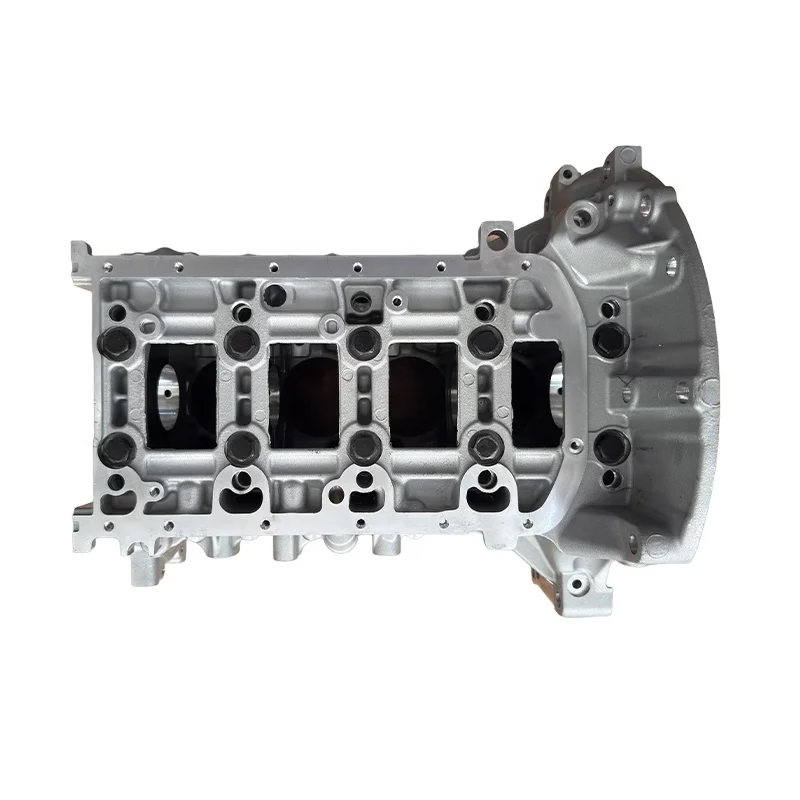
Tolerances hold at ±0.005 mm (±0.0002 in) on critical features. Surface finish runs from Ra 0.2–0.8 μm on sealing faces to Ra 1.6–3.2 μm as-machined on brackets. Every part gets raw material check, in-process monitoring and a final inspection before shipment, with reports on request.
Finishing stays under the same roof: anodizing in clear, colour, hardcoat or conductive; electroless nickel, zinc, silver and gold plating; powder coating and black oxide; bead blasting, tumbling, brushing and polishing; laser marking down to 1.5 mm character height. Qualifying four separate vendors costs more time than the run itself.
Match the method to the batch size and the geometry, not to habit.
| Quantity | Recommended route | Why |
|---|---|---|
| 1–20 parts | 5-axis CNC from billet | No tooling cost, design changes stay cheap |
| 20–500 parts | CNC with shared fixtures | Unit price falls, setup already amortized |
| 500–5,000 parts | Vacuum casting or die casting | Tool cost spread across a larger batch |
| 5,000–10,000+ parts | Die casting plus CNC finishing | Lowest unit cost at stable geometry |
| Sheet metal enclosures | Sheet metal fabrication | Faster than machining thin panels |
Simultaneous five-axis cutting for complex geometry, undercuts and five-face work in a single setup.
Three-axis, four-axis and mill-turn centers covering prismatic parts and turned shafts.
Machined and printed prototypes for fit checks, before any tool is cut.
Silicone tooling for 20 to 500 urethane parts when CNC unit price gets too high.
Aluminium and zinc die casting for housings once the design is frozen.
Anodizing, plating, powder coating, blasting and laser marking in the same plant.
| Item | Specification |
|---|---|
| Quantity range | 1 to 10,000+ parts, no minimum order quantity |
| Tolerance | ±0.005 mm (±0.0002 in) on critical features |
| Surface finish | Ra 0.2–0.8 μm fine, Ra 1.6–3.2 μm as-machined |
| Maximum part size | 4,000 mm, travel to 4,000 × 400 × 150 mm |
| Materials | Aluminium, stainless, steel, copper, titanium, PEEK, HDPE |
| Quotation | Within 12 hours, with free DFM analysis |
| Production start | Within 24 hours of drawing release |
| Delivery | Parts ship in 3–5 days |
Six figures engineers and buyers check before awarding a pilot build.
Fifteen years of short-run work across aerospace, automotive, medical and robotics programs.
Capacity spread across three wholly-owned plants in Dongguan and Singapore.
Held on critical features and verified by 100% inspection before shipment.
Quotation plus free DFM analysis inside half a day of receiving the files.
Measured across past production orders, not a forward-looking promise.
ISO 9001:2015, IATF 16949:2016, ISO 13485:2016 and ISO 27001:2022.
Brackets, housings and fixtures before hard tooling is committed.

HDPE and aluminium components for pilot lines and spares.
Instrument bodies and fixtures in stainless and titanium.
End-effector plates and gearbox housings at low quantity.
Anything from one part to roughly 10,000 pieces where hard tooling has not been justified yet. Below about 500 pieces, CNC from billet usually beats a die because there is no tool cost to recover.
Above that, we compare the CNC unit price against vacuum casting or die casting and tell you where the crossover sits for your geometry.
No. We quote single prototypes and 10,000-piece runs on the same form.
A one-piece order carries a higher unit price because setup is not shared, and we state that plainly in the quote rather than hiding it in a line item.
Quotation and DFM analysis come back within 12 hours. Production can start within 24 hours of drawing release.
Typical parts ship in 3–5 days. That depends on material availability, finishing and inspection scope, so the quote lists the actual window for your parts.
±0.005 mm (±0.0002 in) on critical features. General dimensions follow the drawing's title block tolerance.
Surface finish ranges from Ra 0.2–0.8 μm on sealing faces to Ra 1.6–3.2 μm as-machined. Tell us which features are functional and we concentrate inspection there.
Yes, and that is the main reason to machine rather than tool up early. A revised pocket or moved hole costs a new program and setup, not a new die.
Send the updated model and we re-quote the affected operations only. Fixtures already built for unchanged features stay in use.
Uploads are secure and confidential. An NDA is available on request before you send files.
We hold ISO 27001:2022 for information security management, which covers how drawings, models and process data are stored and accessed.
Aluminium 6061, 7075, 2024 and ADC12; stainless 303, 304, 316L, 17-4PH; steel 1018, 4140, 4340; copper and brass C110, C36000; titanium TC4; plastics including POM, PEEK, PA and HDPE.
Inconel and magnesium AZ31B or AZ91D are available for parts where weight or heat resistance drives the choice.
Raw material check, in-process monitoring and final inspection on 100% of parts before shipment.
Inspection reports are issued on request. If you need first article inspection or a specific report format, say so at quote stage.
Upload a STEP file and we return pricing plus a free DFM analysis. No minimum order quantity, from one prototype to 10,000 parts.
12-hour quoteNo minimum order quantity100% inspectionNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.