GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Three-Axis Milling

Precision 3 Axis CNC Machining Services

Three-axis milling for flat, prismatic and hole-dense parts, held to ±0.005 mm with 100% inspection before shipment. Send a STEP file and get a quote plus free DFM analysis within 12 hours.

±0.005 mm27 three-axis machinesRa 0.8–1.6 μmNo MOQ
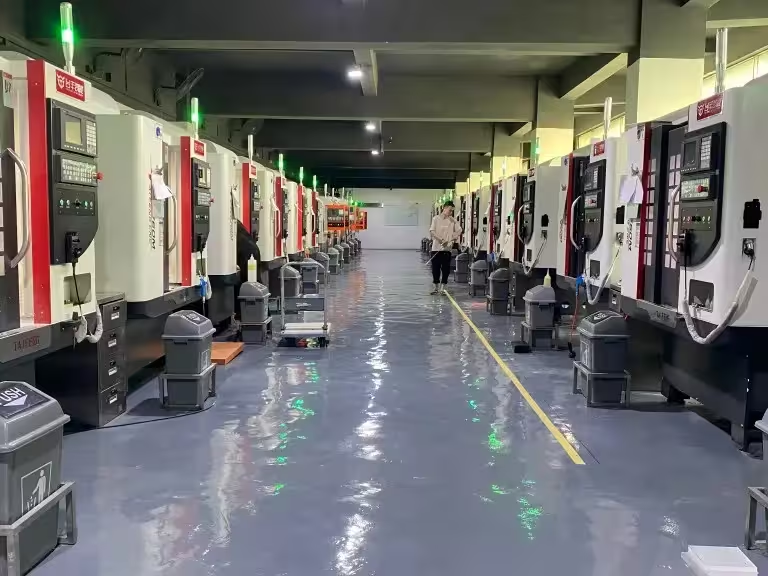
3 axis vertical CNC machining center at the GreatLight factory
27Three-axis machines on site
±0.005 mmAchievable tolerance
4,000 mmMaximum part length
12 hQuote and DFM turnaround
Where three-axis jobs go wrong

Four failures we get called in to fix

Most of these start as a drawing review problem, not a machine problem.

01

Do you keep re-quoting a part that should be one setup?

A part arrives with six faces of work. The shop quotes it as six operations, and the price never lands. On the right 3-axis setup with tombstone fixtures, the same part is two or three ops. The hours disappear, and so does the price gap.

02

Are hole positions drifting between batches?

Holes look fine on part one and miss on part fifty. Usually the cause is a vise that was re-clamped after a drill change, or a fixture with no hard stop. Position tolerance should come from the fixture, not from the operator.

03

Does the surface finish fail incoming inspection?

A Ra 1.6 μm callout turns into a hand-polish step, and the lead time grows. That usually means the tool path left chatter marks or the feed was pushed to save cycle time. Both are fixable in the program, not on the bench.

04

Is a 5-axis quote pricing work you do not need?

If every face of the part is reachable from three directions, 5-axis time buys nothing. You pay for simultaneous motion and a more expensive machine hour. Three-axis work with good fixtures is often the cheaper route to the same drawing.

The approach

Match the machine to the geometry, then control the setup

Three-axis work is won or lost in fixturing and in-process checks.

low volume manufacturing
Capability 1

One program, two or three operations

We start from the drawing and the stock, not from the machine list. Parts with flat faces, stepped pockets, drilled hole patterns and open profiles sit well on three axes. We plan the op sequence so datum faces stay accessible and re-clamping happens as little as possible.

Tombstone and pallet fixtures let us run the second and third sides without losing the datum. For a 200 mm aluminum bracket with 14 holes and two pockets, that is typically two setups instead of four, and the operator is not re-indicating the part each cycle.

  • 1
    Best fitPrismatic parts, plates, housings, brackets, manifolds with reachable faces
  • 2
    Not the best fitUndercuts, deep curved cavities, impeller blades needing simultaneous motion
  • 3
    Fixture planSoft jaws, tombstones, vacuum plates, hard stops on every datum

Get Instant Quote

684bbab2b23fcefcf18080703469ec1d
Capability 2

Tolerance held by the process, not by luck

The machines hold ±0.005 mm on a controlled process. To get there, we check the raw material certificate first, then monitor the first article and the middle of the run. A CMM report is available on request.

Thermal drift matters on long runs. We keep roughing and finishing in separate passes and let the part stabilize before the finish cut on tight bores. That is why a Ra 0.8–1.6 μm finish holds across the batch and does not need a polishing bench.

  • 1
    InspectionFirst article, in-process check, final inspection before shipment
  • 2
    ReportsDimensional report and material cert on request
  • 3
    Finish rangeRa 1.6–3.2 μm as machined, Ra 0.8–1.6 μm on request
Selection guide

Three-axis or five-axis? Use the geometry to decide

Same drawing, different machine hour. Pick by reachable faces and tolerance stack.

Part featureThree-axisFive-axis
Flat faces and open pocketsPreferredWorks, extra cost
Holes on three sidesWith tombstone fixtureOne setup
Undercuts and side wallsNeeds special toolingPreferred
Deep curved cavityNot practicalPreferred
Tight true position across facesFixture dependentFewer datum shifts
Simple plate, high volumePreferredOverkill
Prototype, one pieceFast to set upOnly if geometry needs it
What we run

Machining and finishing under one roof

Three-axis work rarely ships alone. These are the services that sit around it.

01

3 Axis CNC Machining

Milling of flat, prismatic and drilled parts on 27 three-axis machines, up to 4,000 mm in length.

02

CNC Milling & Turning

Milled features and turned diameters on the same part, with mill-turn centers for round-to-flat transitions.

03

4 Axis CNC Machining

Indexed rotary work for parts needing features on four sides without a second fixture.

04

5 Axis CNC Machining

For undercuts, curved cavities and one-setup multi-face work that three axes cannot reach.

05

Rapid Prototyping

Low-volume runs from a single piece, with DFM feedback before the program is cut.

06

Part Surface Finishing

Anodizing, plating, bead blasting, polishing and laser marking to finish the part.

Scope

Three-axis capacity and what is included

Numbers below come from our own machine list and inspection process.

ItemRangeNotes
Tolerance±0.005 mm±0.0002 in
Surface finishRa 0.8–1.6 μmRa 0.2–0.8 μm on request
Maximum length4,000 mmTravel 4,000 × 400 × 150 mm
Medium travel750 × 1,150 × 550 mmAlso 600 × 600 × 600 mm
Compact travel500 × 500 × 450 mmAlso 500 × 310 × 200 mm
Order sizeOne part to 10,000+No minimum order quantity
Lead timeShips in 3–5 daysProduction start within 24 hours
Inspection100% before shipmentReports on request
Why GreatLight

Data, not adjectives

Six numbers that decide whether your part ships on drawing.

27

Three-axis machines

Dedicated three-axis capacity, so a simple plate does not wait behind a complex five-axis job.

±0.005 mm

Held tolerance

Achievable on a controlled process, with first-article and in-process checks.

12 h

Quote and DFM

Quotation plus free DFM analysis within 12 hours of receiving a usable file.

150

Technicians

Across 3 wholly-owned plants covering 7,600 m² in Dongguan and Singapore.

4

Certifications

ISO 9001:2015, IATF 16949:2016, ISO 13485:2016 and ISO 27001:2022.

15Y

Machining since 2011

Fifteen years of production work, from prototypes to repeat runs.

127High-precision CNC machines
99.99%Qualification rate
<2%Historical late-delivery rate
7600 m²Manufacturing space
What ships

Parts and the checks behind them

cnc-machining-hdpe

Polymer fixture plates

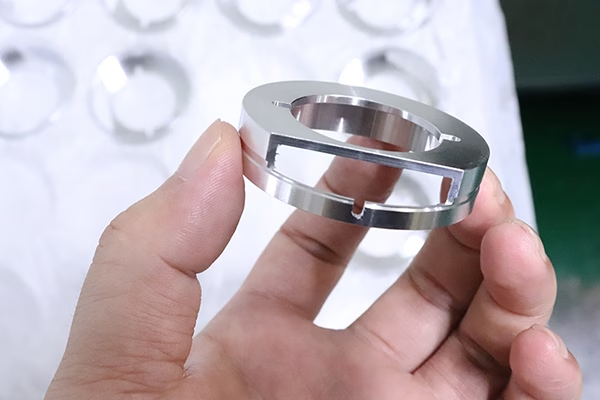
HDPE and POM plates with drilled patterns, flatness checked on the table.

  • ±0.005 mm
  • Ra 1.6 μm
a42b2d33e15263ef957ae4d86c94dbd5

Aluminum housings

6061-T6 enclosures with stepped pockets and cover screw holes.

  • 2 setups
  • 100% inspection
920d9fa383a15047596733347e2d5221

Stainless manifolds

316L blocks with cross-drilled ports and sealed faces.

  • 3–5 days
  • Material cert
5-Axis CNC Machining Online Quotation

Anodized brackets

Machined, deburred and clear anodized before final inspection.

  • Anodizing
  • +/−0.005 mm
FAQs

Questions engineers ask before sending a file

When is three-axis machining the right choice over five-axis?

Use three axes when every feature is reachable from a small number of directions: flat faces, open pockets, drilled holes, stepped profiles. If the part has no undercut and the tolerances stack from datums you can hold in a fixture, three axes will be cheaper and faster.

Move to five axes when the geometry needs side access, a deep curved cavity, or true position across faces that would otherwise need three or four re-clamps.

What tolerance can you actually hold on a production run?

±0.005 mm ( ±0.0002 in ) is our stated achievable tolerance on a controlled process. That assumes a stable material, a reasonable wall thickness and a datum you can repeat in the fixture.

Tighter work is possible on specific features, but it should be discussed before quoting. We will say so if a callout is not realistic on three axes.

What file format and information should I send?

A STEP file plus a 2D drawing with tolerances, material, finish and any critical features marked. If you only have a 3D model, note which dimensions are functional.

We return a quotation and a free DFM analysis within 12 hours. Production can start within 24 hours after the order is confirmed.

Which materials do you machine on three axes?

Aluminum 6061, 6061-T6, 2024, 5052, 5083, 6063, 6082, 7075 and ADC12; stainless 303, 304, 316, 316L, 420, 430, 431, 440C and 17-4PH; steels including 1018, 1045, 4130, 4140 and 4340; brass C36000 and other copper grades; titanium TA1, TA2 and TC4.

Plastics such as ABS, PC, POM, PA, PEEK, PP and HDPE are also common, especially for fixture plates and covers.

Is there a minimum order quantity?

No minimum order quantity. We run from one prototype to 10,000+ part runs on the same process.

For one-off parts we still do a first-article check. For repeat runs we keep the fixture and the program so the second order does not restart from zero.

How do you keep the part flat and the holes on position?

The fixture does the work. Hard stops and a repeatable datum mean the operator is not re-indicating the part every cycle. On thin plates we control clamping pressure so the part does not spring back after unclamping.

For hole patterns, we check the first article on a CMM and monitor the middle of the run. A dimensional report is available on request.

What surface finishes are available?

As machined we work in the Ra 1.6–3.2 μm range. On request we hold Ra 0.8–1.6 μm, and Ra 0.2–0.8 μm for sealing faces and sliding surfaces.

Finishing options include anodizing, electroless nickel and zinc plating, powder coating, black oxide, bead blasting, brushing, polishing and laser marking.

How is my design kept confidential?

All uploads are secure and confidential. We do not share drawings or models outside the production team, and an NDA is available on request.

ISO 27001:2022 covers our information security process, which applies to customer files as well as internal data.

Send the drawing, get a real answer in 12 hours

Upload a STEP file and we return a quotation with free DFM notes. No minimum order quantity, 100% inspection before shipment.

12-hour quote100% inspectionNo MOQ

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC