GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Magnesium Alloy Machining

CNC Magnesium Alloys: AZ31B and AZ91D Machining

Lightweight magnesium parts machined to ±0.005 mm with fire-safe chip handling. AZ31B and AZ91D run on our 3, 4, and 5-axis centers for housings, brackets, and drone frames.

AZ31B / AZ91D±0.005 mm5-axisFire-safe chip controlNo MOQ12-hour quote
cnc-magnesium-alloys
16Simultaneous 5-axis centers
±0.005 mmAchievable tolerance
150Technicians
99.99%Qualification rate
What Goes Wrong

Why Magnesium Parts Get Rejected or Delayed

Magnesium is not hard to machine. It is hard to machine without scrap, fire, or warped dimensions.

01

Chips ignite in the bin

Magnesium fines burn hot and fast. Shops that treat this metal like aluminium and let fines pile up in an open bin create a real fire risk. One spark in the tray stops the whole job and can take the machine offline for days.

02

Thin walls bow after clamping

Magnesium cuts easy, so operators push feeds and clamp hard. A 1.5 mm wall on a drone frame or instrument housing then springs back once the vise opens. The part measures true on the machine and out of spec on the CMM.

03

Corrosion starts at the fixture mark

Bare magnesium reacts with moisture and salts. Clamp marks, fingerprints, and coolant residue left on the surface become white oxide patches within weeks. The customer sees pitting on a part that was cosmetically clean at packing.

04

Wrong alloy, wrong properties

AZ31B and AZ91D do not behave the same. AZ91D casts well and machines fast but is less ductile. AZ31B bends and welds but is softer. Specifying one where the other belongs shows up as cracking or fatigue failure in service.

How We Machine It

Controlled Chips, Stable Cuts, Protected Surfaces

Three things decide whether a magnesium part leaves the shop good or scrapped.

low volume manufacturing
Chip Control

Fire-Safe Chip Handling From Spindle to Bin

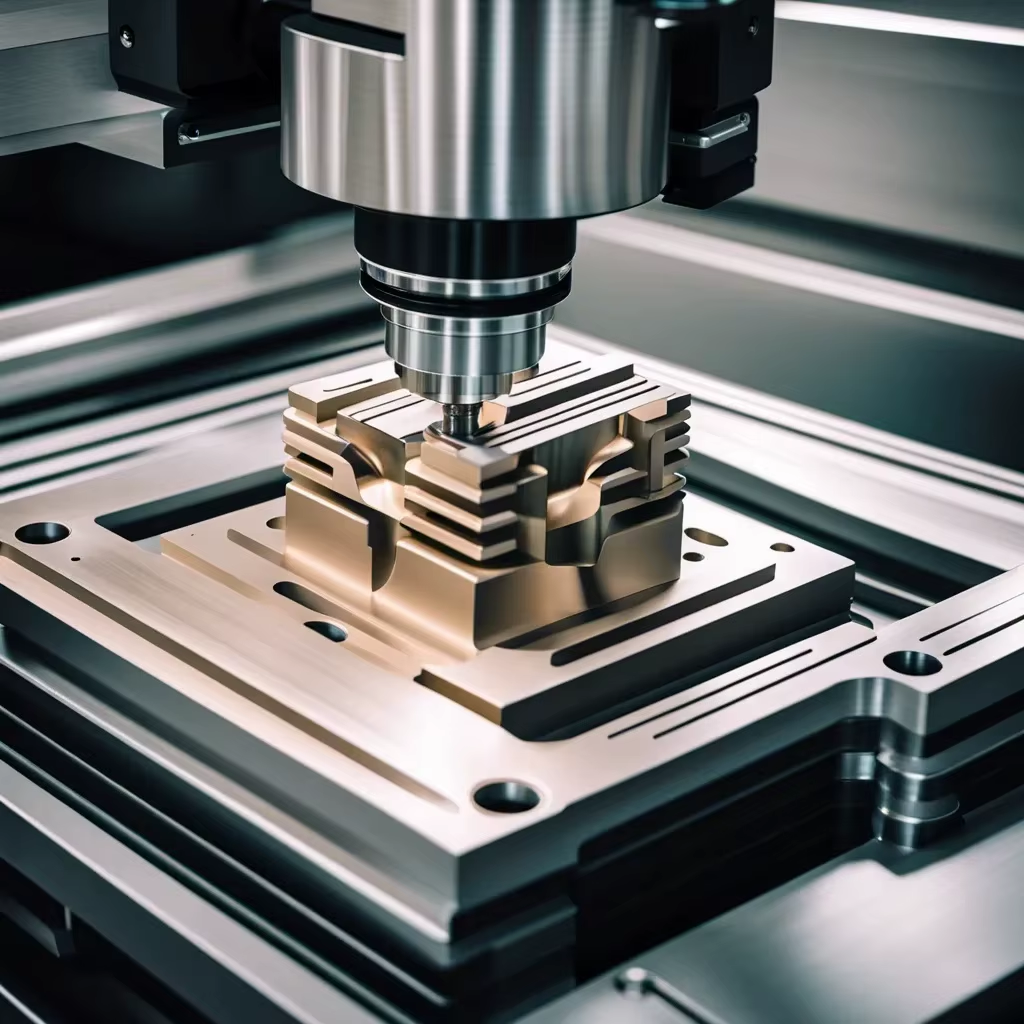
Magnesium chips are the main hazard on this job, not the cutting itself. We run sharp, high-rake tooling with large flute spaces so chips break short and clear the cut instead of packing in the flutes. No fine dust sitting under the part.

Dry or minimum-quantity lubrication is used where geometry allows. When coolant is needed, it is a dedicated magnesium-compatible fluid, never water-based fluid shared with steel jobs. Chips go straight into covered steel containers and are cleared at set intervals, not at the end of the shift.

  • 1
    Sharp high-rake toolsShort chips, less heat, lower ignition risk.
  • 2
    Covered steel binsFines never accumulate in an open tray.
  • 3
    Dedicated coolantNo cross-contamination with steel or aluminium lines.

Get Instant Quote

Custom 5 Axis CNC Machined Parts for Robot Arm Joints
Geometry and Finish

Thin Walls, Tight Tolerances, No Spring-Back

Magnesium has a low modulus, so it moves under clamp load. We rough and semi-finish, stress-relieve where the part allows, then take light finishing passes with reduced clamping pressure. Thin-wall housings and brackets hold ±0.005 mm without bowing.

Surfaces are protected before packing. Bead blasting, brushing, or a conversion coating removes clamp marks and leaves a surface that resists oxide growth in transit. Laser marking is available at a minimum character height of 1.5 mm for traceability.

  • 1
    Light finishing passesReduced clamp pressure keeps thin walls flat.
  • 2
    Surface protectionBlasting, brushing, or coating before packing.
  • 3
    Finished to Ra 0.8–1.6 μmRa 0.2–0.8 μm when the drawing calls for it.
Alloy Selection

AZ31B or AZ91D: Which One Fits the Part

Pick by load path, wall thickness, and how the part is made. Both machine well on our centers.

PropertyAZ31BAZ91D
Typical useSheet, extrusions, welded framesDie cast housings, covers
DuctilityHigher, bends and formsLower, stiffer in service
Machining speedGood, softer chipFast, clean chip break
Corrosion resistanceBetter in salt sprayNeeds coating sooner
Best for thin wallsYes, down to 1 mmOnly with light clamping
WeldingWeldableNot recommended
Surface finish as machinedRa 1.6–3.2 μmRa 0.8–1.6 μm
Cost per partHigher material costLower at volume
What We Do

Machining Services for Magnesium Parts

One shop for the whole part, from first article to production run.

01

5-Axis CNC Machining

Complex housings and brackets cut in fewer setups. 16 simultaneous 5-axis centers handle contoured surfaces and deep pockets that would need three fixtures on 3-axis.

02

4-Axis CNC Machining

Cylindrical and prismatic parts with features on multiple faces. A Ø400 mm rotary table keeps hole patterns concentric around a single axis.

03

3-Axis CNC Machining

Flat plates, covers, and simple brackets. The quickest route when the part has one working face and no undercuts.

04

CNC Milling & Turning

Mill-turn centers combine turning and milling on one platform. Shafts, bushings, and threaded bodies come off with concentricity held between features.

05

Rapid Prototyping

First articles in days for fit checks and test rigs. From one piece to 10,000+ part runs with the same process and inspection plan.

06

Surface Finishing

Bead blasting, brushing, polishing, anodizing, plating, and laser marking. Magnesium gets a protective step before packing so it ships clean.

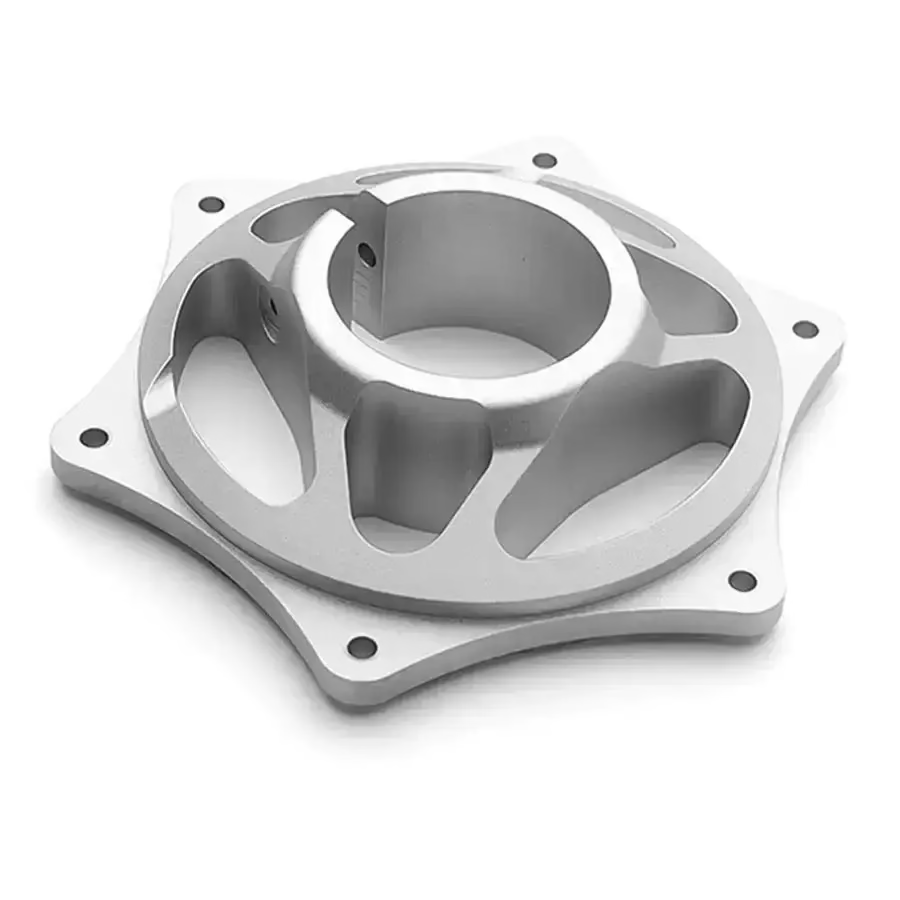
Scope

Magnesium Machining Scope and Limits

Numbers we hold on real jobs, not catalog promises.

ItemSpecification
MaterialsAZ31B, AZ91D
Tolerance±0.005 mm (±0.0002 in)
As-machined finishRa 1.6–3.2 μm
Fine finishRa 0.2–0.8 μm
Maximum part size4,000 mm
Large travel4,000 × 400 × 150 mm
Rotary tableØ400 mm
Minimum wall adviceFrom 1 mm, light clamping
Inspection100% before shipment
Order sizeOne prototype to 10,000+ parts
Why GreatLight

Why Engineers Send Magnesium Work Here

The differences that show up on the inspection report.

15Y

15 Years in Metal Cutting

Founded in 2011. Three wholly-owned plants and 7,600 m² of manufacturing space in Dongguan, plus a Singapore factory at No.3 Joo Koon Circle.

127

127 High-Precision CNC Machines

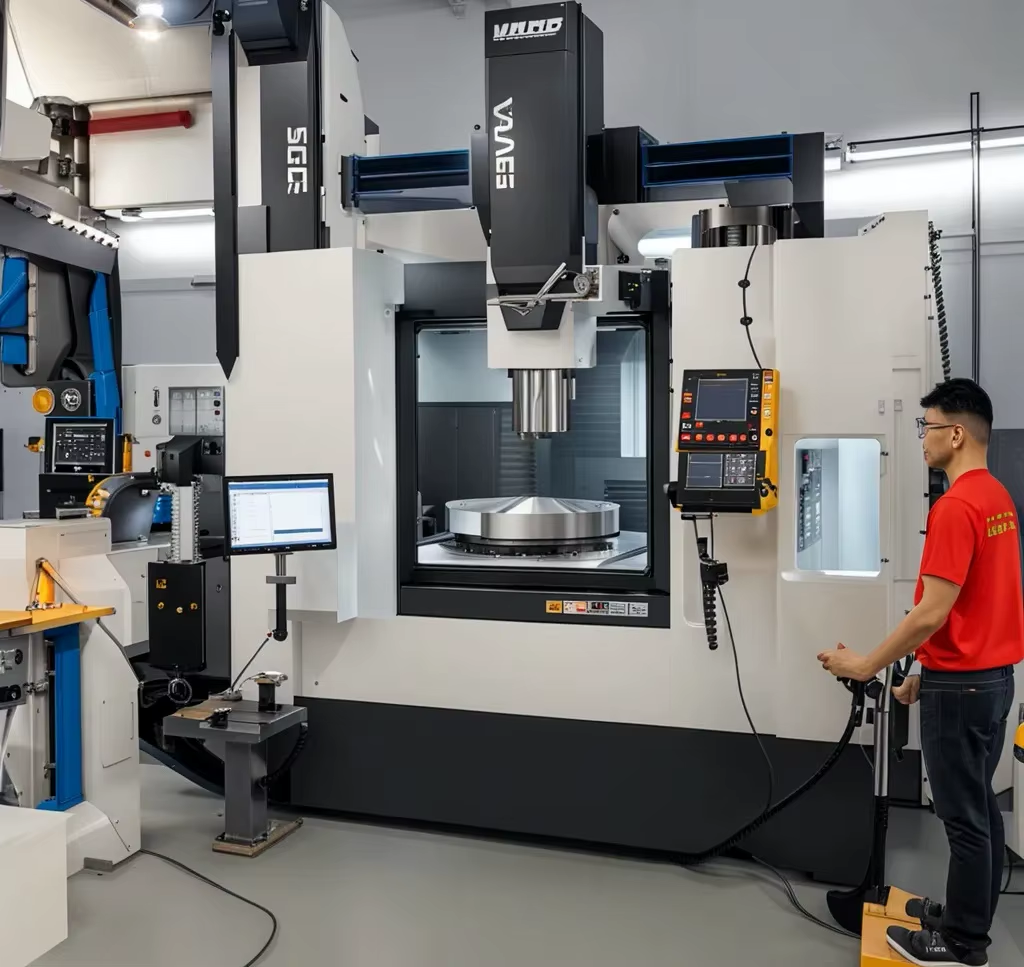
16 simultaneous 5-axis centers, 12 four-axis mills, 27 three-axis machines, and 16 mill-turn centers. Magnesium jobs get the right machine, not the free one.

±0.005 mm

Tolerance Held on Thin Walls

Light finishing passes and controlled clamping keep low-modulus parts flat. The same number applies to first article and to part 5,000.

99.99%

Qualification Rate

Raw material check, in-process monitoring, and final inspection on every order. Reports are available on request.

12 h

Quote and DFM in 12 Hours

Send a model and get a quotation with free DFM analysis inside 12 hours. Production can start within 24 hours after approval.

3–5 d

Parts Ship in 3–5 Days

Historical late-delivery probability below 2%. We quote the date we can hold, not the date that wins the order.

7,600 m²Manufacturing space
150Technicians
16Simultaneous 5-axis centers
4,000 mmMaximum processing size
Industry Fit

Where Magnesium Parts Are Used

Custom 5 Axis CNC Machined Parts for Robot Arm Joints (3)

Robotics & Automation

Arm links and joint housings where mass drives motor sizing and cycle time.

  • ±0.005 mm
  • Lightweight arm links
  • 100% inspection
GreatLight Your Premier Partner for Precision Auto Parts Processing Custom CNC Machined Solutions

Automotive & EV

Brackets and housings that cut sprung mass without giving up stiffness.

  • IATF 16949:2016
  • Weight reduction
  • Run sizes to 10,000+
Custom 5 Axis CNC Machined Parts for Robot Arm Joints (1)

Aerospace

Instrument housings and support structures where every gram counts.

  • AZ31B sheet parts
  • Ra 0.8–1.6 μm
  • Inspection reports
FAQs

Questions Engineers Ask About Magnesium Machining

Is machining magnesium actually dangerous?

The metal in solid form is not the problem. Fine chips and dust are. They have a low ignition temperature and burn with a hot flame that water can make worse.

The controls are simple and well known: sharp tooling to make short chips, no fines sitting in open trays, covered steel containers, and a dedicated magnesium-compatible coolant when coolant is used at all. We run the job that way on every order.

Which alloy should I specify, AZ31B or AZ91D?

Start from the load path and the process. AZ31B is more ductile, welds, and holds up better in salt spray, so it suits sheet parts, welded frames, and anything that bends in service.

AZ91D machines faster and takes a better as-machined finish, which suits die-cast housings and covers. If you need thin walls below about 2 mm, AZ31B is usually the safer choice.

What tolerance can you hold on a thin magnesium wall?

±0.005 mm is achievable on stable geometry, including walls around 1 mm, provided we control clamping pressure and take light finishing passes.

Very long unsupported walls or parts with large open pockets may need an intermediate stress-relief step or a fixture that supports the wall from behind. We flag that in the DFM review before cutting.

How do you stop magnesium parts corroding before they reach us?

Bare magnesium reacts with moisture, salts, and skin oils. Clamp marks and fingerprints become oxide patches if the part is packed as-is.

We remove handling marks by bead blasting or brushing, then apply a conversion coating or the finish called out on the drawing. Parts are bagged with desiccant before shipping.

Can you machine magnesium and aluminium on the same machine?

Not without a full clean-down. Magnesium fines left in a machine that later runs aluminium, or mixed with steel swarf, create a fire and contamination hazard.

We schedule magnesium work with dedicated tooling and a clean-down routine between material families, and keep the chips segregated from the start.

What is the minimum order quantity?

There is no minimum order quantity. We run from a single prototype to 10,000+ part runs with the same process and inspection plan.

Prototype pricing and production pricing are quoted separately so you can see where the volume break sits before committing.

What do you need to quote a magnesium part?

A 3D model in STEP or IGES, a 2D drawing with tolerances and critical features, the alloy, the finish, and the quantity. Material condition and any coating spec help too.

Quotation and free DFM analysis come back within 12 hours. Uploads are secure and confidential, and an NDA is available on request.

Do you provide inspection reports for magnesium parts?

Yes. Every order gets a raw material check, in-process monitoring, and a final inspection, with 100% inspection before shipment.

Dimensional reports and material certificates are available on request. If a feature is critical, tell us at quoting so it goes on the inspection plan.

Send Your Magnesium Part for a Quote

Upload a model and get a quotation with free DFM analysis within 12 hours. No minimum order quantity, 100% inspection before shipment.

12-hour quoteNo MOQ100% inspectionNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC