
Mitsubishi CNC Machining Center: How It Cuts Metal
This page explains what a Mitsubishi CNC machining center actually does inside our shop: spindle and thermal behavior, axis configuration, workholding, and the tolerances it can hold. It is written for design engineers and buyers who need to judge whether a part belongs on this machine or somewhere else.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
- 8
What a Mitsubishi CNC machining center does on the floor
A Mitsubishi CNC machining center is a vertical or horizontal machining platform: the frame, spindle, ballscrews and control come from Mitsubishi, and the tooling, fixtures and programs come from us. That split matters. The builder sets the machine's stiffness and its control loop; the shop decides how hard it can push before chatter, drift or tool wear eats the tolerance.
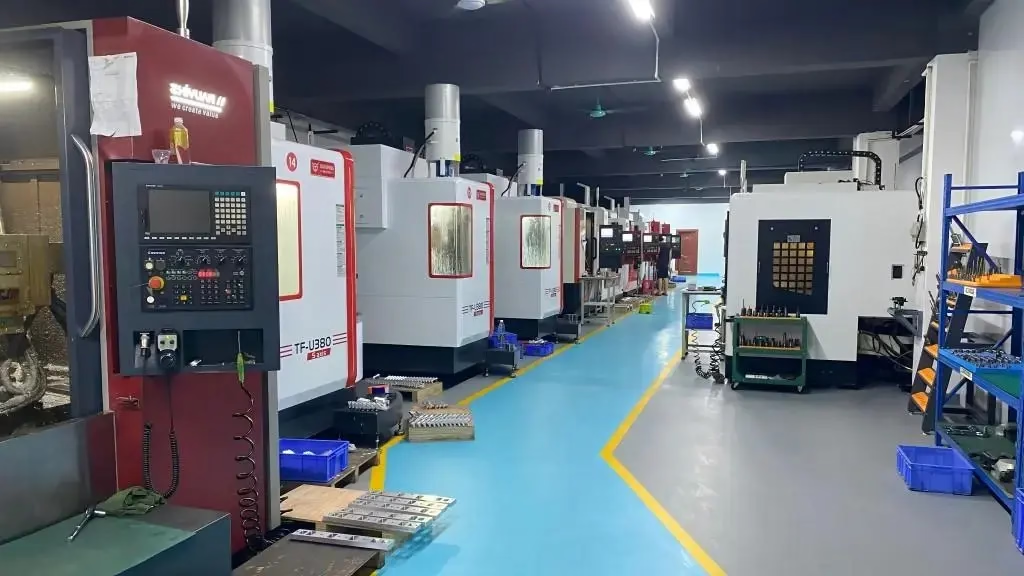
GreatLight runs 127 high-precision CNC machines across three wholly-owned plants in Dongguan and Singapore. Mitsubishi centers sit in that fleet alongside 16 simultaneous 5-axis machining centers, 12 four-axis mills, 27 three-axis machines and 16 mill-turn centers. We keep the Mitsubishi platforms on jobs where the geometry needs a stable, well-damped cut rather than the fastest possible cycle.
When a part arrives, the first question is not which machine is free. It is which axis count and which workholding will hold the drawing tolerance through the whole run. A Mitsubishi CNC machining center can hold ±0.005 mm (±0.0002 in) on a well-fixtured part, but only if the setup stops the part from moving when the cutter loads it.
The control matters too. Mitsubishi drives and controls let us tune acceleration, look-ahead and feed override per operation. On a thin-wall aluminum housing that tuning is the difference between a clean floor finish and a part that rings like a bell and scraps.
- 1Frame and spindleSet by the builder; determines stiffness and damping.
- 2Fixtures and programsSet by the shop; determines whether tolerance holds.
- 3Control tuningAcceleration and look-ahead tuned per operation.
Spindle speed, load and what it does to the cut
Spindle speed and feed are a pair. Push the surface speed up on aluminum and the chip leaves hot but clean; push the same number on 316 stainless and the edge breaks down in minutes. On a Mitsubishi CNC machining center we set the spindle range by material first, then adjust feed to keep chip load per tooth in a sane band.
For aluminum 6061 and 7075 we typically run high spindle speeds with light radial depth and heavy axial depth. The cutter engages a short arc, heat leaves with the chip, and the tool lasts. For titanium TC4 (Ti-6Al-4V) and Inconel the opposite applies: lower surface speed, heavier chip load, and enough coolant or air blast to keep the edge from rubbing.
Spindle load is the number to watch, not spindle speed alone. A meter that climbs toward the machine's rated load during a finishing pass means the tool is rubbing rather than cutting. Back off the feed or change the stepover before the edge dulls.
Runout is the quiet killer. A toolholder with 0.01 mm runout cuts one flute harder than the others, and that flute wears first. We check holders on the presetter and swap anything that drifts beyond the shop limit.
- 1AluminumHigh surface speed, light radial, heavy axial depth.
- 2Titanium and InconelLower surface speed, heavier chip load, strong cooling.
- 3Watch spindle loadRising load on a finish pass means rubbing, not cutting.
Thermal drift and why the first part is not the tenth
A machine grows as it warms. Spindle bearings, ballscrews and the frame all move a few microns as temperature rises through the first hours of a shift. On a tight job that drift can consume most of a ±0.005 mm band if nobody accounts for it.
The fix is boring and effective. We run a warm-up cycle before the first cut, then probe a master artifact and let the control compensate. On long runs we re-probe at intervals, not just at the start. That keeps part ten sitting where part one sat.
Coolant temperature matters as much as spindle temperature. A chiller holding the coolant within a degree or two keeps the part from growing between roughing and finishing. On thin aluminum plates, part growth from cutting heat alone can exceed the tolerance band.
If a job cannot tolerate that drift at all, the answer is often to rough, let the part and machine settle, then finish in a second setup. It costs a fixture re-clamp. It saves the run.
- 1Warm up firstRun the spindle cycle before the first cut.
- 2Probe and compensateMaster artifact checked at start and during long runs.
- 3Chill the coolantHold temperature within a degree or two.
Materials that behave well and materials that fight back
Aluminum is the easy one. Grades 6061, 6061-T6, 2024, 5052, 5083, 6063, 6082 and 7075 all cut cleanly on a Mitsubishi CNC machining center at high spindle speed. They also move when you remove stock, so roughing and finishing in separate passes keeps flatness in check.
Stainless is where setups start to matter. Grades 303, 304, 316, 316L, 420, 430, 431 and 440C work-harden if the tool rubs instead of cuts. Keep the chip load up and never let the cutter dwell. 17-4PH (SUS630) cuts well in the annealed state and gets harder after aging, so schedule the heat treat after machining.
Titanium and Inconel demand patience. TA1, TA2 and TC4 (Ti-6Al-4V) conduct heat poorly, so the edge carries the temperature. Lower surface speed, generous coolant, and sharp tools. Inconel is worse. It is doable on the Mitsubishi platforms but it is not a fast job, and the quote should reflect that.
Plastics and composites are their own problem. ABS, PC, PMMA, POM, PA, PEEK, PP, HDPE and carbon fibre cut at high spindle speed with sharp, polished flutes and strong chip evacuation. Carbon fibre dust is abrasive; it wears cutters and it needs extraction, not just a vacuum hose nearby.
- 1AluminumFast and clean; watch stress relief on thin walls.
- 2StainlessWork-hardens if the tool rubs; keep chip load up.
- 3Titanium and InconelHeat goes into the edge; lower speed, sharp tools.
- 4Plastics and carbon fibreSharp polished flutes; extract abrasive dust.
Workholding decides whether the tolerance survives
Most out-of-tolerance parts do not fail because the machine was inaccurate. They fail because the part moved. A vise with too little grip, a thin plate supported only at the edges, or a fixture that lets the part deflect under cutter load will all produce a part that measures wrong after unclamping.
For a Mitsubishi CNC machining center we match the fixture to the part stiffness. Thick blocks go in vises or on tombstones. Thin plates get vacuum chucks or a bed of support so the cutter cannot push the middle down. Round parts go on a Ø400 mm rotary table when faces need indexing.
The 4,000 × 400 × 150 mm travel on our large platforms lets long weldments go on in one setup. That is usually better than re-clamping a long part across two operations, because every re-clamp adds a new error source. One setup, one datum, one tolerance stack.
We also plan the order of operations around the fixture. Faces that must be parallel get machined in the same setup whenever the geometry allows it. When it does not, we leave stock and finish them after a re-clamp that has been probed back in.
- 1Match fixture to stiffnessVises for blocks, vacuum or full support for thin plates.
- 2Fewer setupsEach re-clamp adds an error source to the stack.
- 3Probe after re-clampRe-establish the datum before finishing.
Holding ±0.005 mm and the finishes that follow
±0.005 mm is a shop capability, not a default. It applies to features that are accessible, well-supported and measured on a machine that has been warmed up and probed. A deep bore at the end of a long tool is not the same job as a face milled with a short, rigid cutter.
Surface finish follows the same logic. As-machined aluminum lands around Ra 1.6–3.2 μm. A careful finishing pass on a stable setup reaches Ra 0.8–1.6 μm. Fine finishes in the Ra 0.2–0.8 μm range need slower feeds, sharper tools and often a secondary operation rather than a single pass on the machining center.
Inspection backs this up. We check raw material on arrival, monitor in process, and inspect 100% of parts before shipment. Reports are available on request. If a feature is critical, tell us which one at quote time so the inspection plan targets it rather than spreading effort evenly.
Tolerance and finish also interact with the finishing services. Anodizing, electroless nickel, zinc, silver and gold plating, powder coating and black oxide all add or remove a thin layer. Laser marking needs a minimum character height of 1.5 mm to stay legible. Plan those steps before the final dimensions are locked.
- 1Capability, not default±0.005 mm applies to accessible, supported features.
- 2Finish tiersRa 1.6–3.2 μm as-machined up to Ra 0.2–0.8 μm fine.
- 3Plan finishing earlyCoatings change dimensions; marking needs 1.5 mm.
When a Mitsubishi CNC machining center is the wrong call
A machining center removes metal from solid stock. If the part is a thin-walled enclosure with a complex shape and you need fifty of them, die casting or sheet metal fabrication will beat it on cost per part. Machining wins on prototypes, low volume, tight tolerance and geometry that a mold cannot pull.
If the part is a simple round shaft with no milled features, a lathe is faster than a machining center. If it has milled flats and turned diameters, a mill-turn center does both in one chucking and avoids the concentricity error of moving the part between machines.
Five-axis simultaneous cutting is not automatically better than 3-axis. It adds setup and programming time. Use it when the geometry needs it or when one setup removes a tolerance stack that would otherwise need three fixtures. For a flat bracket, five-axis just costs more.
Finally, if the tolerance you need is beyond ±0.005 mm on a feature that is hard to reach or hard to hold, say so at quote time. We would rather tell you the part needs a different process than ship a run that measures wrong.
- 1High volume, thin wallsDie casting or sheet metal usually wins on cost.
- 2Simple round partsA lathe is faster than a machining center.
- 3Five-axis by defaultAdds setup time unless geometry or setups demand it.
Which axis count fits which part
Judged by geometry, not by machine availability.
| Part feature | Axis count | Why |
|---|---|---|
| Flat plate, holes on one face | 3-axis | One setup, no re-clamp, fastest cycle. |
| Holes on four sides of a block | 4-axis | Rotary table indexes faces without re-fixturing. |
| Contoured impeller or turbine blade | 5-axis simultaneous | Tool stays normal to surface, one setup. |
| Deep pocket with undercut | 5-axis | Short tool reach, less deflection. |
| Turned shaft with milled flats | Mill-turn | Turning and milling in one chucking. |
| Large weldment, 4,000 mm long | 3-axis gantry | Travel fits the part; rigidity suits long cuts. |
| Prototype, one to ten parts | 3-axis or 4-axis | Setup time dominates; skip the extra axes. |
The verdict
Choose a Mitsubishi CNC machining center for prototypes, low-to-mid volume and parts that need tight tolerance in few setups. Choose casting, sheet metal or turning when the geometry or the volume points there instead.
Questions engineers ask
Can you hold ±0.005 mm on every feature?
No, and no shop can honestly promise that. ±0.005 mm is the capability on features that are accessible, rigidly supported and measured after the machine has warmed up and been probed.
Deep bores, long tool reaches and thin unsupported walls sit outside that band. Tell us which feature is critical at quote time and we will build the setup and the inspection plan around it.
Is five-axis always more accurate than three-axis?
Not by itself. Five-axis simultaneous cutting helps when the geometry needs it or when one setup removes tolerance stack that three fixtures would add.
For a flat bracket with holes on one face, three-axis is faster, cheaper and just as accurate. We pick the axis count from the part, not from what is idle.
How do you stop thermal drift from ruining a long run?
We run a warm-up cycle before the first cut, probe a master artifact, and let the control compensate. On long runs we re-probe at intervals rather than only at the start.
Coolant is chilled within a degree or two, which keeps the part from growing between roughing and finishing. If the job still will not hold, we split roughing and finishing into separate setups.
What is the maximum part size?
Our large platforms take up to 4,000 mm maximum processing size, with travel of 4,000 × 400 × 150 mm on the biggest configuration.
Other machines cover 750 × 1,150 × 550 mm, 600 × 600 × 600 mm, 500 × 500 × 450 mm and 500 × 310 × 200 mm. Send the drawing and we will match it to the right platform.
Do you machine titanium and Inconel?
Yes. TA1, TA2 and TC4 (Ti-6Al-4V) are routine, and Inconel is doable on the Mitsubishi platforms.
Both carry heat into the cutting edge, so surface speed drops and cycle time rises. The quote reflects that. It is not a fast job and we will not pretend otherwise.
Can you handle finishing after machining?
Yes. Anodizing (clear, colour, hardcoat, conductive), electroless nickel, zinc, silver and gold plating, powder coating, black oxide, bead blasting, tumbling, brushing and polishing are all available.
Laser marking and engraving need a minimum character height of 1.5 mm. Coatings add a thin layer, so lock final dimensions with the finishing step in mind.
Send the drawing, get a real answer
Quotation and free DFM analysis within 12 hours. Uploads are secure and confidential, and an NDA is available on request.
12-hour quote100% inspectionNo minimum order quantity
More from GreatLight
We publish setup notes, tooling trials and inspection data from the factory floor.











