
CNC Processing Center for Personal Data: How Job Data Stays Protected
A machining center is a mill with an automatic tool changer and an enclosed work envelope. This page explains how a CNC processing center for personal data handles files, programs, and job records, plus where the machine itself stops being the right choice. Read it if you are deciding between a machining center, a lathe, or a mill-turn platform.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
What a CNC processing center actually is
A CNC processing center is a milling machine that changes its own tools. That single feature separates it from a manual mill and from a basic CNC mill. The spindle stops, the arm swaps the cutter, the spindle restarts, and the cut continues from the same coordinate system. A job that needs a 12 mm end mill, a 6 mm ball nose, a drill, and a tap runs without an operator standing at the door.
The second feature is the enclosure. Chips and coolant stay inside. The machine can run at higher feed rates because the operator is not standing in the line of fire. Thermal drift is smaller too, since the casting and the ballscrews sit in a controlled pocket of air rather than in the shop draft.
The third feature is the control. A single controller holds the tool table, the work offsets, and the program. Everything the machine needs to make a part lives in one place. That is why the same machine can run a one-off prototype on Monday and a 10,000 part run next month with the same setup sheet.
None of that is about the data on your drawing. It is about the mechanics. The data question comes later, once you decide the geometry belongs on a machining center at all.
3-axis, 4-axis, and 5-axis: what the extra axes buy you
A 3-axis machining center moves the table in X and Y and the spindle in Z. The cutter always points down. Any face you cannot reach from above needs a second setup, a re-fixture, and a new datum. Each re-fixture adds error. On a part with four machined faces, that is four chances to lose 0.02 mm.
A 4-axis machine adds a rotary table, usually about a horizontal or vertical axis. Now the part can index to a new face without being unclamped. Holes on four sides of a block get drilled in one program. The datum never changes. For housings, manifolds, and brackets, this alone removes most of the setup error.
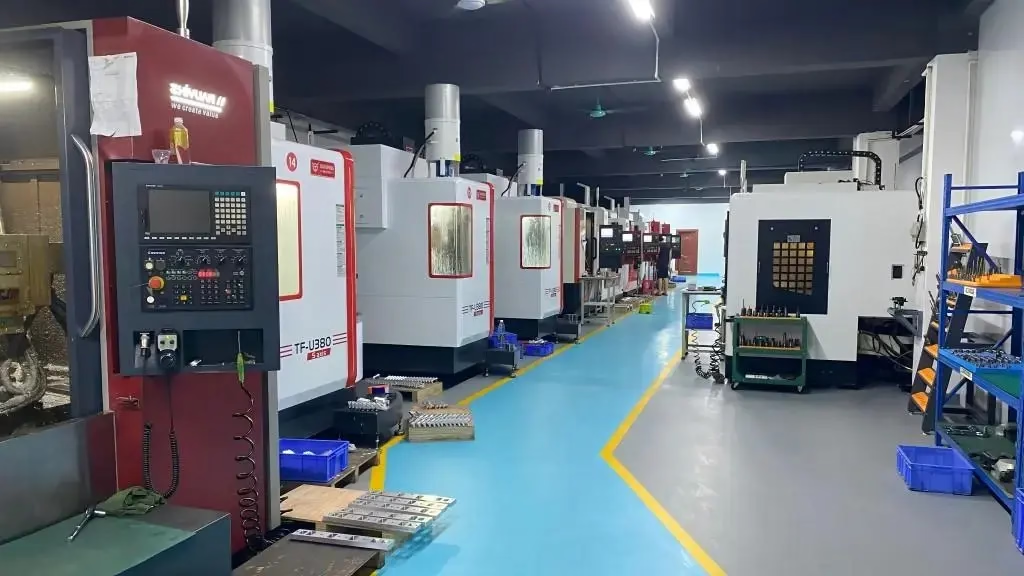
A 5-axis machine moves the tool and the part at the same time. The cutter can tilt, so a ball nose reaches into a deep pocket without the shank rubbing the wall. Undercuts, compound angles, and sculpted surfaces come off in one pass. GreatLight runs 16 simultaneous 5-axis machining centers alongside 27 three-axis and 12 four-axis mills, so the axis count is chosen by geometry, not by what is free.
The trade-off is rigidity. A trunnion table hangs the part out on a rotating axis, and that axis flexes under load. Deep, heavy cuts belong on a 3-axis machine. Thin, complex, hard-to-reach features belong on 5-axis. Mixing them up is how you get chatter on a part that should have been simple.
Tool changing, offsets, and why the tool table matters
The tool changer holds a magazine of cutters, commonly 20 to 40 stations. Each station has a length and diameter stored in the control. When a program calls T07, the machine knows how long that tool is and compensates in Z. Change the tool without updating the offset and the next cut is off by the difference.
This is where most first-article scrap comes from. A fresh end mill is shorter than a reground one. The operator measures the tool, enters the number, and the control does the math. On a ±0.005 mm job, a 0.02 mm offset error is four times the tolerance band. It will show up on the CMM.
Tool life is managed by cut time or by part count. A carbide end mill in 6061 aluminium might run for hours. The same cutter in 17-4PH stainless wears much faster. The control flags the tool for change, and the next part runs with a fresh edge. This keeps the finish consistent across a run instead of drifting from Ra 0.8 μm to Ra 1.6 μm halfway through.
For a part with a tight bore, we often leave the finishing tool in the spindle and run the whole batch with it. Swapping mid-run introduces a step you cannot inspect away.
How a CNC processing center for personal data handles job files
Every machining job carries data: the CAD model, the CAM program, the setup sheet, the inspection report, and the customer name attached to all of it. On a shared shop network, that data can leak through a shared folder, an email thread, or a machine terminal left logged in. A CNC processing center for personal data is the same machine with tighter controls around those files.
The first control is access. Programs live on a server with named accounts, not on a USB stick in a drawer. An operator sees the program for the job at their machine and nothing else. When the job closes, the access closes with it. That is the difference between a machine and a machine inside a managed system.
The second control is the record. Every file open, every program edit, and every download is logged with a user and a timestamp. If a drawing leaves the building, there is a trail. This matters for medical device work and for any customer under an NDA who needs to show their own auditor how the part was handled.
The third control is the network itself. Machines sit on a segmented network, separate from office email and browsing. A shop floor terminal that cannot reach the open internet is a much smaller target. GreatLight holds ISO 27001:2022 for information security, alongside ISO 9001:2015, IATF 16949:2016, and ISO 13485:2016 for the quality side.
None of this changes the cut. It changes who can see the drawing that produced it.
Which parts belong on a machining center, and which do not
A machining center earns its cost when a part has multiple features on multiple faces, needs tight tolerance, or has to be made in a batch that stays identical. A gearbox housing with bores on four sides, a manifold with angled ports, a fixture plate with 60 tapped holes. These are machining center parts.
Prismatic parts with pockets, slots, and faces are the classic fit. So are parts that need a good surface finish on a visible face, because the machine can run a finishing pass at Ra 0.8–1.6 μm without a second operation.
A shaft, a bushing, or a threaded stud is not a machining center part. Those are turned parts, and a lathe makes them faster and rounder. Sending a simple turned part to a mill wastes cycle time and usually hurts concentricity.
Very large parts need a machine that can hold them. GreatLight runs a 4,000 mm maximum processing size with travels up to 4,000 × 400 × 150 mm for long parts, and 750 × 1,150 × 550 mm or 600 × 600 × 600 mm for the mid-size envelope. A part that does not fit the envelope is not a machining center job, no matter how good the geometry is.
Finally, consider quantity. One prototype and 10,000 parts both run on the same machine, but the economics change. At low volume the setup dominates. At high volume the cycle time dominates, and it is worth spending a day on a better fixture to shave 40 seconds per part.
If the part is thin-walled, flexible, or made of a gummy plastic like PP or HDPE, expect to fight chatter and chip welding. Those parts can be machined, but they need light passes, sharp tooling, and often a fixture that supports the wall from behind.
Machining center vs lathe vs mill-turn
Pick the platform by part geometry, not by habit.
| Part type | Best platform | Why | Watch out for |
|---|---|---|---|
| Prismatic housing with pockets | 3-axis machining center | One datum, flat faces, easy fixturing | Multiple setups on side features |
| Part with holes on 4 faces | 4-axis machining center | Indexes without unclamping | Rotary table rigidity |
| Sculpted or undercut surface | 5-axis machining center | Tilting cutter reaches deep walls | Longer cycle, higher rate |
| Shaft or bushing | CNC lathe | Roundness comes free from rotation | Off-axis holes need a mill |
| Round part with cross holes | Mill-turn center | Turning and milling in one setup | Program complexity |
| Thin-wall plastic cover | 3-axis, light passes | Simple geometry, low load | Chatter and chip welding |
| 4,000 mm long extrusion | Long-travel 3-axis | Fits the 4,000 × 400 × 150 mm bed | Sag needs support |
| One-off prototype | 3-axis or 4-axis | Setup cost dominates | Do not over-spec the axis count |
The short version
If your part is prismatic, needs tight tolerance, and has features on more than one face, use a machining center. If it is round, use a lathe. If it is round with cross holes, use a mill-turn. The axis count should follow the geometry, and the data controls should follow the customer's NDA.
Common questions
What tolerance can a machining center hold in production?
On aluminium and stainless parts, ±0.005 mm (±0.0002 in) is achievable on critical features when the setup is rigid and the machine is thermally settled. That is a production number, not a best-case lab number.
Tighter than that usually means grinding or lapping after machining. We will tell you if the tolerance on your drawing needs a second process.
Can a machining center cut titanium and Inconel?
Yes, with the right tooling and speeds. TC4 (Ti-6Al-4V) and Inconel both cut on a rigid 3-axis or 5-axis machine, but they generate heat at the cutting edge and work-harden if the feed is too light.
Expect slower cycle times and more tool changes than aluminium. We machine TA1, TA2, TC4, Inconel, and magnesium AZ31B / AZ91D regularly.
How do you keep my drawings confidential?
Files sit on a named-account server, not on shop floor USB drives. Access is limited to the people running the job, and the job closes when the parts ship.
We sign NDAs on request and hold ISO 27001:2022 for information security. Uploads through our quote page are encrypted in transit.
Do I need 5-axis, or is 3-axis enough?
Use 3-axis if all your features are reachable from one direction and the part is stiff. Use 5-axis if you have compound angles, deep pockets with thin walls, or undercuts that a straight cutter cannot reach.
The test is simple: can a cutter pointing straight down reach every feature? If yes, 3-axis is cheaper and often faster.
What is the smallest order you take?
There is no minimum order quantity. We run from one prototype to 10,000+ part runs on the same equipment.
For a single prototype, a 3-axis or 4-axis setup usually makes more sense than a 5-axis job, because the setup cost is lower.
How fast can parts ship?
Quotation and DFM feedback come back within 12 hours. Production can start within 24 hours after that, and parts typically ship in 3–5 days.
That depends on material availability and finish. Anodizing and plating add time to the schedule.
Send us the drawing, get a real answer
Upload your CAD file and we will tell you which machine the part belongs on, what tolerance is realistic, and what it will cost.
12-hour quote100% inspectionNo minimum order quantity
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.











