GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Display Dummies & Presentation Models

iPhone 17 Prototype CNC Machining for Display Dummies

We machine non-functional phone bodies that match your CAD envelope, so accessory brands and retail teams can check fit, finish and weight before tooling is cut. Aluminum or plastic, 5-axis, built to ±0.005 mm.

±0.005 mm16 five-axis centersNo MOQ12-hour DFM
Eb8e491ce670cd367ed5171558e71240
±0.005 mmMachining tolerance
16Simultaneous 5-axis centers
3–5 daysParts ship after start
99.99%Qualification rate
Where display dummies go wrong

Four Failures We See Every Month

Most dummy phone problems show up on the buyer's desk, not on the drawing.

01

Cable fit fails at the port cutout

A 0.15 mm error at the charging port and the Lightning or USB-C plug binds. Buyers return the whole batch, and the accessory launch slips a week. Port and speaker slots need to be cut with micro-tooling and checked against a gauge, not eyeballed.

02

Camera bezel height drifts

Raised bezels that sit 0.2 mm proud break the look in product photos. Too low and the lens ring rubs the table. We hold bezel height and step depth on the same setup so the rear face reads flat to the eye and to calipers.

03

Plastic bodies come back warped

Thin ABS or PC walls move after machining when the blank was molded with internal stress. A 0.3 mm bow kills the seam line. We rough, stress-relieve, then finish, and keep wall thickness above 1.2 mm where the design allows.

04

Surface finish does not match the real phone

Bead blast too coarse and the body looks like a tool, not a phone. Too fine and fingerprints show under showroom lights. Anodized 6061 at Ra 0.8–1.6 μm reads closest to a production handset for display and trade-show use.

How we build the dummy

Machined Bodies That Match Your CAD Envelope

From a STEP file to a finished, non-functional phone body in days.

cnc-machining-hdpe
Body machining

5-axis cutting of the shell, bezel and slots

A dummy handset lives or dies on the outer shell. We clamp the blank once and cut the profile, the rear camera plateau, the side button slots and the port opening on a simultaneous 5-axis center. One setup means the datum never moves between features, so the bezel stays concentric with the body and the buttons sit at the right depth.

For aluminum bodies we start from 6061 or 7075 and hold ±0.005 mm on critical faces. Plastic shells run in ABS, PC, PMMA or POM. Walls below 1.0 mm are possible but they flex during clamping, so we add support ribs or machine them in a soft jaw.

  • 1
    One-setup accuracyProfile, bezel and cutouts share the same datum.
  • 2
    Micro-tooling0.5–2 mm end mills for port slots and speaker holes.
  • 3
    CMM verifiedKey dimensions checked against your CAD model before shipping.

Get Instant Quote

deb497643057917a23d79fa6ea36ce7a
Finish and assembly

Finishing that reads like a real handset

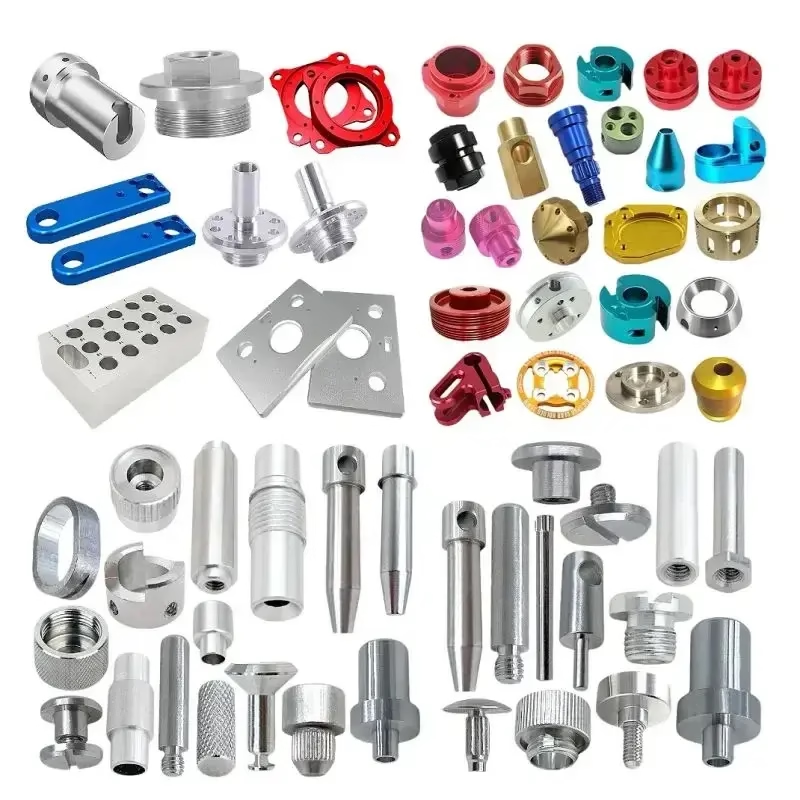
A display dummy is judged at arm's length under store lighting. Anodizing in clear, black or a custom color gives aluminum the right sheen. Bead blasting before anodizing sets the texture. Laser marking handles logos and regulatory text down to 1.5 mm character height.

Weight matters too. Buyers notice a dummy that feels hollow. We can machine a thicker rear wall or add a steel slug in the cavity so the body lands within a few grams of the target handset, while keeping the outer envelope identical.

  • 1
    Anodize + blastClear, color or hardcoat over a uniform matte base.
  • 2
    Laser markingLogos and text at 1.5 mm minimum character height.
  • 3
    Weight tuningInternal ballast to match the real handset's heft.
Material and process choice

Which Route Fits Your Program

Pick by how the dummy will be used, not by what looks cheapest on the quote.

RequirementRecommended routeWhy
Retail display, needs real weight6061-T6 aluminum, anodizedMetal heft, durable edges, holds finish
Trade show, many unitsABS or PC, machined or vacuum castLower unit cost, light to ship
Transparent back panelPMMA machined and polishedOptical clarity, can be flame polished
Accessory fit testingAluminum, tight toleranceStable dimensions for repeated plug cycles
Photo and video propsAluminum, bead blastedMatte surface reads well on camera
Early ergonomic studyPOM or ABS, as-machinedFast turnaround, easy to revise
What else we run

Services Around the Dummy Program

One shop for the body, the fixture and the finish.

01

5 Axis CNC Machining

Simultaneous 5-axis centers for contoured shells and bezels that need one-setup accuracy.

02

CNC Milling & Turning

Milled bodies and turned inserts, pins and small metal details for the assembly.

03

Rapid Prototyping

First-article dummies in days so the design review does not wait on tooling.

04

Vacuum Casting

Silicone molds for 20 to 50 near-identical units with a consistent surface.

05

Part Surface Finishing

Anodizing, plating, powder coat, bead blasting, brushing and polishing in house.

06

Sheet Metal Fabrication

Display stands, trays and brackets that hold the dummies on the shelf.

Program parameters

What We Can Hold

Numbers below come from our standard shop capability.

ItemCapability
Tolerance±0.005 mm (±0.0002 in)
Surface finishRa 0.2–0.8 μm fine, Ra 0.8–1.6 μm high
Maximum part size4,000 mm
Aluminum alloys6061, 7075, 6082, 5052, 2024
PlasticsABS, PC, PMMA, POM, PEEK, PP, HDPE
Minimum orderOne prototype, no MOQ
Quote turnaroundQuotation and DFM within 12 hours
Production startWithin 24 hours of approval
Why GreatLight

Shop Facts, Not Slogans

What we own and what we can prove on paper.

15Y

Machining since 2011

Fifteen years of prototype and low-volume work, with three wholly-owned plants.

127

CNC machines on the floor

Including 16 simultaneous 5-axis centers and 16 mill-turn centers.

±0.005

Standard tolerance

Held on critical features and confirmed with CMM reports on request.

12h

Quote and DFM analysis

Send a STEP, IGES or X_T file and get feedback within half a day.

100%

Inspection before shipment

Raw material check, in-process monitoring and final inspection on every lot.

4

Quality systems in place

ISO 9001, IATF 16949, ISO 13485 and ISO 27001 certified.

7,600 m²Manufacturing space
150Technicians
<2%Historical late-delivery rate
10,000+Parts per run supported
Industry fit

Where These Dummies Go

option-1-concise-seo-focused

Accessory brand fit testing

Cases, screen protectors and cables need a body with stable outer dimensions. Requirement: repeatable ±0.05 mm on the port and button openings. We hold ±0.005 mm and check with CMM.

  • ±0.005 mm
  • CMM report
F19e67b4550897dce79a5e3c173cd093

Retail and trade-show display

Showroom units take handling and drops. Requirement: durable finish and realistic weight. We anodize 6061 and tune internal weight to match the target handset.

  • Anodized 6061
  • Weight tuned
De87b48e1260f26a6b5a054e191733d6

Engineering design review

Industrial design teams need a physical body to judge grip and button placement. Requirement: fast revisions. We machine one-off bodies and turn changes in days.

  • No MOQ
  • 3–5 day ship
FAQs

Questions Engineers Ask Before Ordering

What file formats do you need for a dummy body quote?

Send a STEP, IGES or X_T file, or a physical sample if the CAD is not released yet. We also accept 2D drawings with key dimensions marked.

Within 12 hours you get a quotation plus a DFM note listing any wall thickness, tool reach or tolerance issues we can see.

Can the dummy be dimensionally identical to the real phone?

Yes, to the extent your CAD model defines the outer envelope. We machine to the model and hold ±0.005 mm on critical features.

Be aware that internal cavities and antenna lines may not be in your file. If you need the dummy to match a real handset, send one for reference measurement or provide a full model.

Aluminum or plastic for a display dummy?

Aluminum if the dummy will be handled by customers, dropped, or needs realistic weight. Anodized 6061 holds up and reads like a real handset.

Plastic if you need many units at lower cost or the body is a temporary study piece. ABS and PC machine quickly and can be painted or vacuum cast for short runs.

How do you handle the camera bezel and button slots?

These are cut with micro-tooling, typically 0.5 to 2 mm end mills, on the same 5-axis setup as the outer profile.

Bezel height and step depth are checked against the CAD model. If the design has a very sharp internal corner, we will flag it in the DFM note because a standard cutter leaves a radius.

What surface finish matches a production handset?

For aluminum, bead blast then anodize at Ra 0.8–1.6 μm. That gives a matte surface close to a production phone and hides fingerprints in showroom lighting.

Mirror polish at Ra 0.2–0.8 μm is available but shows every touch mark. It suits photo props more than handling displays.

Will you sign an NDA for an unreleased product?

Yes. Uploads are kept secure and confidential, and we can sign your NDA or provide ours before you send files.

We do not share customer drawings, model names or program details.

What is the minimum order for a machined dummy?

One piece. There is no minimum order quantity, from a single prototype to a 10,000+ part run.

For quantities above roughly 50 units, vacuum casting or a short injection run may cost less than machining each body. We will say so in the quote if that is the case.

How fast can I get a dummy body?

Quotation and DFM feedback come back within 12 hours. Production can start within 24 hours of approval, and parts typically ship in 3–5 days.

Complex multi-part assemblies or heavy finishing may add time. We tell you the expected ship window in the quote instead of after the order.

Send Your CAD, Get a Quote in 12 Hours

Upload a STEP or IGES file and our engineers return a price, a DFM note and a ship window. One piece or ten thousand, the same process.

12-hour quote100% inspectionNo MOQNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC