GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

3D Printing & Rapid Prototyping

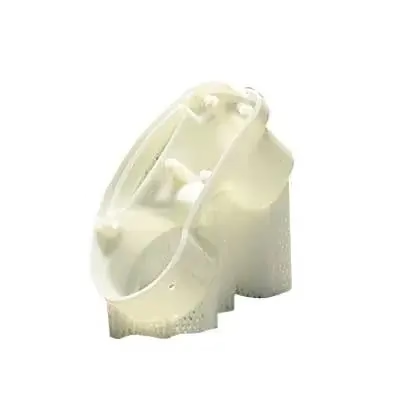
Auto Part Plastic ABS Models

Print ABS, PC, PA and resin prototypes for bumper clips, housings, ducts and interior trim. Check fit and finish before you commit to a mold. DFM feedback lands within 12 hours.

SLA / SLS / FDM / MJFABS, PC, PA, resinNo MOQ3–5 day shipping
Automotive-front-bumper-plastic-rapid-prototyping-jpg
±0.005 mmMachining tolerance
127High-precision CNC machines
12 hQuote and DFM analysis
15 yearsSince 2011
Common Problems

Where plastic prototypes go wrong

Most of these show up after the print, not during it.

01

The print fits, the molded part will not

SLA resin and ABS shrink at different rates. When the printer ignores that difference, your snap-fit tabs pass on the bench and fail in the tool. Shrink compensation has to be dialed in per material, per wall thickness, before the first print leaves the machine.

02

Layer lines show through the Class A surface

A bumper fascia printed at 0.2 mm layer height will telegraph every step once it is painted. Buyers reject it at the review. You need either a finer layer height, vapor smoothing, or a primer and sand cycle budgeted into the quote.

03

The material is not the grade under the hood

Standard ABS softens around 90 °C. An under-hood bracket printed in it will creep against a hot engine cover. Glass-filled PA, PC-ABS or PEEK costs more per part, but it is the only way to get a meaningful heat and chemical test.

04

Three suppliers, three sets of numbers

One shop prints the housing, another machines the insert, a third does the finish. Nobody owns the assembly tolerance. First-article inspection reveals the stack-up is wrong, and the review slips two weeks while everyone points elsewhere.

How We Build It

One workflow from CAD file to testable auto part plastic

Print, machine and finish under one roof in Dongguan.

SLA-3d-Printing-jpg
Process Selection

Pick the process from the part, not the price list

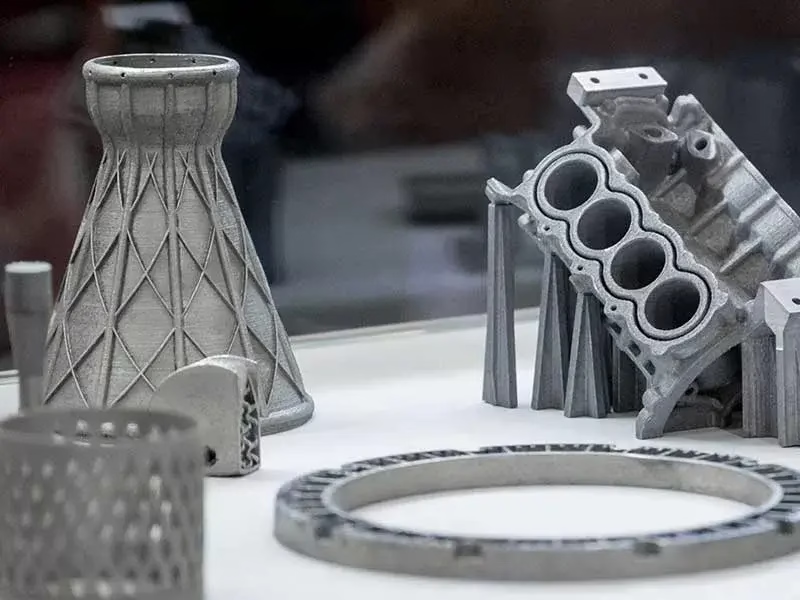
SLA holds fine detail for clips and grilles, but resin is brittle. SLS in PA12 gives you living hinges and snap-fits that survive repeated assembly. FDM in ABS or PC is the cheap way to check a bracket envelope, though layer bonding limits it in thin walls. MJF sits between SLS and injection molding for short runs of 20 to 200 units.

We ask what the model has to prove. A clearance check across a 400 mm fascia does not need the same process as a latch that will be cycled 500 times. Send the drawing and we will say which route fits and which one wastes your budget.

  • 1
    SLATight detail, smooth surface, brittle in thin sections.
  • 2
    SLS / MJFFunctional PA parts, snap-fits, small batches.
  • 3
    FDMFast and cheap for form and envelope checks.

Get Instant Quote

Rapid-3D-Printing-Services-jpg
Fit & Finish

Close the gap between prototype and production part

A printed model is only useful if the numbers transfer. We compensate for material shrink, add machining allowance where an insert seat needs a tight bore, and check the assembly stack before anything ships. Where a plastic part meets metal, we machine the mating insert on the same tolerance basis as the print.

Post-processing decides whether the part reads as a prototype or a production sample. Bead blasting knocks down layer texture. Primer, sand and paint get you to a Class A look for a show build. Laser marking puts part numbers on at a minimum character height of 1.5 mm.

  • 1
    Shrink compensationPer material and wall thickness, not a fixed factor.
  • 2
    Metal insertsMachined here, checked against the print in assembly.
  • 3
    FinishingBead blast, paint, texture, laser mark.
Selection Guide

Match the process to what the part must prove

Use this before you request a quote.

ProcessBest forWatch out for
SLAFine detail, smooth show surfacesBrittle thin walls, UV ageing
SLS (PA12)Snap-fits, living hinges, ductsPorous surface, grainy texture
FDM (ABS / PC)Envelope and clearance checksWeak layer bonding in Z
MJF (PA12)Runs of 20–200 functional partsLess detail than SLA
Vacuum casting10–50 urethane parts off one masterShorter tool life than steel
CNC (ABS / POM)Tight bores, threads, insert seatsHigher cost per part
What We Do

Services behind a printed auto part plastic model

Printing is one step. These are the others.

01

Custom 3D Printing

SLA, SLS, FDM, MJF and SLM. Choose the process by what the part has to prove, not by the cheapest rate.

02

Rapid Prototyping

One-off models and small batches, with DFM feedback before the machine starts.

03

5 Axis CNC Machining

16 simultaneous 5-axis centers for metal inserts, test fixtures and short-run plastic parts.

04

CNC Milling & Turning

Tight bores, threads and sealing faces on ABS, POM, PEEK and aluminium.

05

Vacuum Casting

Urethane parts off a printed or machined master when you need 10 to 50 units with a consistent color.

06

Part Surface Finishing

Bead blasting, tumbling, polishing, painting, anodizing and laser marking to your callout.

Scope

What a printed auto part plastic order includes

ItemIncludedDetail
DFM reviewYesQuotation and analysis within 12 hours
MaterialsABS, PC, PA, POM, PEEK, PP, resinGlass-filled grades on request
Build sizeUp to 4,000 mm processing sizeLarge parts split and bonded
Tolerance±0.005 mm on machined featuresPrint tolerance is process dependent
Inspection100% before shipmentReports on request
Minimum orderNo MOQOne prototype to 10,000+ parts
ConfidentialityNDA availableSecure uploads
Why GreatLight

Reasons engineers keep sending the next revision here

2011

15 years in business

Founded in 2011. Three wholly-owned plants and 150 technicians across Dongguan and Singapore.

127

High-precision machines

16 simultaneous 5-axis centers, 16 mill-turn centers and a Ø400 mm rotary table for insert machining.

±0.005 mm

Machining tolerance

Held on insert seats and mating bores, so the printed body and the metal part agree.

12 h

Quote turnaround

Quotation and free DFM analysis within 12 hours. Production can start within 24 hours.

IATF

16949:2016 certified

Also ISO 9001:2015, ISO 13485:2016 and ISO 27001:2022. Documentation available on request.

100%

Inspection before shipment

Raw material check, in-process monitoring and final inspection on every order.

7,600 m²Manufacturing space
150Technicians
3Wholly-owned plants
99.99%Qualification rate
Industry Fit

What automotive and EV programs ask for

Custom Auto Spare Parts 5 Axis CNC Machining Engine Parts

Under-hood brackets

Heat and vibration test parts in glass-filled PA or PEEK, with machined metal inserts.

  • ±0.005 mm
  • IATF 16949
Calculating Long-Term Value of High-Accuracy CNC Auto Parts

Interior trim and clips

Snap-fit checks in SLS PA12 that survive repeated assembly and disassembly.

  • No MOQ
  • 3–5 day ship
Experience the GreatLight Advantage in Auto Parts Processing!

EV housings and ducts

Large covers printed in sections, bonded and checked for flatness before assembly.

  • 4,000 mm
  • 100% inspection
GreatLight Your Premier Partner for Precision Auto Parts Processing Custom CNC Machined Solutions

Sensors and connector bodies

Tight bores and sealing faces machined in plastic, checked against the printed housing.

  • Ra 0.8–1.6 μm
  • NDA available
FAQs

Questions we get before the first print

Which process should I use for an ABS model of an auto part?

It depends on what the model has to prove. For a form and envelope check, FDM in ABS is the fastest and cheapest route. For snap-fits and living hinges that get cycled, SLS or MJF in PA12 holds up far better.

SLA gives the crispest detail and the smoothest surface, but resin is brittle in thin walls. If the part will be painted to a Class A look, SLA plus primer and sand is usually the better starting point.

Can you match the shrink of the production material?

Yes, within limits. We compensate per material and wall thickness rather than applying one fixed factor across the whole part.

Tell us the production resin and the gate location if you have them. That gets the compensation closer on the first print instead of the third.

How do you handle a part larger than the build envelope?

We split the model along low-stress lines, print the sections, then bond and finish them. The joint is planned in CAD, not improvised on the bench.

The maximum processing size here is 4,000 mm. For long trim pieces or full-width covers, we will tell you where the split should sit and how flatness will be checked after bonding.

Do printed plastic parts need support removal and sanding?

Most do. FDM and SLA both need supports, and the witness marks show after painting if they are not dressed back.

We remove supports, sand the contact areas and bead blast where the finish callout allows it. If the part is going to a Class A surface, primer and sand cycles are quoted as a separate line so you can see the cost.

What tolerances can I put on a printed model?

Print tolerance depends on the process, part size and geometry. It is not a single number you can write on the whole drawing.

Where a feature needs to hold a tight fit, we machine it. Machined features on ABS, POM or aluminium hold ±0.005 mm, and those are the numbers we will stand behind.

Can you make the matching metal insert too?

Yes. With 16 simultaneous 5-axis centers and 16 mill-turn centers in-house, the insert is machined on the same tolerance basis as the plastic part.

That matters for a stack-up. One shop owning both sides of the joint removes the argument about whose dimension is wrong.

How fast can I get parts, and is there a minimum order?

Quotation and free DFM analysis come back within 12 hours. Production can start within 24 hours, and parts ship in 3 to 5 days.

There is no minimum order quantity. One prototype or a 10,000-part run both go through the same inspection process. We do not quote a guaranteed delivery date before the drawings are reviewed.

How is my design kept confidential?

Uploads are secure and confidential. An NDA is available on request before you send files.

We are ISO 27001:2022 certified for information security, and inspection reports are issued only to the contacts you name.

Send the CAD file and get a real answer

Tell us what the model has to prove. An engineer reviews the geometry, picks the process and comes back with a quote and DFM notes within 12 hours.

12-hour quote100% inspectionNo MOQNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC