GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Motorcycle Component Machining

CNC Motorcycle Parts

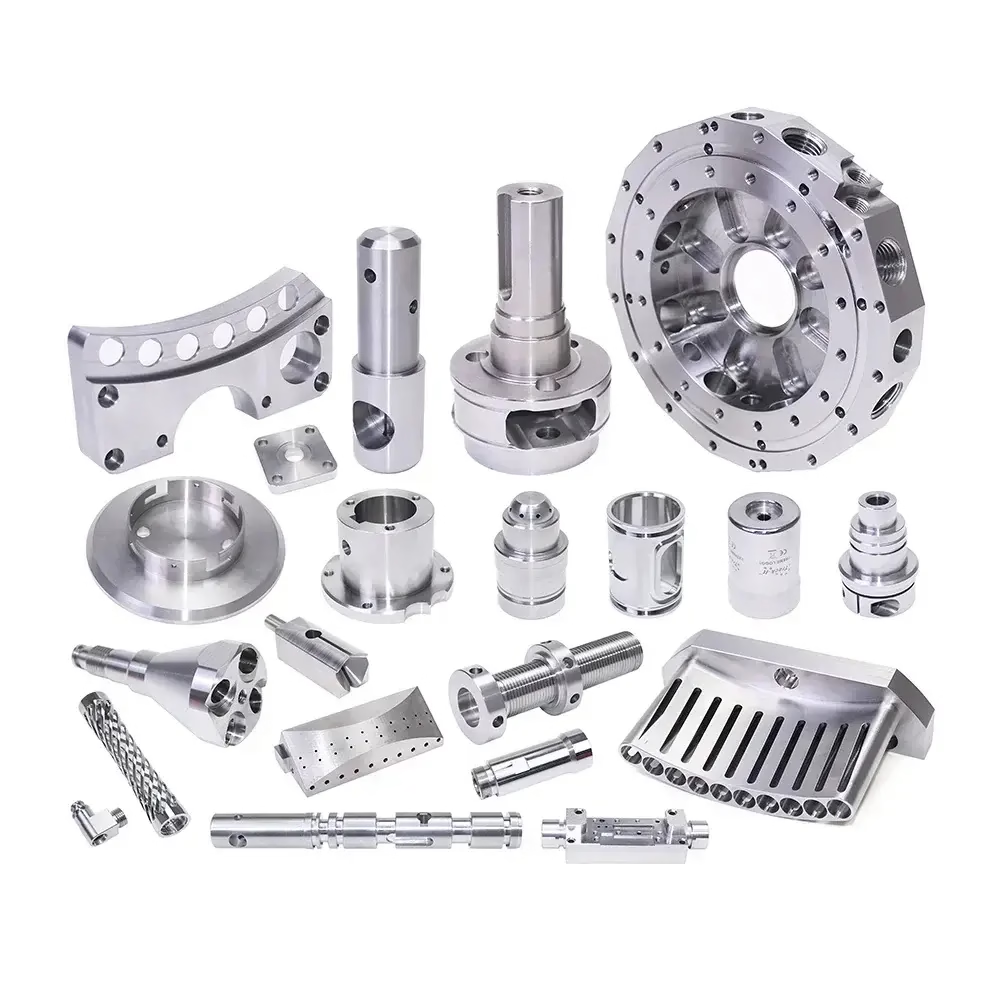
Brass, titanium and stainless components machined on 5-axis mill-turn centers. Tolerances to ±0.005 mm, finishes from as-machined to Ra 0.2–0.8 μm, and a DFM report back within 12 hours.

±0.005 mm toleranceBrass C36000Ti-6Al-4VNo MOQ12-hour quote100% inspection
titanium-cnc-machining
127High-precision CNC machines
16Simultaneous 5-axis centers
±0.005 mmAchievable tolerance
15 yearsMachining since 2011
Where parts fail

Four Problems That Show Up After Assembly

Most motorcycle part defects are not random. They trace back to a process decision made early.

01

Threads that gall on titanium

Ti-6Al-4V galls against stainless fasteners when the thread is cut dry or the pitch diameter runs to the low limit. The joint seizes at final torque and the part is scrapped. Thread milling plus a controlled pitch diameter range avoids it.

02

Brass fittings that crack at the hex

C36000 machines fast, but the sharp corner between hex and shank concentrates stress. Under vibration the fitting cracks within a few hundred hours. A generous radius plus a stress-relief pass fixes it.

03

Bores that drift after anodizing

Hardcoat anodizing adds 25–50 μm per surface. A bore toleranced at ±0.01 mm before coating closes up and the bearing will not seat. We mask critical bores or pre-machine undersize.

04

Lead times quoted before the print is read

A shop quotes three weeks, then finds a 0.4 mm wall and a deep pocket that needs a custom tool. Production stalls. We return a DFM report with the quote so the schedule is real.

How we machine them

One Setup, Fewer Stack-Ups

Turning, milling and drilling on the same machine reduces the error that accumulates across fixtures.

CNC Lathe Technical Specifications Terminology
Mill-turn

Turned and milled features in one setup

Motorcycle parts mix round and non-round features: a shaft body with a flat, a hub with drilled flanges, a fitting with a hex and a cross-hole. Each extra fixture adds a datum shift. Our 16 mill-turn centers cut OD, bore, thread and cross-features without releasing the part.

For brass and titanium this matters more than for aluminum. Brass moves under light clamping, titanium springs back after the cut. Keeping one datum through the operation removes both problems from the tolerance stack.

  • 1
    16 mill-turn centersTurning plus milling in a single chucking
  • 2
    Ø400 mm rotary table4-axis indexing for cross-holes and flanges
  • 3
    ±0.005 mmPosition tolerance across milled features

Get Instant Quote

CNC Machining Services Online
Material behavior

Cutting parameters chosen per alloy, not per family

Titanium conducts heat poorly. The cutting edge keeps the heat, so a tool that runs fine in 6061 burns through in Ti-6Al-4V. We run lower surface speed, higher feed per tooth and flood coolant, and we change inserts on a count rather than on a squeal.

Brass C36000 is the opposite case. It cuts clean at high speed, but leaded grades are not suited to every application, and thin walls deflect if the chuck pressure is set for steel. Beryllium copper and C27400 get their own programs and their own inspection plan.

  • 1
    Titanium TA1, TA2, TC4Low speed, high feed, rigid tooling
  • 2
    Brass C36000, C27400High speed, light clamping for thin walls
  • 3
    17-4PH, 316L, 303Stainless grades with controlled work hardening

Get Instant Quote

Selection guide

Which Process Fits Your Part

Use this to pick a route before you send a print.

Part featureRecommended routeWhy
Shaft under Ø60 mm, round features onlyCNC turningSingle-axis work, lowest cost per part
Shaft with flats, cross-holes or a hexMill-turnOne datum, no second fixture
Complex bracket, 5 faces5-axis machiningFewer setups, tighter feature-to-feature position
Thin-wall brass fittingTurn, light clamp, radius cornersPrevents deflection and stress cracking
Titanium threaded insertThread mill, not tapControls pitch diameter, avoids galling
Small batch, 1–50 piecesNo dedicated fixtureSetup cost stays out of the unit price
What we run

Machining Services for Motorcycle Components

Most parts use one of these routes. Some use three.

01

5-Axis CNC Machining

Linkages, triple clamps and housings with features on five faces. 16 simultaneous 5-axis centers, up to 4,000 mm travel.

02

4-Axis CNC Machining

Cross-drilled shafts, hubs and flanges indexed on a Ø400 mm rotary table.

03

3-Axis CNC Machining

Plates, covers and brackets where all features sit on one face. 27 machines available.

04

CNC Milling & Turning

Turned bodies, spacers and fittings, with milled flats and drilled patterns in the same setup.

05

Rapid Prototyping

One-off fit checks before tooling. No minimum order quantity, prototype to 10,000+ parts.

06

Part Surface Finishing

Anodizing, plating, powder coating, bead blasting, brushing and laser marking in house.

Scope

Tolerance, Finish and Inspection

Numbers are what we hold on production, not best-case lab results.

ParameterCapabilityNotes
General tolerance±0.005 mm±0.0002 in on critical features
Fine finishRa 0.2–0.8 μmBearing bores, seal surfaces
Standard finishRa 0.8–1.6 μmMost mating surfaces
As-machinedRa 1.6–3.2 μmNon-critical faces
Maximum part size4,000 mm4,000 × 400 × 150 mm travel
Inspection100% before shipmentReports on request
Laser marking1.5 mm min character heightPart numbers, traceability
Qualification rate99.99%Measured on shipped lots
Why GreatLight

Six Reasons Engineers Keep Sending Prints

15Y

Machining since 2011

Fifteen years on turned and milled metal parts, three wholly-owned plants and 7,600 m² of floor space in Dongguan.

127

CNC machines on site

16 simultaneous 5-axis centers, 12 four-axis mills, 27 three-axis machines and 16 mill-turn centers. Scheduling stays inside our walls.

±0.005

Millimeter tolerance

Held across milled features, not just on a turned diameter measured at the machine.

12h

Quote and DFM report

Drawing in, quotation plus manufacturability notes back within 12 hours.

3–5d

Days to ship

Production can start within 24 hours once the print and material are confirmed.

IATF

16949 and ISO 9001

Also ISO 13485 for medical and ISO 27001 for information security. NDA on request.

99.99%Qualification rate
<2%Historical late-delivery rate
150Technicians
ISO 27001Secure file handling
Industry fit

What These Parts Have to Survive

oplus_262178

Powertrain and drivetrain

Spacers, adapters and mount blocks that see constant load and heat cycling.

  • ±0.005 mm
  • 17-4PH
  • 100% inspection
6011

Brake and suspension hardware

Calipers mounts, linkage arms and bushings where a bore that drifts ruins the fit.

  • Ra 0.8–1.6 μm
  • 6061-T6
  • Mill-turn
GreatLight Metal new factory building

Fuel and hydraulic fittings

Brass bodies with cross-holes and tapered threads that must seal on the first torque.

  • C36000
  • Thread milled
  • Pressure tested
Leader in Cnc Machining Service China

Custom builds and prototypes

One-off brackets and adapters for frame changes, before any tooling is cut.

  • No MOQ
  • 3–5 days
  • 12-hour quote
FAQs

Questions We Get Before the First Order

Can you machine titanium motorcycle parts without galling the threads?

Yes, if the thread is milled rather than tapped. Thread milling lets us hold the pitch diameter in a controlled band instead of running to the low limit, which is where galling starts.

We also specify the mating fastener material. A titanium part with a titanium bolt needs a dry-film lubricant or a different alloy pair. We flag that in the DFM report.

Is brass strong enough for a load-bearing part?

It depends on the grade. C36000 is free-machining and good for fittings, spacers and low-load bushings. C27400 and beryllium copper carry more load and wear better.

For a stressed bracket, aluminum 7075 or 17-4PH is usually the better answer. We will say so rather than quote brass.

What tolerance can you actually hold on a long shaft?

±0.005 mm on diameters up to the machine capacity, but length matters. Beyond roughly 300 mm, thermal growth and deflection start to eat into that.

On long shafts we hold ±0.01 mm as a working tolerance and inspect at 20 °C. If you need tighter, we discuss a temperature-controlled cut and a slower cycle.

How do you handle anodizing on a part with tight bores?

Hardcoat adds 25–50 μm per surface, so a bore needs to be pre-machined undersize or masked. We decide which in the DFM review.

The drawing should call out which surfaces are functional. Coating everything usually means the critical bore is out of tolerance when the parts come back.

Do you run small batches or only volume?

There is no minimum order quantity. We run single prototypes and batches over 10,000 parts on the same equipment.

For one or two pieces we skip dedicated fixtures, so setup cost stays low. For volume, we build fixtures and cut cycle time.

What files do you need for a quote?

A STEP, STP, IGES or X-T file plus a 2D drawing with tolerances, material and finish. SolidWorks, Pro/Engineer, AutoCAD DXF and DWG all work.

A PDF or TIF drawing is fine if that is what you have. Missing tolerances get flagged rather than guessed.

How do you check parts before they ship?

Raw material is verified on receipt, dimensions are monitored during the run, and every part gets a final inspection before packing.

We use CMM, tool microscope, multi-joint arm, height gauges and roughness measurement. Reports are available on request.

Can you sign an NDA before we send drawings?

Yes. NDAs are available on request, and uploads are handled as confidential. We hold ISO 27001:2022 for information security.

We do not share customer drawings, part numbers or project details.

Send a Drawing, Get a Quote and a DFM Report

Upload your STEP file and 2D print. We come back within 12 hours with pricing, lead time and any manufacturability notes worth acting on.

12-hour quote100% inspectionNo minimum order quantityNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC