
Matrix CNC machining guide
This guide explains what matrix CNC machining means on the shop floor: many axes cutting at once, one setup, and a toolpath that never stops moving. It is written for design engineers and buyers who need to decide whether a part belongs on a matrix machine or on a 3-axis mill. Read it and you can judge setup count, tolerance risk and cost before you send an RFQ.
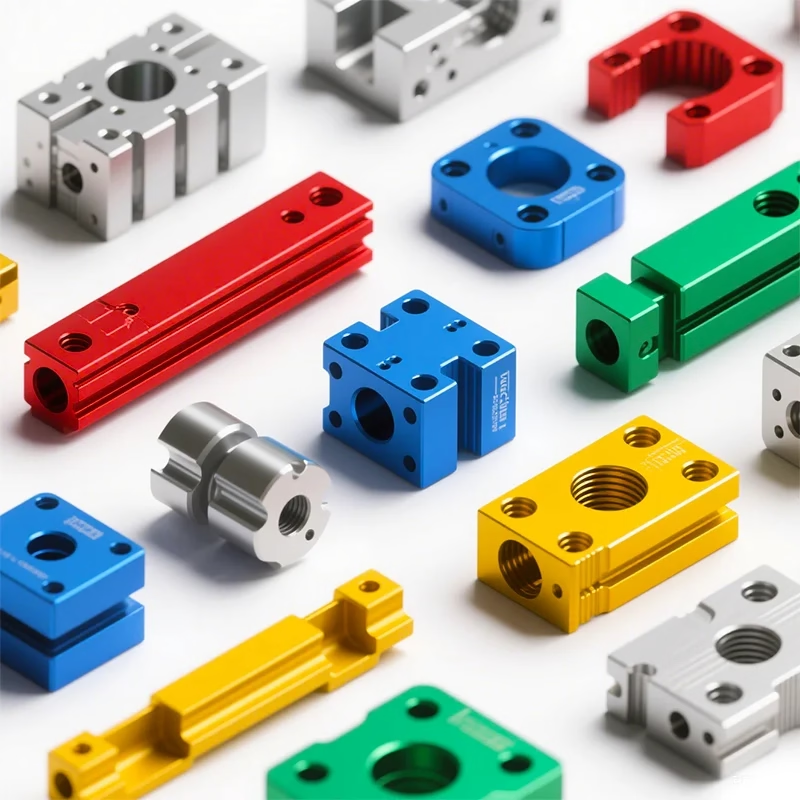
What matrix CNC machining actually means
The word matrix here does not describe a machine brand. It describes the way the machine moves. Instead of three linear slides that meet at 90°, a matrix machine carries several linear and rotary axes at the same time, so the tool can approach a face from an angle that a 3-axis mill simply cannot reach. The controller solves all axes together, in one block of motion.
That single solved motion is the whole point. On a 3-axis mill, every new face means a new setup: unclamp, rotate the part, re-zero, cut again. Each of those steps adds a datum shift. On a matrix machine, the rotary table and the spindle tilt while the tool stays in cut, so five faces of a block can come off one clamping.
The practical result is fewer datums. A part that needs four setups on a 3-axis machine may need one on a matrix machine. Every setup you remove also removes a stack of errors: fixture runout, chip trapped under a locator, operator re-zeroing. That is why matrix work often holds ±0.005 mm across features that sit on different faces.
Matrix machines are not magic. They are slower to program, they need more clearance around the part, and they cost more per hour. The gain is real only when the geometry has features on several faces, or when a single datum chain must run from one face to another. For a flat plate with holes on one side, a 3-axis mill wins on price.
At GreatLight we run 16 simultaneous 5-axis machining centers, 12 four-axis mills and 27 three-axis machines. Parts from one prototype to 10,000+ piece runs go through the same inspection routine: raw material check, in-process monitoring, final inspection before shipment.
- 1Many axes, one setupLinear and rotary axes move together under one controller solution.
- 2Datums stay putFewer re-clampings means a shorter tolerance chain.
- 3Not for flat platesSimple one-face parts are cheaper on a 3-axis mill.
How the controller solves multiple axes at once
A matrix toolpath is written in the part coordinate system, not in machine coordinates. The CAM system posts a cutter location and a tool axis vector, and the control works backward to find the slide positions that put the tool there. That backward step is the kinematics solution, and it runs thousands of times per second.
Rotary axes change the effective feed rate. When the table turns, a point 200 mm from the center of rotation travels much faster than a point near the center. The control has to slow the linear axes so the cutting edge does not overload. Feed rates that look fine in the CAM simulation can still chirp in the cut if the post processor ignores this.
Singularities are the other trap. A trunnion machine loses an axis of control when the tool axis lines up with the rotary axis. Near that point the rotary table has to spin very fast to keep the tool oriented, and the surface finish shows it. Good programmers tilt the part or the fixture a few degrees so the toolpath never passes through the singularity.
Rigidity sets the real limit. A rotary axis hanging off the end of a linear axis is a cantilever, and cantilevers deflect. Deep pockets in hard steel still want a short, stiff tool and a 3-axis approach, even if the part is complex overall. Mix the two methods and the cycle time drops.
Thermal drift matters too. Five servos generate more heat than three, and a warm ball screw grows. On long cycles we let the machine idle to temperature, then touch off the tool probe again before the finishing pass.
- 1Post processor qualityFeed and orientation logic lives in the post, not the CAD model.
- 2Avoid singularitiesTilt the fixture so the tool axis never aligns with the rotary axis.
- 3Rigidity firstCantilevered rotary setups deflect under heavy radial load.
Which parts belong on a matrix machine
Look at the drawing and count the faces that carry toleranced features. One face means 3-axis. Two or three faces at right angles can still be done with a tombstone fixture and two setups. Four or more faces, or any feature whose position is measured from a face that is not the base, points to multi-axis work.
Angled holes are the clearest signal. A hole drilled at 30° to the surface on a 3-axis machine needs a wedge fixture, and the wedge itself has to be set with a dial indicator. A matrix machine tilts the head and drills it in one pass. If the part has five such holes at different angles, the case is settled.
Undercuts and swept surfaces behave the same way. A ball nose tool on a 3-axis machine cannot reach behind a lip. A tilted tool can. Impellers, turbine blades and impeller-like housings are classic matrix parts for this reason, and they are common in aerospace and energy work.
Size is a boundary too. GreatLight machines up to 4,000 mm in the largest configuration, with travels of 4,000 × 400 × 150 mm on the long-bed machines, 750 × 1,150 × 550 mm and 600 × 600 × 600 mm on the mid-size centers, and 500 × 500 × 450 mm or 500 × 310 × 200 mm on the compact ones. A Ø400 mm rotary table sets the limit for turned-and-milled parts.
Material matters less than people expect, but hard alloys shrink the sweet spot. Titanium TA1, TA2, TC4 and Inconel cut slowly and wear tools fast, so a matrix setup earns its cost only when the geometry truly needs it. Aluminum 6061, 7075, 6082 and stainless 303, 304, 316L, 17-4PH give more headroom.
- 1Count the toleranced facesFour or more faces usually justifies multi-axis work.
- 2Angled featuresHoles and slots off the normal axis favor a tilting spindle.
- 3Hard alloysTitanium and Inconel raise cost, so confirm the geometry needs it.
Workholding, toolpath strategy and inspection
Workholding decides whether the matrix setup pays off. If the fixture blocks two of the faces you want to machine, you gained nothing. We design soft jaws or a custom nest so the part sits on three points and the tool can reach around it. For thin walls, a low-melt alloy or vacuum chuck spreads the clamping load.
Toolpath strategy follows the tolerance map. Features that must hold ±0.005 mm relative to each other are cut in the same operation, with the same tool, after the machine has warmed up. Surfaces that only need Ra 1.6–3.2 μm can be cut in a separate pass at a higher feed. Splitting the work this way keeps the cycle honest.
Finish calls are part of the plan, not an afterthought. Anodizing, electroless nickel, zinc plating, powder coating and black oxide all add or remove a few micrometers. If a bore has to accept a bearing after hardcoat anodizing, the pre-finish size has to be offset. Bead blasting and tumbling can also round a sharp edge you wanted to keep.
Inspection closes the loop. We inspect 100% of parts before shipment, with reports on request, and the same routine runs for a single prototype and for a 10,000 piece run. For matrix parts we check feature-to-feature position, not just individual sizes, because that is where multi-axis error shows up first.
- 1Fixture as part of the designLeave clearance for the tool to reach every toleranced face.
- 2Group tight featuresCut the ±0.005 mm features in one warm-up operation.
- 3Plan the finishCoating thickness changes bore sizes; offset before plating.
3-axis, 4-axis or matrix setup: which one fits
Use this as a first pass before you request a quote.
| Part feature | Best setup | Why | Watch out for |
|---|---|---|---|
| Flat plate, holes on one face | 3-axis | One datum, short cycle | Nothing major |
| Part with two opposite faces | 4-axis with tombstone | Two setups, good rigidity | Fixture runout |
| Four or more toleranced faces | Matrix 5-axis | One clamping, one datum chain | Higher hourly rate |
| Angled holes at several angles | Matrix 5-axis | Head tilts, no wedge fixture | Singularity near axis alignment |
| Undercut or swept surface | Matrix 5-axis | Tilted tool reaches behind lips | Longer CAM time |
| Deep pocket in hard steel | 3-axis plus matrix finish | Short stiff tool for roughing | Tool deflection |
| Large frame up to 4,000 mm | Long-bed 3-axis or gantry | Travel sets the limit | Thermal drift |
| Thin-wall housing | Matrix 5-axis | Light finishing passes, less re-clamp | Chatter, workholding marks |
When to pick which
If the part has one flat side and holes on one face, send it to a 3-axis mill and keep the cost down. If it has four or more toleranced faces, an angled hole pattern, or an undercut a straight tool cannot reach, use matrix CNC machining and pay for one clamping instead of four.
Common questions about matrix CNC machining
Is matrix CNC machining the same as 5-axis machining?
In daily shop language, yes. Both mean several linear and rotary axes solved together so the tool can reach a face without re-clamping the part.
A true matrix setup also includes the fixture and CAM strategy. Two shops with the same machine can deliver very different results if one of them still programs face by face.
How tight a tolerance can a matrix setup hold?
GreatLight works to ±0.005 mm (±0.0002 in) on multi-axis work, with surface finish between Ra 0.2–0.8 μm on fine finishing passes.
The number only holds when the tight features are cut in the same operation on a warm machine. A tolerance split across two setups will drift, no matter how good the machine is.
When is a 3-axis mill the better choice?
When every toleranced feature sits on one face, or when the part is a simple plate, bracket or bushing.
A 3-axis cycle is usually shorter and the hourly rate is lower. Adding rotary axes to that part buys nothing and adds CAM time.
What materials can be machined this way?
Aluminum 6061, 2024, 5052, 6082, 7075 and ADC12; stainless 303, 304, 316L, 17-4PH; steels 1018, 1045, 4130, 4140, 4340; copper and brass C101, C110, C36000; titanium TA1, TA2, TC4 and Inconel.
Hard alloys such as Inconel cut slowly and wear tools, so we only route them through a matrix setup when the geometry needs the extra axes.
How many parts do I need to order?
There is no minimum order quantity. We run one prototype or 10,000+ parts on the same process.
Quotation and a free DFM analysis come back within 12 hours, and production can start within 24 hours after that.
How do you protect my drawings?
Uploads are secure and confidential, and we sign an NDA on request before any file review.
If you want to see how a similar part was cut, ask for samples from the sample center instead of sending production files.
Send a drawing, get a setup plan
Share the part and we will tell you which faces need multi-axis work, which can stay on 3 axes, and where the tolerance risk sits. Quotation and free DFM analysis within 12 hours.
12-hour quote100% inspectionNo minimum orderNDA on request
More from GreatLight
We publish setup notes, tooling trials and inspection data from the factory floor.











