
Why Are G Codes Used in CNC Machining?
G codes are the instruction set that tells a CNC machine where to move, how fast to feed, and when to change tools. This guide explains the engineering reasons behind them and walks through the faults engineers see most often on the shop floor.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
Symptom, likely cause, and what to do
Use this table when a proven program still produces bad parts or alarms out.
| Symptom | Likely cause | Action |
|---|---|---|
| Part is oversize by a constant offset | Wrong work offset or tool length stored | Re-measure G54 and tool length, re-post |
| First part is good, part 200 drifts | Thermal growth in spindle or ball screw | Add warm-up cycle, re-check offsets mid-run |
| Alarm on G00 rapid move | Rapid path crosses a clamp or fixture | Set G00 to clear plane, use G01 approach |
| Corners are rounded on a pocket | Excessive feed with no exact stop | Add G61 or reduce feed at corners |
| Thread is torn or galled | Wrong pitch feed or spindle sync lost | Check G76 values and encoder cable |
| Surface finish is chatter marked | Feed and speed outside cutter window | Adjust feed per tooth, check tool runout |
| Machine stops mid-cycle with no alarm | Optional stop or block skip left active | Clear M01 and block skip, restart from line |
| Hole position is off in one axis only | Backlash or lost motion on that axis | Check backlash comp, inspect thrust bearing |
Why are g codes used in cnc machining instead of manual control?
A G code is a preparatory command that tells the machine what kind of motion or state to enter. G00 moves at rapid traverse, G01 cuts in a straight line at a defined feed, G02 and G03 cut arcs, and G81 through G89 cover canned drilling cycles. The machine reads these words in blocks, one line at a time, and executes them in order. That is the whole idea: replace a handwheel and a skilled operator's judgment with a set of numbers the controller can repeat exactly.
The reason this matters for g codes used in cnc machining is repeatability. Once a program is proven, the first part and the ten-thousandth part come off the same set of coordinates. Human error in reading a dial or counting handwheel turns disappears. For work held to ±0.005 mm, that is the difference between a process and a gamble.
G codes also separate geometry from machine behavior. Coordinates define where the tool goes. G codes define how it gets there, how fast, and with what coolant. A CAM system can regenerate the geometry for a design change without touching the motion logic. On a 5-axis job with a Ø400 mm rotary table, that separation keeps the post-processor manageable.
- 1Motion controlG00, G01, G02, G03 cover rapid, linear, and arc moves.
- 2CompensationG41 and G42 shift the path for cutter radius without editing geometry.
- 3CyclesG81–G89 shorten drilling, tapping, and boring code.
- 4Units and datumG20/G21 and G54–G59 set scale and work origin.
How a G code block is structured and why order matters
Most controllers accept a block in a loose order, but the machine executes modal states in a fixed sequence. Feed rate, spindle speed, tool change, and coolant are set before the move that uses them. If M03 spindle start appears after the G01 line, the first cut happens with a stationary spindle. That is a crash, not a typo.
Modal G codes stay active until cancelled. G01 remains in effect for every following block until a G00 or G02 appears. This is efficient, but it is also where many scrap parts come from: an operator edits one line, forgets the mode carries forward, and the next twenty moves run at the wrong feed.
M codes handle everything that is not axis motion. M06 changes tools, M08 floods coolant, M09 stops it, M30 ends the program and rewinds. The controller interleaves these with G codes in a single sequence. When a machine alarms on a tool change, the fault is usually in the M06 line or the tool table, not the G code itself.
On our 127 machines, we keep a standard header block for every job: units, absolute mode, work offset, safe Z, and spindle direction. It costs ten seconds and removes a whole class of setup errors.
Which parts benefit most from g code programming
Parts with repeated features are the clearest case. A manifold with twelve identical bolt holes, or a bracket family that shares a mounting pattern, becomes a short subprogram called with M98. Change the pattern once and every instance updates. Hand programming the same hole twelve times invites a transposition error on the ninth.
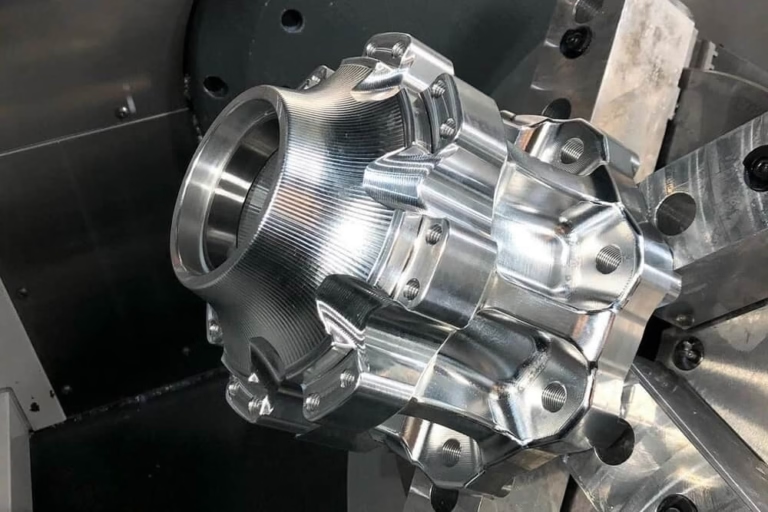
Complex contours are the second case. Free-form surfaces, undercuts, and internal channels cannot be cut by turning two dials. They need a toolpath computed from the CAD model, posted as thousands of small linear moves. A 5-axis simultaneous cut on a titanium impeller is not something a manual machinist can reproduce by feel.
High-mix, low-volume work benefits differently. When you run one prototype today and fifty parts next month, the program is the process record. The setup sheet, offsets, and feeds are all captured. We hold ±0.005 mm across prototype and production runs because the same code drives both.
- 1Repeated patternsSubprograms and cycles cut programming time and error.
- 2Free-form geometryCAM-posted paths handle surfaces manual control cannot.
- 3Regulated industriesAerospace, medical, and automotive work needs traceable motion.
- 4Family partsParameterized code adapts one program to several sizes.
When g code programming is not the right answer
For a one-off repair on a worn shaft, writing a full program is slower than turning it by hand. Manual lathe work still wins when the geometry is simple, the quantity is one, and the tolerance is loose. We say this to customers who ask us to program a single chamfer.
G codes cannot see the part. They have no idea the stock is 0.5 mm oversize or that a previous operation left a step. Adaptive control and in-process probing fill that gap, but they add cost. If the blank varies from part to part, no program will save you; you need to control the incoming material first.
Code also cannot fix a bad setup. A fixture that lifts under cutting force will produce a tapered wall no matter how clean the program is. When we troubleshoot, we check the fixture before we touch the G code. Roughly half the tolerance problems we see trace back to workholding or thermal drift, not the program.
Step by step: isolating a G code fault
Work through these in order. Stop as soon as the symptom changes.
- 1Confirm the symptom is repeatableRun the same program on the same material twice. If the error moves, suspect thermal drift or workholding, not the code. Note the axis and the direction of the error.
- 2Check work offset and tool lengthRe-measure G54 through G59 and every tool in the pocket. A single wrong tool length shifts one feature, not the whole part. Compare the offset value to the setup sheet.
- 3Read the active modal stateLook at the controller's modal display before the suspect block. Confirm G90 absolute, G21 metric, and the correct plane (G17 for XY arcs). A leftover G91 incremental mode explains a lot of sudden over-travel.
- 4Dry run with rapids raisedRun the program with a +50 mm Z offset and feed override at 20%. Watch for clamp interference on G00 moves. Fix the clear plane in CAM if the rapid path skims the fixture.
- 5Isolate the block with single blockStep through from the last known good line. When the symptom appears, you have the block. Check feed rate, cutter comp direction (G41 vs G42), and whether the move should be G01.
- 6Verify cutter compensation entryG41 and G42 need a lead-in move longer than the tool radius, or the controller alarms or cuts a gouge. Use a 2 mm minimum lead-in on a Ø6 mm cutter.
- 7Re-post from CAM and compareDiff the old and new programs. Look for changed feed, changed tool number, or a missing G43 height offset. Most post-processor faults show up as a missing line, not a wrong number.
- 8Log the fix and update the setup sheetRecord the offset, the feed change, or the CAM setting. If the same fault appears on the next run, the setup sheet was not the problem; the fixture or machine is.
Common questions about G codes
Is G code the same on every CNC machine?
The core set follows ISO 6983, so G00, G01, G02, G03, and the standard drilling cycles mean the same thing on most controllers. Fanuc, Siemens, Heidenhain, and Haas all accept them.
The differences sit in the edges: canned cycle details, high-speed machining modes, and probe routines vary by builder. A post-processor handles those, which is why we match the post to the exact machine model before running a new job.
Can I edit G code by hand after CAM posts it?
Yes, for small changes like a feed rate, a safe Z height, or a coolant command. Those edits are low risk and common at the machine.
Editing geometry by hand is where people get into trouble. Move one coordinate and the cutter comp lead-in, the arc endpoints, and the retract move may no longer line up. Re-post instead, then compare the two files.
Why does my machine alarm on G02 or G03?
The most common cause is an arc endpoint that does not sit on the radius defined by the I, J, K values. The controller checks this and rejects the block when the mismatch is beyond its tolerance.
The second cause is the wrong plane. G17 selects XY, G18 selects XZ, G19 selects YZ. An arc on the wrong plane will either alarm or cut in the wrong direction. Check the plane command before the arc block.
What is the difference between G codes and M codes?
G codes control how the machine moves and what state it holds. M codes control discrete actions: spindle on and off, tool change, coolant, program end. They work together in the same block sequence.
A simple rule: if it changes position or a modal condition, it is a G code. If it turns something on, off, or swaps it, it is an M code.
Do G codes affect surface finish?
Indirectly. Feed rate in the G01 block sets the chip load, which drives finish and tool life. Too high a feed on a finishing pass leaves visible scallops; too low rubs the edge and work-hardens stainless.
The controller's look-ahead and exact stop settings matter just as much. G61 forces an exact stop at corners, which improves accuracy but slows the cycle. For most finishing passes we use a small tolerance-based stop instead.
How do you keep G code programs consistent across prototype and production?
We store the proven program, the offsets, and the setup sheet together as one record. The prototype run and the 10,000-part run use the same code, the same tools, and the same workholding where possible.
When a change is needed, it goes back through CAM and gets re-posted, then re-proven on the first part. We inspect 100% of parts before shipment, so any drift from the original program shows up before it reaches the customer.
Need a program that holds tolerance on the first run?
Send your CAD files and we will return a quotation with a free DFM analysis within 12 hours. Uploads stay confidential, and an NDA is available on request.
12-hour quote100% inspection±0.005 mm toleranceNo minimum order quantity
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.











