GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Engineering Plastics, Machined

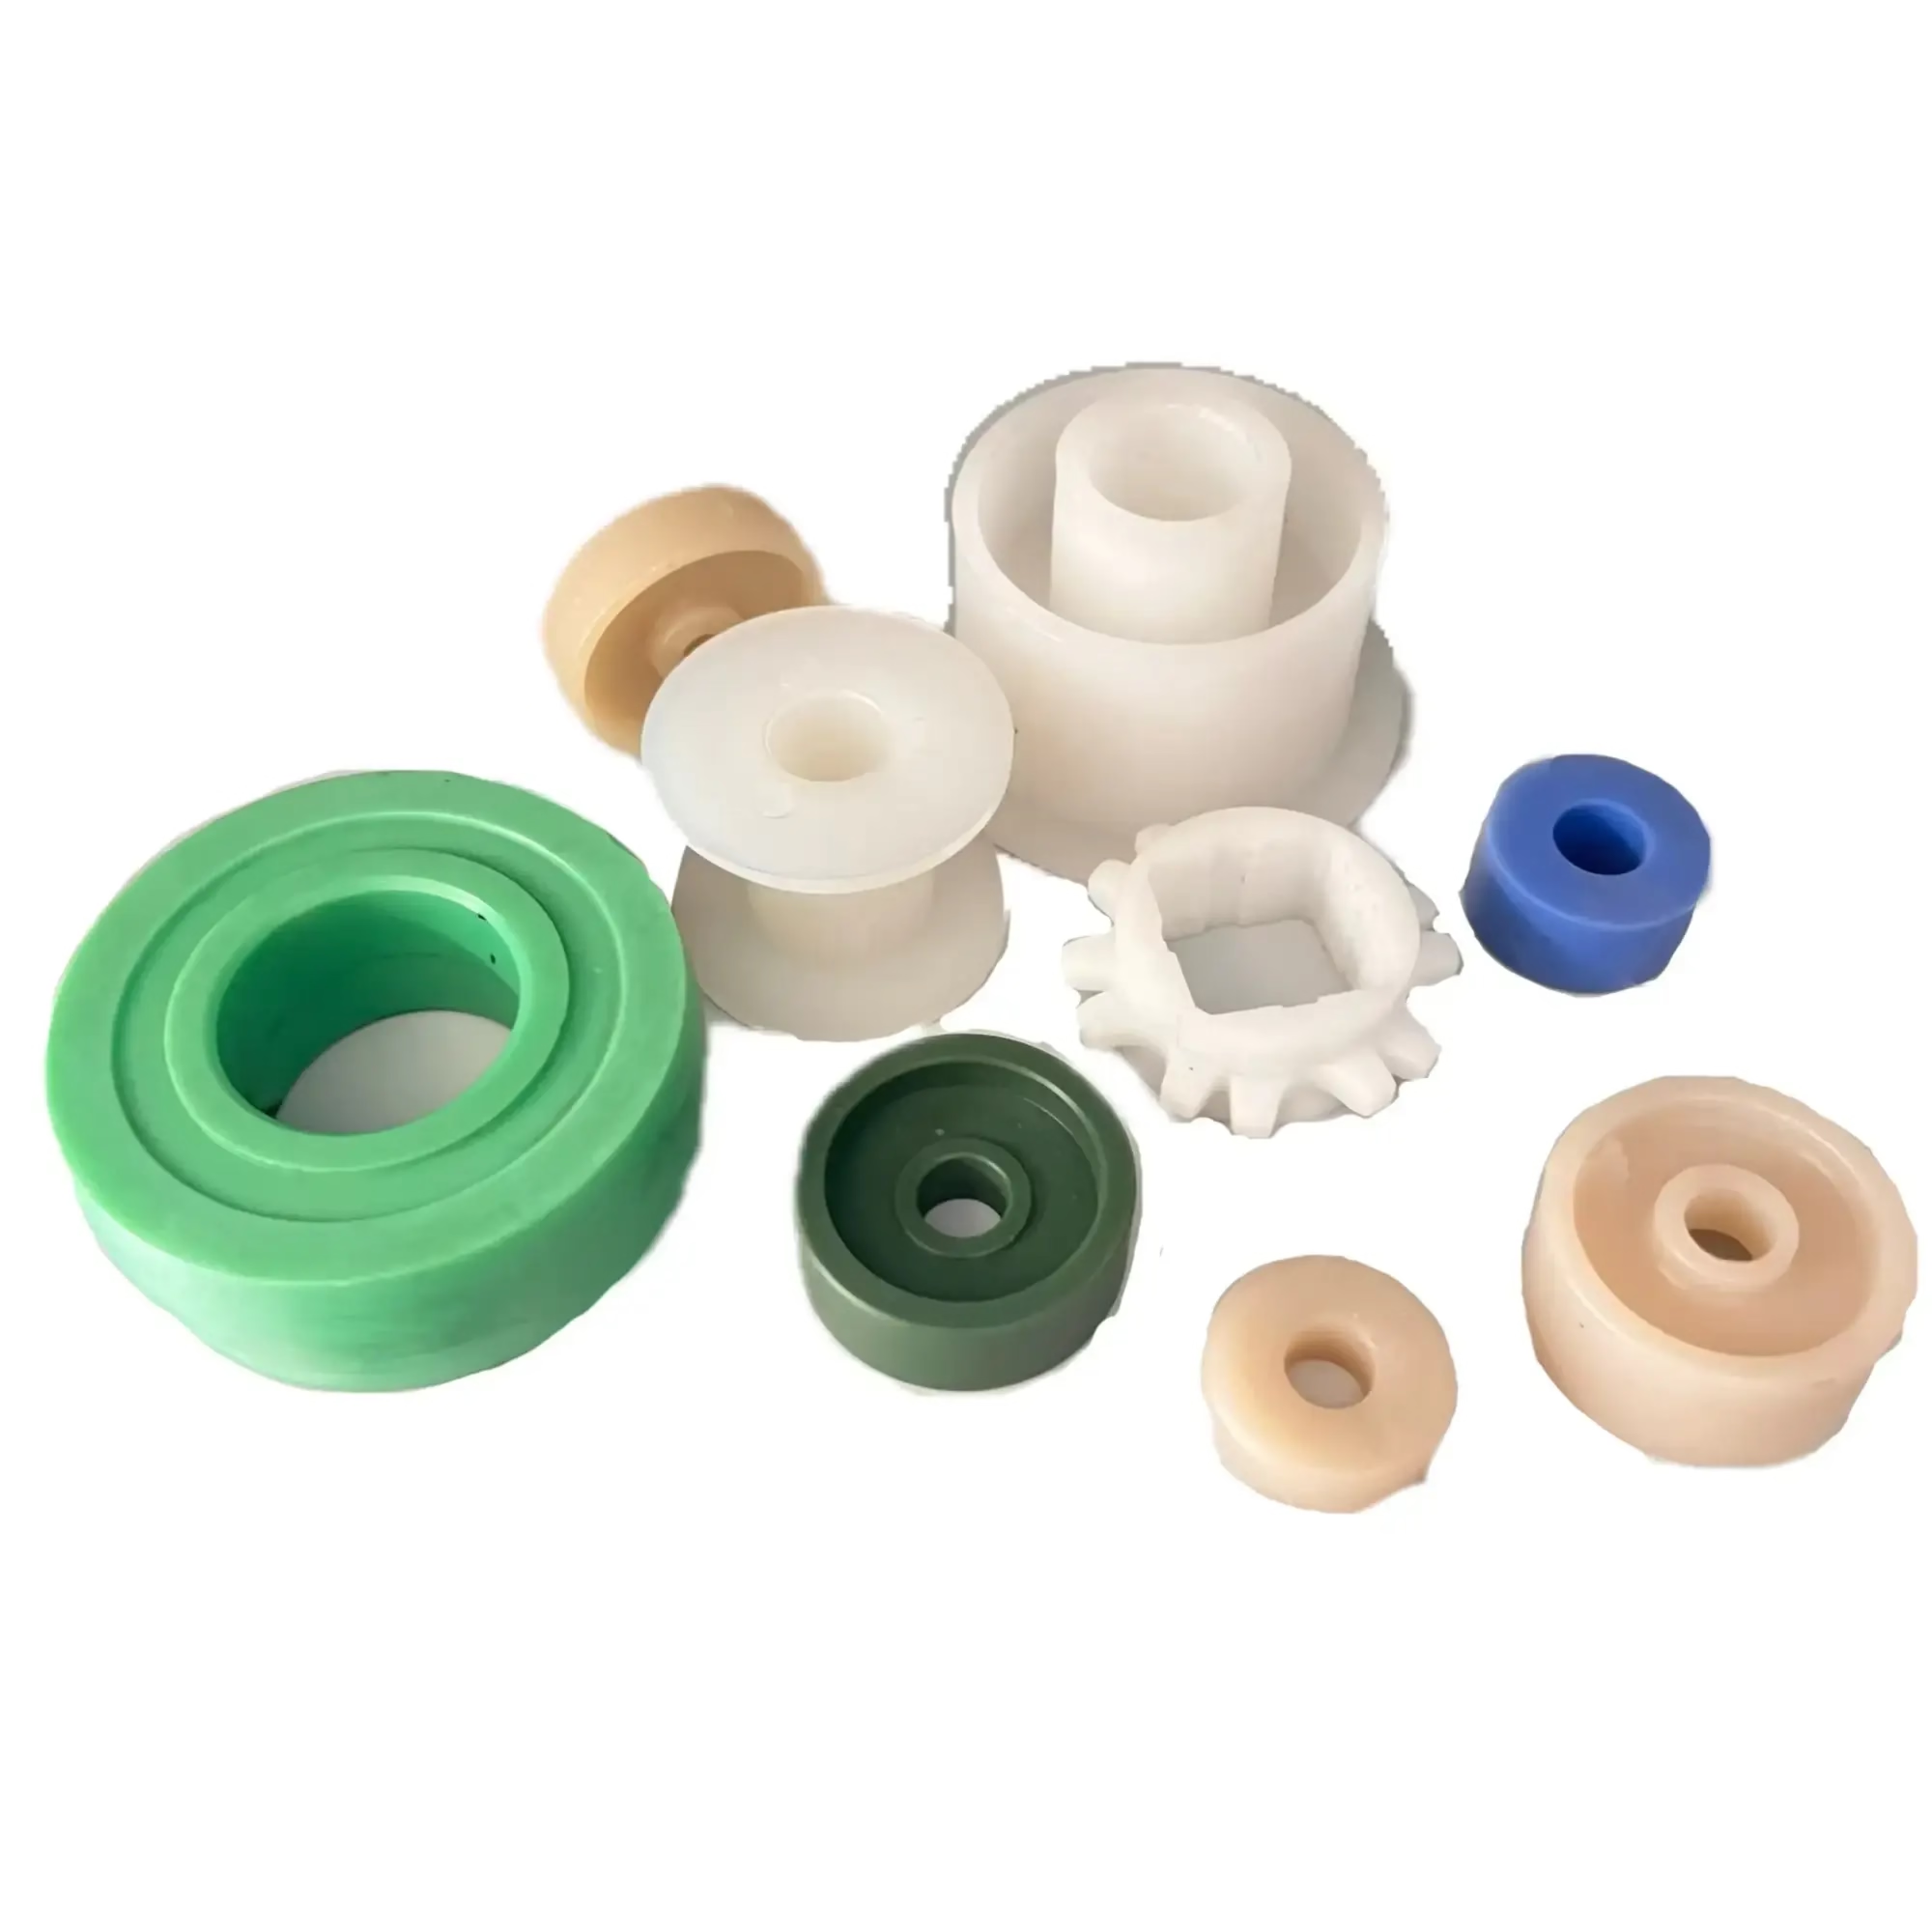
ABS POM Materials and Plastic CNC Parts

We machine ABS, PP, PC, PE and POM on the same 127-machine floor we use for aluminum and stainless. Send a drawing and we will tell you which of these five plastics actually holds your tolerance.

No minimum order quantity±0.005 mm12-hour quote and DFMRa 0.8–1.6 μm
pom-cnc-machining-scaled
127High-precision CNC machines
±0.005 mmAchievable tolerance on plastics
3–5 daysTypical shipping window
15 yearsMachining since 2011
Where plastic parts go wrong

Do you recognize any of these?

Most plastic machining problems are decided before the first cut. These four come up every week.

01

The part fits on the bench, not in the fixture

ABS and PE move after machining. A housing that measures on target at 9 a.m. can drift out of tolerance by afternoon if the stock was not stress-relieved or the finish cut removed too much material in one pass.

02

POM threads strip on the second assembly

POM cuts clean but has low surface energy, so adhesives and some thread forms fail under torque. The fix is a coarser thread, a metal insert, or a switch to a different plastic. We flag this at DFM, not after shipment.

03

Fine finish turns cloudy or hairy

Soft thermoplastics smear instead of cutting when the tool is dull or the spindle runs too slow. You get a Ra 3.2 μm surface and a burr line that no amount of tumbling removes.

04

Wall thickness changes and the part warps

PC and PP shrink unevenly around thick bosses and thin ribs. Ribs that look fine on the drawing pull the adjacent face out of flatness once the part cools.

Our approach

Match the plastic to the load, not to the catalog

Five materials cover most plastic turning and milling work. Each one has a job it does well and a job it does badly.

abs-cnc-machining
Material selection

ABS, POM, PP, PC and PE: what each one is for

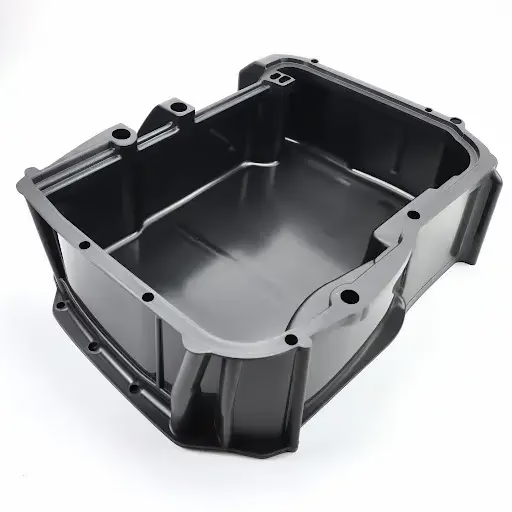
ABS is the general-purpose choice. It machines to a clean matte finish, takes paint and laser marking well, and costs less than PC or POM. Use it for enclosures, brackets, covers and prototype housings where stiffness matters more than chemical resistance.

POM is the closest thing to a machinable metal among thermoplastics. It holds ±0.005 mm on turned diameters, has low friction, and resists fuels and solvents. Gears, bushings, rollers and valve bodies are typical. It does not bond well, so plan on mechanical fastening.

  • 1
    PP and PEChemical resistance and toughness. Weak stiffness, so add ribs or increase wall.
  • 2
    PCImpact strength and clarity. Needs stress relief before finishing cuts.
  • 3
    POMDimensional stability and low friction. Best for moving parts.

Get Instant Quote

CNC Milling & Turning Services
Machining practice

How we hold tolerance in soft plastic

Plastic is not aluminum with a different color. It cuts at higher surface speed, takes a sharper edge, and pushes back against the tool. We run POM and PC on the same 5-axis and mill-turn centers used for metal, but with polished carbide, climb milling and lighter depth of cut.

For thin walls and long parts we rough, let the part normalize, then take the finish pass. On a 4,000 mm maximum processing envelope, that pause is often what separates a flat part from a banana. Coolant choice depends on the resin: some grades absorb moisture and grow, others crack under the wrong fluid.

  • 1
    Climb milling, sharp carbideReduces smearing and burrs on ABS and PE.
  • 2
    Rough, relax, finishLets internal stress release before the final pass.
  • 3
    Air blast on hygroscopic gradesKeeps PA and some PC stock from swelling mid-cut.

Selection table

Which plastic for which part

Use this as a starting point. Send the drawing and we will confirm against wall thickness and load.

MaterialBest forWatch out for
ABSEnclosures, covers, bracketsLow stiffness, absorbs some moisture
POMGears, bushings, rollersPoor bonding, hard to glue
PPChemical tanks, hinges, living partsVery low stiffness, warps easily
PCImpact guards, lenses, housingsStress cracking, needs annealing
PE (HDPE)Wear strips, insulators, food partsCreeps under sustained load
What we run

Turning and milling services for plastic parts

One shop for prototypes through 10,000+ part runs. Same machines, same inspection, same team.

01

CNC Turning

POM and ABS bushings, spacers, rollers and threaded inserts turned to ±0.005 mm on diameters.

02

CNC Milling

Housings, brackets and manifolds with pockets, slots and thin ribs. 3-axis through 5-axis.

03

5 Axis Machining

Complex plastic geometry in one setup. Fewer re-fixtures means fewer tolerance stacks on soft material.

04

Mill-Turn

Turned features plus cross-drilled holes on one machine. Good for POM valve bodies and fittings.

05

Rapid Prototyping

One-off ABS and PC prototypes to check fit before committing to a run of 10,000.

06

Surface Finishing

Bead blasting, tumbling, polishing and laser marking. Minimum character height 1.5 mm.

Scope

Plastic machining scope and inspection

ItemRangeNotes
Tolerance±0.005 mm (±0.0002 in)On turned diameters, stable resins
Surface finishRa 0.2–0.8 μm to Ra 1.6–3.2 μmDepends on resin and geometry
Maximum size4,000 mmLong PE and PP profiles
Order quantity1 to 10,000+No minimum order quantity
Inspection100% before shipmentReports on request
CertificationsISO 9001, IATF 16949, ISO 13485, ISO 27001Audited quality system
Why GreatLight

Reasons engineers keep sending plastic work here

15Y

Machining since 2011

Fifteen years on thermoplastics and metals. We know which resin fights which feature.

±0.005

Tolerance we hold

Millimeters on turned plastic diameters, measured and reported, not assumed.

12h

Quote and DFM in 12 hours

Material and geometry feedback comes back with the price, before you commit.

24h

Production start

Once the drawing and material are locked, cutting can begin within a day.

3

Wholly-owned plants

7,600 m² across Dongguan and Singapore. Your file stays inside our walls.

150

Technicians

Programmers and machinists who read drawings, not just job tickets.

127CNC machines
165-axis centers
99.99%Qualification rate
<2%Historical late-delivery risk
Where these parts go

Plastic parts by industry

Automotive-front-bumper-plastic-rapid-prototyping-jpg

Automotive and EV

PP and ABS brackets, clips and interior fixtures. IATF 16949 process control from first article.

  • PP / ABS
  • ±0.005 mm
  • IATF 16949
turning-copper-parts-3

Medical devices

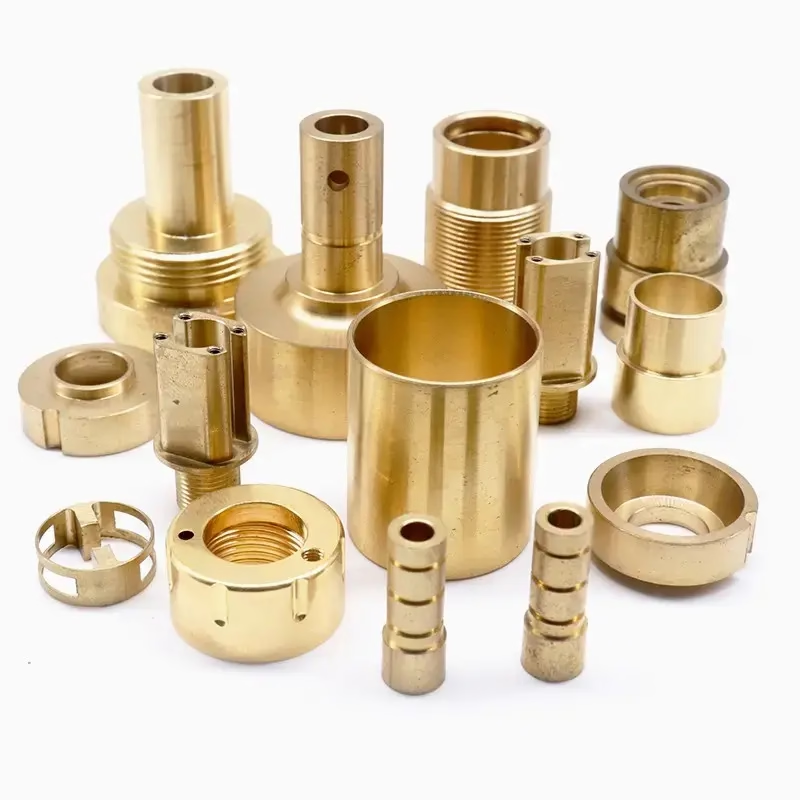
POM and PC housings, manifolds and instrument covers. Clean handling and 100% inspection.

  • POM / PC
  • 100% inspection
  • ISO 13485
custom-cnc-milling-services-2

Electronics

ABS and PC enclosures, bezels and insulating spacers with laser-marked labels.

  • ABS / PC
  • Laser marking
  • Ra 1.6 μm
custom-cnc-milling-services-23

Industrial machinery

POM gears, PE wear strips and PP guards. Runs held to the same drawing for repeat orders.

  • POM / PE / PP
  • 10,000+ runs
  • Repeatable
FAQs

Questions engineers ask about plastic CNC parts

How do I choose between ABS and POM?

ABS is for covers, enclosures and parts that stay still. It is cheaper, machines easily and takes paint.

POM is for parts that move or need to hold a tight dimension over time. If the part sees load, friction or solvent, start with POM.

Can you hit ±0.005 mm on every plastic?

No. That tolerance is realistic on POM and PC with stable geometry and controlled temperature.

PP and PE creep and warp. On those we usually work to looser bands and tell you so in the DFM report.

What is the maximum part size in plastic?

Up to 4,000 mm on the long travel machines, within a 4,000 × 400 × 150 mm envelope.

Large thin parts in PE and PP need extra support and a stress-relief step, which we plan into the routing.

Do you stress-relieve plastic before finish machining?

For PC, ABS and large PE parts, yes. We rough, let the part rest, then take the finish cut.

Skipping that step is the most common cause of a part that measures right in the shop and wrong at assembly.

Which plastics can be laser marked?

ABS, PC and POM mark cleanly with a contrasting result. PP and PE give a low-contrast mark.

Minimum character height is 1.5 mm. Below that we recommend an engraved or printed label instead.

Can plastic parts be threaded?

Yes. POM and ABS thread well with a coarse pitch and a relieved entry.

For parts that are assembled many times, we suggest a metal insert. Threads cut directly into PP or PE strip easily under torque.

What is the smallest order you accept?

One part. There is no minimum order quantity.

The same routing and inspection apply whether you order a single prototype or a run of 10,000+.

How do you protect the drawing and the design?

Uploads are handled as confidential and stay inside our three plants.

An NDA is available on request before you share files or CAD data.

Send your plastic part drawing

Tell us the resin, or send the drawing and let us recommend one. You get a price and a DFM note within 12 hours.

12-hour quote100% inspectionNo minimum order quantityNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC