
01
The drawing goes quiet for a week
You send a STEP file and hear nothing. No quote, no questions, no DFM notes. Two weeks later a price arrives with no explanation of what changed or which features drive the cost.
Send a drawing and get a quote plus DFM notes within 12 hours. We machine prototypes and production runs, handle finishing, and inspect every part before it ships.

Four failures we see on incoming RFQs every week.
You send a STEP file and hear nothing. No quote, no questions, no DFM notes. Two weeks later a price arrives with no explanation of what changed or which features drive the cost.
A callout of ±0.01 mm on a 300 mm thin-wall plate will scrap parts at any shop. Nobody flags it before cutting metal, so the first article fails and the schedule slips.
The machine shop ships bare parts. Anodizing, plating and heat treating go to separate vendors with their own queues, and no one owns the final surface result or the rework.
You ask for a status update and get a vague answer. Meanwhile your assembly line has a start date and no confirmed ship date, so you build buffer stock you did not budget for.
Three steps from file to finished part, with a named engineer on the account.

Every upload goes to a process engineer, not a sales queue. Within 12 hours you get a price and a short list of DFM notes: features that will chatter, walls that are too thin for the material, tolerances that cost more than they are worth.
You decide what to change. If a corner radius can open up from R0.5 to R2, we say so and show what it saves. If a datum needs to move, we explain why before the first cut, not after the first reject.

Production can start within 24 hours of a released order. We run 16 simultaneous 5-axis centers, 12 four-axis mills, 27 three-axis machines and 16 mill-turn centers across three plants. Maximum processing size is 4,000 mm, so long frames and housings do not need to be split into bolted sections.
Finishing is scheduled with the machining, not after it. Anodizing, plating, powder coating, bead blasting and laser marking all come back through our own final inspection. Parts ship in 3–5 days on typical jobs.
Match the geometry and quantity to the right route before you commit.
| Part situation | Recommended route | Why |
|---|---|---|
| One-off bracket, simple 3-axis geometry | 3-axis milling | Fastest setup, lowest cost at quantity one |
| Impeller or contoured housing | 5-axis simultaneous | One setup, no repositioning error |
| Shaft with milled flats | Mill-turn center | Turning and milling in a single cycle |
| Thin-wall enclosure, 500+ parts | 4-axis with fixture | Repeatable clamping, shorter cycle time |
| Long frame up to 4,000 mm | Large-travel 5-axis | No splitting or bolted joints |
| Prototype before tooling | Rapid prototyping | Validate fit before committing to a run |
Machining is only part of it. These are the routes we quote most often.
Simultaneous 5-axis work for contoured surfaces, deep pockets and parts that would need three setups on a 3-axis machine.
Milling, turning and mill-turn centers cover prismatic parts, shafts, bushings and threaded components in one order.
Machined prototypes in the final material, so fit and function testing reflects the production part, not a stand-in.
Brackets, panels and enclosures when the geometry is better formed than cut, including light-gauge aluminum.
Anodizing, electroless nickel, zinc, silver and gold plating, powder coating, black oxide, blasting and laser marking.
For higher volumes where a casting plus finish machining beats cutting the whole part from solid.
If your material is not listed, ask. Most engineering alloys and plastics are workable.
| Category | Typical grades | Notes |
|---|---|---|
| Aluminum | 6061-T6, 2024, 5052, 6063, 6082, 7075, ADC12 | Anodizing and hardcoat available |
| Stainless steel | 303, 304, 316L, 420, 440C, 17-4PH | Passivation on request |
| Steel | 1018, 1045, 4130, 4140, 4340, A36 | Heat treating coordinated in house |
| Titanium & special | TA1, TA2, TC4 (Ti-6Al-4V), Inconel | Slow feeds, tooling planned per part |
| Copper & brass | C101, C110, C36000, beryllium copper | Conductive and RF housings |
| Plastics | POM, PEEK, PA, PC, ABS, PMMA, carbon fibre | Carbon fibre needs per-part feed testing |
Fifteen years, three plants, and a process built around first-article approval.
Fifteen years of production work, 150 technicians across three wholly-owned plants in Dongguan and Singapore.
That is ±0.0002 in. Achievable on the right geometry and material, and we tell you when it is not.
Quotation plus free DFM analysis within 12 hours of a complete upload.
Released orders can enter the schedule within one working day.
Measured across shipped production. Every part inspected, not sampled.
Below two percent on past orders. We quote dates we can hold.

ISO 13485:2016 process control, full traceability and Ra 0.8–1.6 μm internal surfaces.
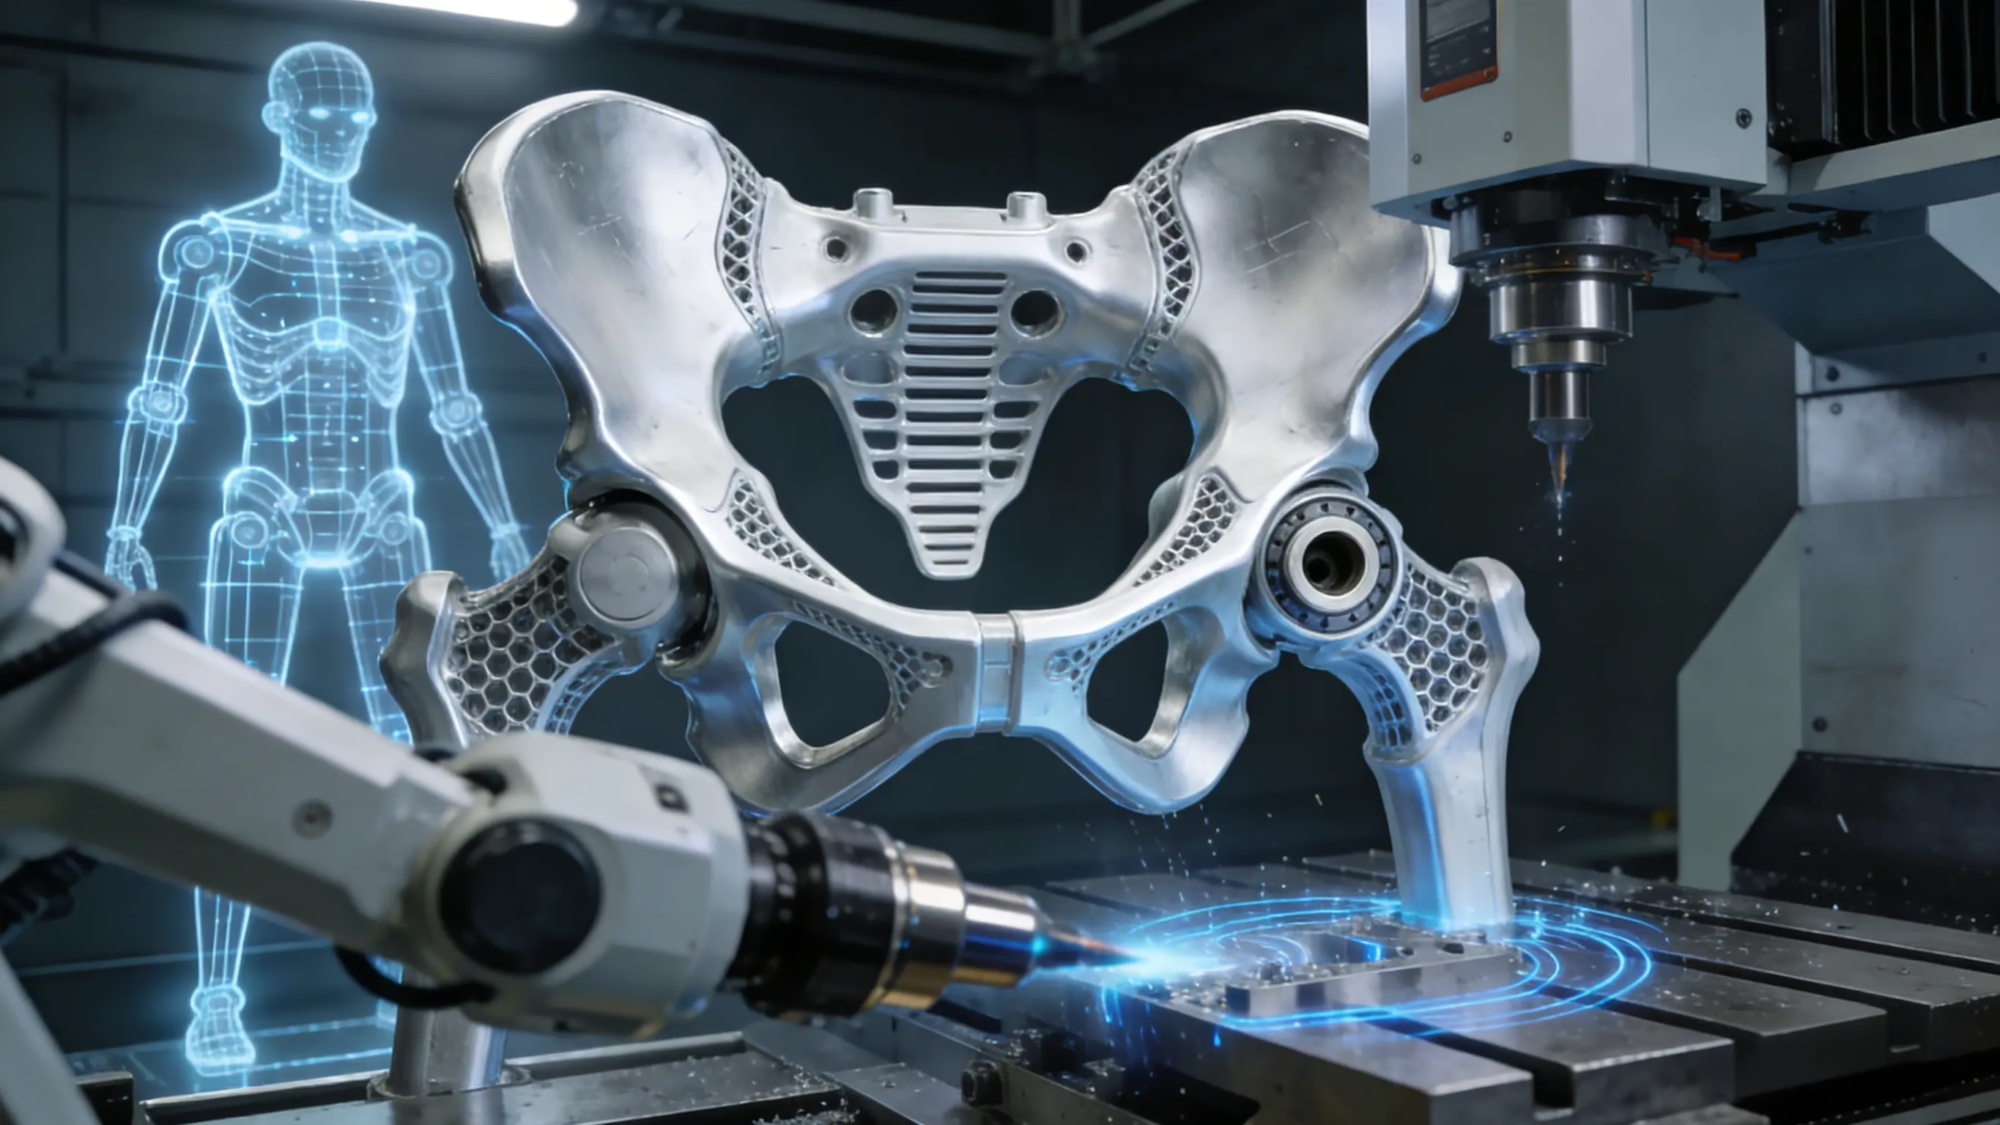
Simultaneous 5-axis work on thin ribs and contoured joints that must hold alignment after assembly.

IATF 16949:2016 control on turned and milled parts, with first-article approval before the run.
Send the 3D model and the 2D drawing together, and say which dimensions are functional. The quote comes back with DFM notes in 12 hours.
Mark the critical tolerances rather than applying one tight tolerance across the whole print. That single change usually cuts cost more than any negotiation.
A single sample is charged as a one-off. Batch production is different: we provide a free sample for you to check before mass production starts.
So if you are validating a design, expect to pay for the first piece. If you are releasing a run, the check piece does not add cost.
Quotation and DFM analysis within 12 hours. Production can start within 24 hours of a released order.
Parts ship in 3–5 days on typical jobs. Historical late-delivery probability is below 2 percent.
Yes. We regularly machine POM, PEEK, PA, PC, ABS, PMMA and PP, along with PVC and PTFE.
Carbon-fibre composites are workable but need special tooling, and each new part needs a feed and speed trial before the run.
We coordinate them as part of the order. Anodizing in clear, colour, hardcoat and conductive, plus electroless nickel, zinc, silver and gold plating, powder coating and black oxide.
Finished parts come back through our own final inspection, so one team owns the surface result.
There is no minimum. We run one prototype or a 10,000+ part run on the same process.
For one-offs, expect a higher unit price because programming and setup do not scale down.
Uploads are secure and confidential. An NDA is available on request and we can sign it before any file moves.
We hold ISO 27001:2022 for information security management.
No, and be careful with any shop that says yes without asking about geometry. That tolerance is achievable on rigid parts with good datums.
On thin walls, long unsupported sections or soft plastics, we will tell you the realistic tolerance and what fixturing it would take to get closer.
Upload your files and get a quotation, DFM notes and a realistic tolerance review within 12 hours.
12-hour quote100% inspectionNo MOQNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.