GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

CNC Turning & Milling

Lathe Machining Milling

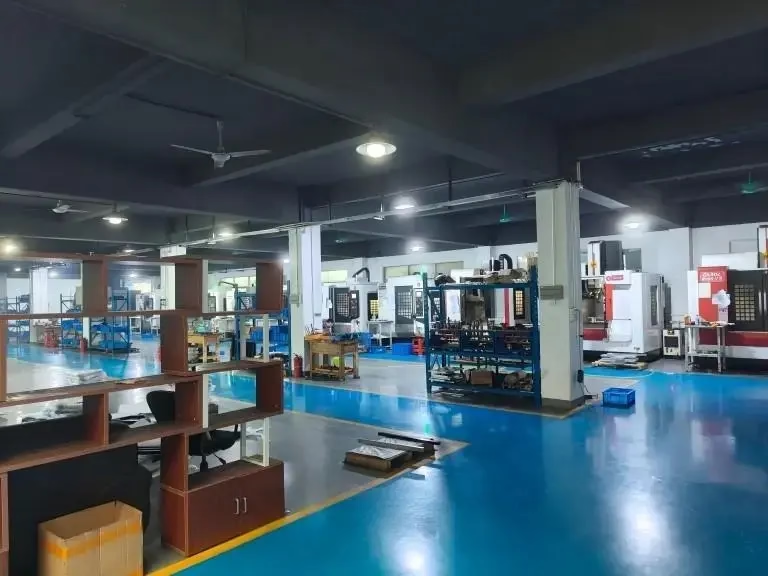
We turn and mill the same part on one machine. One setup, one datum, tighter concentricity. 127 CNC machines in Dongguan, 16 of them mill-turn centers, holding ±0.005 mm on metal and plastic parts up to 4,000 mm.

±0.005 mmRa 0.8–1.6 μm4,000 mm max16 mill-turn centersNo MOQ
CNC Milling & Turning Services
127High-precision CNC machines
16Mill-turn centers
±0.005 mmAchievable tolerance
3–5 daysTypical shipping window
Shop-floor problems

Where turned-and-milled work goes wrong

Most failures on these parts trace back to one of four things.

01

Do you re-chuck the part and lose concentricity?

Move a shaft from the turning center to the mill and the second setup adds its own runout. Bore and OD drift apart. A 0.02 mm eccentricity turns into a rejected assembly, and the fix usually costs more than the part.

02

Does the quote change after the drawing reaches the floor?

Cheap initial numbers often hide extra setups, soft jaws, custom fixtures, or a second inspection pass. The invoice arrives with line items you never approved. Ask what is included before the chips fly.

03

Are cross-drilled holes breaking into the bore?

A milled flat or cross hole that intersects a turned bore leaves a burr you cannot reach with a deburring tool. It shows up as a leak path or a fatigue crack six months into service. Tool exit direction decides whether this happens.

04

Is the finish inconsistent from part to part?

Tool wear, coolant pressure, and depth of cut all move the surface finish. Without in-process checks, part 1 and part 500 can differ by two Ra steps. That matters on sealing faces and bearing journals.

One setup, two operations

How we hold concentricity on turned-and-milled parts

The answer is usually to stop moving the part.

custom-cnc-milling-services-2
Mill-turn capability

Turn and mill in the same spindle

A mill-turn center keeps the part in one chuck while a live tool does the milling. The datum never changes. Concentricity between a turned OD and a milled bore is set by the machine geometry, not by how carefully an operator re-indicates the second setup.

We run 16 mill-turn centers with up to 5 simultaneous axes and a Ø400 mm rotary table. That covers cross-drilled holes, milled flats, slots, and eccentric features on the same part. For a hydraulic manifold or a motor shaft, this removes the tolerance stack that comes from two separate machines.

  • 1
    One datumNo re-indicating between turning and milling operations.
  • 2
    Live toolingCross holes, flats, and slots cut without a second fixture.
  • 3
    Bar feed to 4,000 mmLong shafts and housings stay on one machine.
custom-cnc-milling-services-23
Process control

Deciding the operation sequence

Not every part belongs on a mill-turn center. If a feature needs to be ground after hardening, or if the part is a thin-wall aluminum housing that will deflect under chuck pressure, we split the work across a 3-axis mill and a lathe with soft jaws. The sequence is chosen by what the tolerance stack allows, not by machine availability.

For parts that do stay on one machine, we program the milling passes before the finishing turn whenever possible. That way a cross hole or flat does not interrupt the surface finish on a sealing diameter. It also keeps the tool exit burr on a face you can reach later.

  • 1
    Sequence by toleranceFeatures that stack are cut in one setup.
  • 2
    Soft jaws for thin wallsChuck pressure is controlled on bores and housings.
  • 3
    Deburring planned inTool exit direction chosen so burrs stay accessible.
Selection guide

Mill-turn or separate operations?

Part featureBest processWhy
Shaft with cross holesMill-turn centerConcentricity held in one chuck
Housing with large face mill3-axis mill + latheFace area exceeds live tool reach
Thin-wall aluminum boreLathe, soft jawsChuck pressure controlled
Hardened bearing journalTurn, harden, grindGrinding sets final size
Long shaft over 1,000 mmMill-turn, bar feedNo re-chuck for straightness
Plastic bushingLathe, sharp toolingLow cutting force, no melt
What we run

Turning and milling services

Six operations that cover most turned-and-milled part families.

01

CNC turning

Shafts, bushings, fittings, and housings turned to ±0.005 mm. Bar feed up to Ø80 mm, chuck work to Ø400 mm. Live tooling for cross holes and flats.

02

3-axis milling

Prismatic parts, plates, and brackets. Travels of 750 × 1,150 × 550 mm. Good for parts with one dominant face and no undercut features.

03

4-axis milling

Parts that need features on four sides without re-fixturing. 12 machines available. Cuts setup count and holds angular position between faces.

04

5-axis milling

16 simultaneous 5-axis centers for contoured surfaces, impellers, and complex geometry. Reduces the number of fixtures and the tolerance stack they add.

05

Mill-turn centers

Turning and milling in one spindle. Best for parts where a turned diameter and a milled feature share a tolerance. Ø400 mm rotary table.

06

Surface finishing

Anodizing, plating, powder coating, bead blasting, and polishing. Laser marking available from 1.5 mm character height.

Scope and limits

Machine capacity and part range

ItemRangeNotes
Maximum part size4,000 mmLong shafts on mill-turn centers
Large travel4,000 × 400 × 150 mmLong, narrow parts
Medium travel750 × 1,150 × 550 mmPlates and housings
Compact travel500 × 500 × 450 mmSmall prismatic parts
Tolerance±0.005 mm±0.0002 in on qualified features
Surface finishRa 0.2–3.2 μmFine to as-machined
Minimum order1 partPrototype to 10,000+ runs
Quote turnaround12 hoursIncludes free DFM analysis
Why GreatLight

What you get on the floor

15Y

Machining since 2011

15 years turning and milling production parts. 3 wholly-owned plants, 7,600 m² of floor space, 150 technicians.

±0.005

Tolerance held in production

Not just a first-article number. In-process monitoring keeps the same tolerance on part 1 and part 5,000. Reports available on request.

12H

Quote in 12 hours

Send the drawing and get a quote plus free DFM analysis within 12 hours. Production can start within 24 hours of approval.

ISO

Four certifications

ISO 9001:2015, IATF 16949:2016, ISO 13485:2016, and ISO 27001:2022. Covers automotive, medical device, and data security requirements.

30+

Material range

Aluminum 6061, 7075, and 2024. Stainless 303, 304, 316L, and 17-4PH. Steel 1018, 4140, and 4340. Titanium, Inconel, brass, copper, and engineering plastics.

0

No minimum order

One prototype or 10,000 parts. Same process control either way. Uploads stay confidential and an NDA is available on request.

Industry results

What these parts have to meet

custom-cnc-milling-services-241

Automotive & EV

Motor shafts and transmission components. IATF 16949:2016 process control, ±0.005 mm on bearing journals, in-process checks on every run.

  • IATF 16949:2016
  • ±0.005 mm
  • 100% inspection
custom-cnc-milling-services-261

Medical devices

Surgical instrument bodies and implant housings. ISO 13485:2016, Ra 0.2–0.8 μm on sealing faces, full material traceability on request.

  • ISO 13485:2016
  • Ra 0.2–0.8 μm
  • Traceable
custom-cnc-milling-services-27

Aerospace

Actuator housings and structural fittings. Titanium and 17-4PH turned and milled in one setup, first article inspection on request.

  • Ti-6Al-4V
  • 17-4PH
  • FAI available
custom-cnc-milling-services-31

Robotics & automation

Joint housings and gearbox components. Mill-turn centers hold bore-to-OD concentricity, so gear mesh and bearing fit stay within spec.

  • Mill-turn
  • Concentric bores
  • ±0.005 mm
FAQs

Questions engineers ask before ordering

When should a part be turned and milled on one machine?

When a milled feature and a turned diameter share a tight tolerance. Cross holes relative to a bore, a flat relative to an OD, or an eccentric feature on a shaft all benefit from one setup.

If the part has no such relationship and the features are simple, separate machines are usually faster and cheaper.

What is the largest part you can turn and mill?

Up to 4,000 mm maximum processing size. Long narrow parts run on the 4,000 × 400 × 150 mm travel machines. Larger prismatic parts go on the 750 × 1,150 × 550 mm or 600 × 600 × 600 mm mills.

If a part exceeds these envelopes, we will tell you at quote time rather than after the order.

How do you control burrs where a cross hole meets a bore?

We choose the tool exit direction so the burr lands on an accessible face, then deburr by hand or with a controlled tool path. This is planned at programming, not fixed at inspection.

For hydraulic and pneumatic parts, we can add a bore scope check or a flow test if the drawing calls for it.

Which materials do you machine most often?

Aluminum 6061-T6 and 7075, stainless 303 and 316L, and steel 1018 and 4140. Titanium TC4 (Ti-6Al-4V) and 17-4PH are common for aerospace and medical parts.

Engineering plastics such as POM, PEEK, and PC run on the lathes with sharp tooling and controlled feed to avoid melting.

What surface finishes can you hold?

Turned and milled surfaces range from Ra 0.2–0.8 μm on fine finishes to Ra 1.6–3.2 μm as-machined. The achievable value depends on material, feature geometry, and whether the surface is turned or milled.

Sealing faces and bearing journals usually specify Ra 0.8–1.6 μm. We can confirm what a specific feature can hold during DFM review.

Do you inspect every part?

Yes. 100% inspection before shipment, with raw material checks, in-process monitoring, and a final inspection pass. Inspection reports are available on request.

First article inspection is available on request for orders over 50 units or 5,000 USD.

How fast can you quote and ship?

Quotation and free DFM analysis within 12 hours. Production can start within 24 hours of approval. Parts typically ship in 3–5 days.

Lead time depends on material availability and feature complexity. We give a specific window at quote time.

Can you work from a STEP file without a drawing?

Yes, but a drawing helps. STEP files define geometry; they do not define datum callouts, surface finish requirements, or which dimensions are critical.

If you send only a model, we will flag the tolerances we plan to hold and ask you to confirm before cutting metal.

Send your drawing and get a quote in 12 hours

Upload a STEP file or PDF drawing. We reply with a quote, a DFM analysis, and a realistic lead time. No minimum order.

12-hour quoteFree DFM analysis100% inspectionNo MOQNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC