GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Sheet Metal Fabrication

Metal Bending

Custom metal bending for brackets, enclosures and chassis in aluminum, stainless and steel. We hold bend angles to ±0.5° and cut features to ±0.005 mm, with DFM feedback inside 12 hours.

Bends up to 4,000 mm±0.5° angle controlPrototype to 10,000+ parts100% inspectionISO 9001 / IATF 1694912-hour DFM response
custom-sheet-metal-fabrication-services1
15 yearsBending and CNC experience
7,600 m²Across 3 wholly-owned plants
4,000 mmMaximum bend length
±0.005 mmCut-to-bend datum tolerance
Common problems

Where bent parts go wrong

Most bending failures start before the press brake. Here is what we see on incoming work.

01

Angles drift after the first article

The first piece measures clean. By piece 200 the flange reads 1.5° open, and the weld fixture no longer closes. Springback changes with each coil of material, so a setup that was never dialed in drifts quietly until assembly catches it. We verify angle at the brake, not at the end of the line.

02

Holes stretch near the bend line

A hole placed 2 mm from the inside bend radius pulls oval when the flange forms. Bolts no longer sit flush and the mating bracket rocks. This is a design issue, not a machine issue, and it shows up in the DFM review before any metal is cut.

03

Bend lines land on the wrong datum

Flat patterns are laid out from one edge, but the laser cuts from another. Cumulative error walks the bend line down the part. The bracket fits the first assembly and misses the tenth. One shared datum for laser and brake removes the argument.

04

Tooling marks on visible faces

V-die contact leaves bright lines across a powder-coated panel. On a painted enclosure that is scrap, not rework. Soft tooling pads and a planned bend sequence keep the A-surface clean on the first pass.

How we bend

Forming built around the flat pattern

Bend allowance, tooling choice and inspection all trace back to one layout file.

aluminum-alloy-industrial-control-chassis-sheet-metal-processing
Process control

One datum from laser to brake

We build the flat pattern from your 3D model, then release the same layout file to both the laser and the press brake. Bend allowance and K-factor follow the material and thickness in the drawing, not a default table. For 6061-T6 at 2 mm, that means a different deduction than 304 stainless at the same gauge.

Operators set the angle against a test coupon cut from the same sheet, then check the first article on a CMM. Any angle correction is logged, so a repeat order runs from the same numbers instead of starting over.

  • 1
    Material-specific K-factorAluminum, stainless and steel each get their own bend allowance.
  • 2
    First-article CMM checkAngle and flange length verified before the run continues.
  • 3
    Repeatable setup sheetsTooling, tonnage and backgauge stored for the next run.

Get Instant Quote

cnc-machining-metal
Part design

What bends cleanly, and what does not

A flange shorter than four times the material thickness is hard to form without the punch bottoming out. Holes closer than 2.5 times the thickness to the bend line will distort. Deep boxes with four flanges on the same side need relief cuts or a different sequence, and sometimes a welded box is the cheaper answer.

We flag those cases in the DFM report rather than forming them and hoping. If a design can be adjusted by 1 mm or one bend moved, the part usually gets simpler and the cost drops with it.

  • 1
    Minimum flangeRoughly 4× thickness, or the punch needs a relief.
  • 2
    Edge distanceKeep holes at least 2.5× thickness from the bend line.
  • 3
    Bend reliefAdd corner reliefs on boxes with adjacent flanges.

Talk to an Engineer

Selection guide

Material and thickness, by application

A starting point for common bent parts. Other grades are available on request.

MaterialTypical thicknessGood forWatch out for
6061-T6 aluminum1.5–4 mmBrackets, panels, chassisCracks on tight inside radii
5052 aluminum1–3 mmEnclosures needing formingLower yield strength than 6061
304 stainless0.8–3 mmFood, medical, washdown partsHigh springback, more tonnage
316L stainless1–3 mmChemical and marine exposureCost and work-hardening
Cold-rolled steel 10181–6 mmGeneral structural bracketsNeeds coating to resist rust
Galvanized steel1–3 mmOutdoor housings, cabinetsZinc coating can flake at bends
What we run

Bending plus the operations around it

One supplier for the flat pattern, the form and the finish.

01

Press brake forming

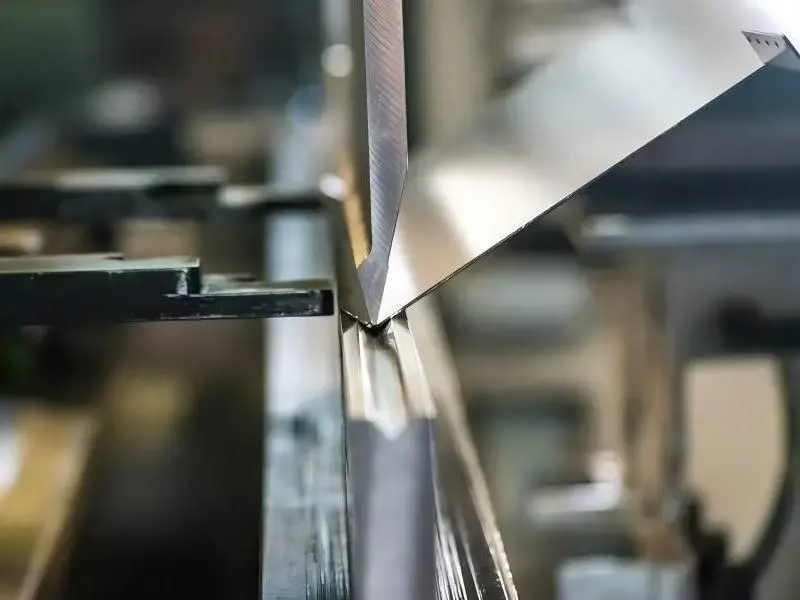
V-die and air bending on material up to 4,000 mm long. Angle control to ±0.5° on production runs.

02

Laser cutting

Flat blanks cut from the same layout file that drives the brake, so bend lines land where the drawing says.

03

CNC machining of bent parts

Post-form milling and drilling on 127 CNC machines, including 16 simultaneous 5-axis centers.

04

Welding and assembly

Spot, MIG and TIG joining for boxes and frames, with fixtures that hold the formed geometry.

05

Surface finishing

Anodizing, powder coating, plating, bead blasting and laser marking, applied after forming.

06

Inspection and reporting

100% inspection before shipment with raw material, in-process and final checks. Reports on request.

Capability range

Bending capacity at a glance

ParameterRangeNotes
Maximum bend length4,000 mmLarger parts quoted case by case
Bend angle tolerance±0.5°Verified on first article
Cut feature tolerance±0.005 mmDatum shared with the brake
Material thickness0.8–6 mmDepends on grade and radius
Order quantity1 to 10,000+No minimum order quantity
Quote turnaroundWithin 12 hoursIncludes free DFM analysis
Why GreatLight

Numbers behind the service

15Y

Forming since 2011

Three wholly-owned plants and 150 technicians covering bending, machining, finishing and assembly under one quality system.

±0.005

mm on cut features

The same tolerance we hold on CNC work applies to the blank that feeds the brake. Bent parts start accurate.

127

CNC machines on site

16 simultaneous 5-axis centers and 16 mill-turn centers handle post-form machining without sending parts out.

99.99%

Qualification rate

Every lot passes raw material check, in-process monitoring and final inspection before it ships.

3–5 days

Typical shipment window

Production can start within 24 hours of a released order. Historical late-delivery probability is under 2%.

4

Quality certifications

ISO 9001:2015, IATF 16949:2016, ISO 13485:2016 and ISO 27001:2022 cover the full process.

7,600 m²Manufacturing space
150Technicians
12 hQuote and DFM response
100%Inspection before shipment
Applications

What bent parts have to survive

large-die-cast-metal-part-back-19

Industrial control chassis

Folded aluminum housing with machined faces for panel cutouts.

  • 6061-T6
  • ±0.5° angles
  • 100% inspected
large-die-cast-metal-part-back-5

Automotive mounting bracket

Multi-flange bracket formed from 3 mm steel, then zinc plated.

  • IATF 16949
  • 3 mm steel
  • No minimum order quantity
metal-3d-printing-1801

Medical equipment enclosure

Stainless cover with a clean A-surface and bead-blasted finish.

  • 304 stainless
  • ISO 13485
  • Tooling marks avoided
FAQs

Questions we get before a bending order

What file formats do you need for a quote?

A STEP or IGES model plus a 2D drawing works best. The 3D file gives us the formed shape and the drawing carries tolerances, material and finish. DXF flat patterns are fine if you already have them.

If you only have a PDF, send it. We will rebuild the geometry and flag anything that cannot be formed as drawn.

How tight can you hold a bend angle?

We hold ±0.5° on production runs and verify it on the first article with a CMM. Tighter angles are possible on short flanges with the right tooling, but they need a conversation before quoting.

Springback is the real limit, not the machine. Aluminum and stainless behave differently, so the setup is built around the grade you specify.

What is the minimum order quantity?

There is none. A single prototype bracket and a 10,000-piece run go through the same process, just with different setup time.

For one-off parts we may hand-form rather than build a dedicated setup. That keeps the cost sane without changing the geometry.

Can you bend parts longer than 4,000 mm?

4,000 mm is our standard maximum bend length. Longer parts are quoted case by case and usually split into welded sections.

If a long part is mostly straight with a few short flanges, segmenting it often costs less than finding a longer brake.

Do you machine after forming?

Yes. Post-form milling, drilling and tapping run on our CNC machines, including 5-axis centers for angled holes on formed faces.

Machining after bending is usually the right call when a hole has to sit on a formed surface. Bending after machining risks distorting a finished bore.

How do you handle visible surfaces?

Tell us which face is the A-surface in the drawing. We choose tooling and bend sequence to keep die marks off it, and use protective film where needed.

On powder-coated panels, a mark that would be invisible on bare steel becomes scrap. It is cheaper to plan the sequence than to strip and recoat.

What inspection do bent parts get?

Raw material certificates on arrival, in-process checks at the brake, and a final inspection before shipment. Every lot is inspected at 100%.

Dimensional reports, first-article inspection reports and material certs are available on request. Say so at the quote stage so we build them into the plan.

How is my design kept confidential?

Uploads are secure and confidential. We are certified to ISO 27001:2022 for information security.

An NDA is available on request before you send files. If your drawings are controlled, tell us and we will route them accordingly.

Send your bending project

Upload a STEP file or a drawing and get a quote with DFM notes within 12 hours. Prototype or production run, same process.

Quote and DFM within 12 hoursNo minimum order quantity100% inspection before shipmentNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC