
What Are CNC Vertical Milling Machines?
A vertical mill holds the spinning tool above the table and drives it down into the work. This page explains the axis layout, the real travel and tolerance limits, and how to tell whether a part belongs on a vertical mill, a lathe, or a 5-axis center. Written for engineers and buyers who need to read a quote and know what they are paying for.
Key takeaways
How a vertical mill actually cuts metal
A CNC vertical milling machine holds the cutting tool in a spindle that points straight down at the worktable. The tool spins at a programmed speed while the table, or the column, moves the workpiece underneath it in X, Y and Z. The result is a shape cut by the side and the end of a rotating multi-tooth cutter, not by a single-point tool as on a lathe.
The cutting action is intermittent. Each tooth enters the material, takes a chip, and leaves. That interrupt is why rigidity matters more than raw spindle power. If the column or the tool holder deflects under load, the cutter rubs instead of shearing and the surface finish drops.
On a typical part, the operator clamps the blank to the table or into a vise, sets the work offset, and lets the program run. The controller reads G-code, positions the tool, and changes tools from the magazine between operations. That single setup logic is what makes vertical mills cheap to program for one-off work.
Materials behave differently under the same cutter. Aluminium 6061 tolerates high spindle speeds and heavy feed. Stainless 316 work-hardens if the cutter dwells, so we keep the feed per tooth up and avoid rubbing passes. Titanium Ti-6Al-4V moves heat into the tool, so we slow the surface speed and flood the cut with coolant.
- 1Cutting motionInterrupted by nature; every tooth makes a separate chip.
- 2RigidityTool deflection shows up as chatter, taper, or a rough floor finish.
- 3CoolantMostly evacuation and heat control, not just lubrication.
Axes, spindle orientation and what each one buys you
A basic vertical mill has three linear axes. X moves the table left and right, Y moves it in and out, Z moves the spindle up and down. A 3-axis machine can cut any shape it can reach from above, so pockets, slots, steps and drilled holes are all routine.
Add a fourth axis and the part can rotate while it is being cut. On a vertical mill this is normally an indexer or a rotary table, listed in our shop as a Ø400 mm rotary table. The part rotates, the tool works on a new face, and you avoid a second setup.
A fifth axis tilts the tool or the table. That lets a short, stiff cutter reach a deep wall at an angle instead of using a long tool that would chatter. Impellers, turbine blades and contoured mold surfaces are the usual justification.
The trade is not free. Every added axis introduces setup time, programming time, and a new stack of geometric error. If the part is a flat plate with a few holes, a 3-axis machine will hold tighter numbers and cost less.
- 13-axisBest tolerance per dollar on prismatic parts.
- 24-axisAdds index positions around one horizontal axis.
- 35-axisReaches undercuts and steep walls without re-fixturing.
Spindle, tool holder and the finish you can hold
The spindle is a rotating shaft with a tapered socket at the bottom. It sets the top end of your cutting speed. Too slow and the tool rubs; too fast and the edge breaks down through heat. The number we care about in quoting is surface speed, not RPM, because it scales with tool diameter.
The tool holder is the interface between the spindle and the cutter. Runout in that stack gets copied into the part. A holder with 0.005 mm runout cutting a 6 mm end mill will cut oversized on one flute and undersized on the other.
Surface finish follows directly. A sharp cutter, correct feed per tooth, and a rigid setup give Ra 0.8–1.6 μm straight off the machine. Pushing to Ra 0.2–0.8 μm usually means a finishing pass with a small stepover, or a separate finishing operation.
Hole accuracy is a separate problem. A drill follows its own point geometry and can wander. If a hole has to sit within ±0.005 mm of true position, it gets drilled undersize, then bored or reamed. The reamer follows the drilled hole, so the drilled hole must already be close.
- 1RunoutShow up in the part as size scatter between flutes.
- 2Finish passSmall stepover, high surface speed, light radial depth.
- 3Hole strategyDrill, then ream or bore when position matters.
When a vertical mill is the wrong machine
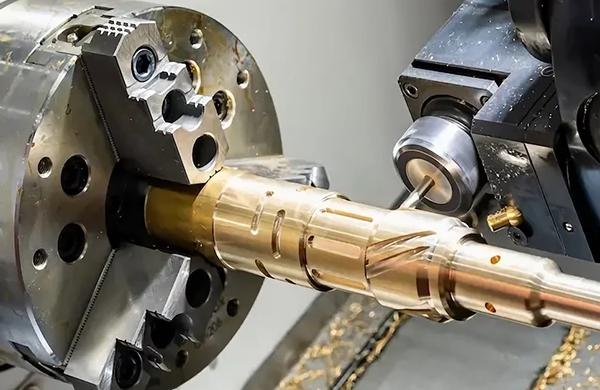
Vertical mills dominate flat and prismatic work. They lose on parts that are mostly round. A shaft with a single axis of symmetry, a bushing, or a threaded fitting cuts faster on a turning center, where the part spins and the tool stays still. Doing that job on a mill means interpolating a circle with an end mill, which is slower and leaves a scalloped surface.
Deep cavities are the second weak point. Tool length grows with depth, and a long tool bends. Past a certain depth-to-diameter ratio, roughly 4:1 in steel with a standard end mill, chatter becomes the limit rather than the machine.
Thin walls are the third. Clamping force deforms the part before the cutter touches it. We counter this with soft jaws, low clamping pressure, and light finishing passes, but the geometry itself sets the ceiling.
If your part is a large weldment, a casting with draft, or a sheet metal enclosure, milling may still be needed for the critical faces but it will not be the primary process. Knowing that early avoids a quote that surprises you.
- 1Round and axialTurning center wins on cycle time.
- 2Deep pocketsDepth-to-diameter ratio drives chatter, not spindle power.
- 3Thin wallsClamping, not cutting, causes the first out-of-tolerance feature.
Which machine fits the part
Match the geometry to the machine before you compare prices.
| Part geometry | Best machine | Why |
|---|---|---|
| Flat plate, pockets, slots | 3-axis vertical mill | Top access, few setups, tight tolerance |
| Round shaft or fitting | Turning center | Single-point tool, no interpolation |
| Faces on 4 sides of a block | 4-axis vertical mill | One index per face, fewer setups |
| Impeller or contoured mold | 5-axis machining center | Short cutter reaches steep walls |
| Deep narrow cavity | Sinker EDM or 5-axis | Long tools chatter past 4:1 in steel |
| Thin-wall housing | Vertical mill, light passes | Soft jaws and low clamp pressure |
| Large weldment face | Vertical mill, 4,000 mm travel | Facing pass on a stable setup |
The short answer
If your part is flat, prismatic, and reachable from above, a 3-axis vertical mill gives you the best tolerance for the money. If it is mostly round, choose turning. If the walls are steep or the part is a single complex form, pay for 5-axis and skip the extra setups.
Questions engineers ask next
What tolerance can a vertical mill hold in production?
On a rigid setup with a controlled tool path, we hold ±0.005 mm (±0.0002 in) on critical features across the run. That number assumes the feature is reachable with a short cutter and the fixture does not distort the part.
Tighter fits are possible on specific features by boring or by a finishing pass after the part has been allowed to settle. A blanket tolerance across every dimension on a drawing usually costs more than the part needs.
Does spindle orientation affect chip evacuation?
Yes. With the spindle vertical, gravity pulls chips down and away from the cut, so flood coolant carries them out of the pocket more easily.
In a deep, closed pocket the chips still collect at the bottom. That is where through-tool coolant or an air blast earns its place on the setup sheet, especially in aluminium where recutting a chip damages the finish.
Is a vertical mill the same as a machining center?
A machining center is a vertical (or horizontal) mill with an automatic tool changer and an enclosed work area. The cutting principle is identical.
The practical difference is unattended time. A tool changer lets one program run many operations without an operator standing at the spindle, which is what makes small and medium batch work economical.
How deep can an end mill cut before chatter sets in?
A common working limit is a depth-to-diameter ratio near 4:1 for a standard end mill in steel. Past that, the tool bends and the cut becomes noisy and dimensionally unstable.
The fix is not always a bigger tool. A tapered tool, a reduced neck, or a 5-axis approach that tilts the holder lets you reach the floor with a shorter effective length.
What materials run well on a vertical mill?
Aluminium 6061, 7075 and 6082, stainless 303, 304 and 316, and steels such as 1018, 4140 and 4340 are routine. Copper, brass, titanium Ti-6Al-4V, Inconel and engineering plastics like POM and PEEK are all machined here as well.
The material changes the cutting parameters, not the machine choice. Titanium and Inconel need lower surface speed and more coolant; plastics need sharp edges and high rake so the material shears instead of melting.
When should a part move off the vertical mill?
When the majority of the material removal is on a rotating axis, when the cavity is deeper than 4:1, or when the part cannot be clamped without deforming.
We flag this during the DFM review that comes with every quote within 12 hours, so you learn about the limit before you commit to a process.
Send the drawing, get a process answer
Upload a STEP file and we return a quotation plus a free DFM analysis within 12 hours, with the machine choice and tolerance limits written out. No minimum order quantity, from one prototype to 10,000+ parts.
12-hour quote100% inspectionNDA on request
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.











