
What Does CNC Machine: A Complete Explainer for Engineers
A CNC machine removes material from a solid block under numerical control, following a toolpath generated from CAD data. This page explains the mechanism, the tolerance limits, the materials it handles, and the cases where it is the wrong process.
In this article
- 1
- 2
- 3
- 4
- 5
- 6
- 7
What does CNC machine remove, and how does the toolpath decide it
A CNC machine is a subtractive tool. It starts with a solid block, bar, or plate and cuts material away until the remaining shape matches the drawing. The cutting edge never guesses: a CAM post-processor converts the CAD model into G-code, and the controller drives each axis to the coordinates in that code.
The difference between a CNC machine and a manual mill is not the spindle. It is the feedback loop. Ball screws, linear scales, and servo drives hold position to ±0.005 mm on a finished feature, and the same program repeats that position on part 1 and part 10,000. Manual machining depends on the operator's hand; CNC depends on the code and the rigidity of the setup.
Three motion types cover most work. Three-axis machines move X, Y, and Z, so undercuts and deep side walls need multiple fixtures. Four-axis adds rotation around one axis, which lets a single setup cut flats and holes around a shaft or a cube. Five-axis moves the tool or the table on two rotary axes at once, so a ball nose cutter can stay normal to a curved surface.
That last point matters for surface finish. On a contoured mold or an impeller blade, a three-axis path leaves visible stepover marks because the cutter angle changes as the surface tilts. A simultaneous five-axis path keeps the contact point consistent and reduces hand polishing. We run 16 simultaneous five-axis centers alongside 27 three-axis machines, because most features do not need five axes.
Which machine type fits which part
Milling covers prismatic parts: housings, brackets, manifolds, heat sinks, and mold inserts. The cutter spins and the work stays put, or the table feeds the work past the cutter. Pocket depth, wall thickness, and corner radius decide whether a standard end mill reaches the feature or an extended tool with reduced feed is required.
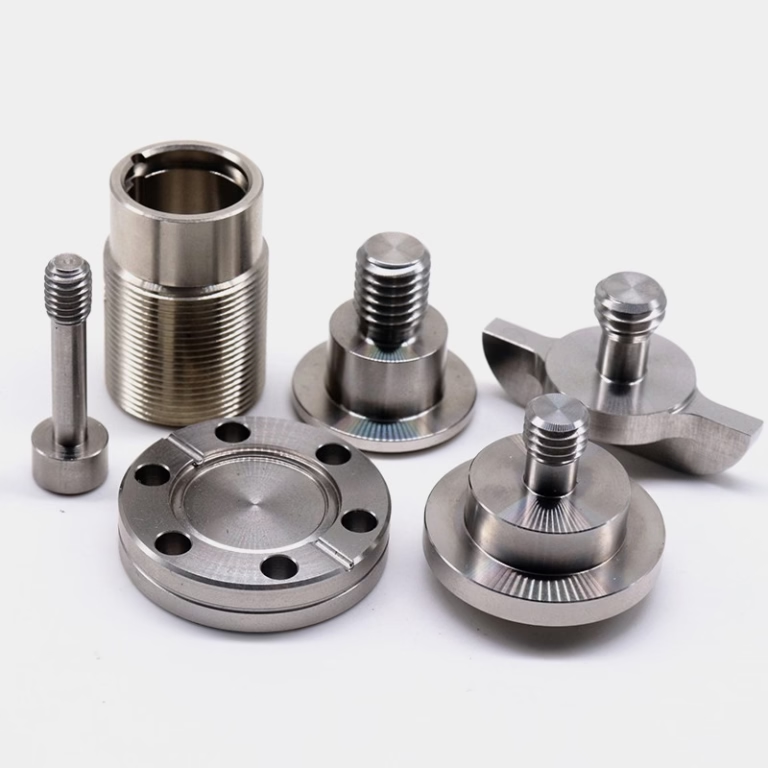
Turning covers round parts: shafts, bushings, fittings, and threaded connectors. The work rotates and a single-point insert removes material along the diameter. A mill-turn center does both in one setup, which removes the concentricity error that comes from flipping a part between two machines. We keep 16 mill-turn centers for exactly that reason.
Five-axis machining is the answer when a feature cannot be reached from three directions, or when one setup is worth more than a faster cycle. Typical parts are impellers, turbine housings, orthopedic bone plates, and complex brackets. The trade-off is programming time and a slightly slower cycle, so we only route a part to five axes when the geometry or the datum stack demands it.
Size sets the ceiling. GreatLight machines a maximum processing size of 4,000 mm, with travel envelopes of 4,000 × 400 × 150 mm on the large gantry and 750 × 1,150 × 550 mm or 600 × 600 × 600 mm on the mid-size verticals. Anything past the envelope gets split into segments or moved to a different process. A Ø400 mm rotary table handles round parts that need indexing.
What tolerance and finish a CNC machine can actually hold
Tolerance is not a single number you apply to the whole drawing. It is a budget you spend across datums, features, and the setup sequence. A general callout of ±0.1 mm is easy on almost any machine. A callout of ±0.005 mm needs a rigid setup, a sharp tool, thermal stability, and a CMM or optical comparator to verify it.
Finish follows the same logic. As-machined surfaces sit around Ra 1.6–3.2 μm. A finer insert or a smaller stepover gets Ra 0.8–1.6 μm. Surfaces below Ra 0.8 μm usually need a finishing pass with a small nose radius, a slower feed, or a secondary operation such as polishing or lapping.
The interaction between tolerance and finish is where drawings go wrong. A tight diameter tolerance with a rough surface finish is unusual, because the tool marks themselves occupy part of the tolerance band. If a bore must hold ±0.005 mm, the surface has to be fine enough that the measurement is repeatable.
We hold ±0.005 mm (±0.0002 in) on critical features and inspect 100% of parts before shipment, with raw material check, in-process monitoring, and final inspection. Inspection reports are available on request. The number is not a marketing claim; it is what the metrology room can document.
Materials a CNC machine cuts well, and materials that fight back
Aluminum is the default for prototypes and most enclosures. 6061 and 6061-T6 machine fast and hold a good finish, 7075 gives higher strength for structural brackets, and 2024 is common in aerospace work. Aluminum cuts at high spindle speeds, so cycle time stays low even on complex pockets.
Stainless steel is where tool wear shows up. 303 is free-machining and behaves well on a lathe. 304 and 316 work-harden if the feed is too light, so the cutter must stay engaged and take a real chip. 17-4PH (SUS630) machines in the annealed condition and then ages to high strength, which suits pump shafts and valve bodies.
Titanium and nickel alloys need low surface speed, high coolant pressure, and sharp tools. TC4 (Ti-6Al-4V) and Inconel are cut at a fraction of the aluminum feed rate, and the toolpath has to avoid dwelling in the cut. These materials are selected for temperature or corrosion resistance, not for machinability.
Plastics and composites behave differently again. POM and PEEK cut cleanly but move with heat, so roughing and finishing passes are separated to let the part cool. Carbon fiber is abrasive and needs diamond-coated tooling and dust extraction. Cutting forces are low; the risk is delamination and frayed edges, not spindle load.
When CNC machining is the wrong process
CNC machining is a poor fit for thin-walled shells produced in high volume. If a part is a hollow housing with 1 mm walls and the annual volume is 50,000 pieces, injection molding or die casting wins on unit cost after tooling amortizes. CNC stays competitive from one prototype to 10,000+ parts, but the crossover depends on geometry and cycle time, not on a fixed rule.
Deep, narrow cavities are another boundary. A pocket that is 8 mm wide and 80 mm deep needs an end mill with a 10:1 length-to-diameter ratio, which deflects under cutting force. The result is a tapered wall and a poor floor finish. If the drawing allows it, widening the pocket or splitting the part removes the problem.
Sharp internal corners are physically impossible with a rotating cutter. Every inside corner carries the radius of the tool, so a drawing that calls for a zero-radius corner cannot be machined as drawn. The corner either gets a radius callout or the feature moves to EDM, which is slower and costs more.
Hardened material above roughly 45 HRC is usually a grinding or EDM job, not a milling job. We can cut pre-hardened steel in the 30–40 HRC range with carbide tooling and reduced depth of cut, but a fully hardened die insert is finished by other means.
From CAD file to finished part: the actual sequence
- 1Review the model and DFMWe check wall thickness, tool reach, corner radii, and datum strategy, then return a DFM analysis with the quotation within 12 hours.
- 2Fix the setup and datumChoose the fixture and the zero point. Features held in one setup keep their relative position; features across setups inherit the fixture error.
- 3Rough the stockRemove the bulk of the material with a larger tool at a high material removal rate, leaving 0.3–0.5 mm of stock for finishing.
- 4Semi-finish and finishSwitch to a smaller or ball nose cutter. Feed and stepover are set by the finish callout: 0.05–0.2 mm stepover for Ra 0.8–1.6 μm.
- 5Deburr and inspectBreak edges, then measure the critical features against the drawing. Inspection reports are available on request.
- 6Finish and markAnodizing, plating, powder coating, bead blasting, or laser marking to a minimum character height of 1.5 mm.
Machine type vs part geometry and practical limits
Pick the lowest axis count that reaches every feature in one setup.
| Machine type | Best for | Practical limit | Typical tolerance |
|---|---|---|---|
| 3-axis mill | Prismatic parts, open pockets, plates | No undercuts in one setup | ±0.01 mm |
| 4-axis mill | Shafts, cubes, holes around a bore | One rotary axis only | ±0.01 mm |
| 5-axis simultaneous | Impellers, contoured surfaces, bone plates | Higher programming cost | ±0.005 mm |
| Mill-turn center | Round parts with milled flats | Bar diameter and length | ±0.005 mm |
| Swiss-type lathe | Long, slender turned parts | Small diameter range | ±0.005 mm |
The short answer
If the geometry needs tight tolerance, real engineering material, or one to a few thousand parts, CNC machining is the right call. If the part is a thin hollow shell at high volume, injection molding or die casting will beat it on unit cost.
Questions engineers ask next
Does a CNC machine only cut metal?
No. The same machine cuts engineering plastics, composites, and graphite with the right tooling and dust control. What changes is the cutting parameter set: spindle speed, feed per tooth, and coolant strategy.
Soft plastics cut at high spindle speed with sharp, polished flutes. Abrasive composites need coated tooling and extraction. The machine structure stays the same.
How close can two CNC parts be to each other?
Repeatability comes from the ball screws, the servo loop, and the fixture, not from the operator. On a stable setup with the same program, part-to-part variation on a critical feature stays inside the tolerance band we verified on the first article.
That is why the first article inspection matters. Once the setup is proven, the process repeats it. We hold ±0.005 mm on critical features and inspect 100% of parts before shipment.
What file format do you need for a quote?
STEP or IGES for the 3D model, plus a 2D drawing in PDF with the tolerance, finish, and material callouts. If the drawing is the only document, we can work from that, but we will flag any feature that cannot be verified from 2D alone.
Send the files through the quote page. Uploads are secure and confidential, and an NDA is available on request.
Can a CNC machine produce a part with no minimum order?
Yes. There is no minimum order quantity, so a single prototype and a 10,000+ part run go through the same process. The first article is inspected, and the same program carries into production.
Production can start within 24 hours of an approved quotation, and parts typically ship in 3–5 days depending on quantity and finishing.
Why do inside corners always have a radius?
Because the cutting tool is round and spins. The tool cannot enter a corner tighter than its own radius, so the machined corner always carries that radius.
If the function of the part requires a sharp corner, the options are a smaller tool with a longer reach, a relief notch, or EDM. Each one trades cycle time or cost for the geometry.
How do certifications affect a CNC order?
Certifications describe the quality system around the machining, not the machine itself. GreatLight holds ISO 9001:2015, IATF 16949:2016, ISO 13485:2016, and ISO 27001:2022.
For automotive and medical work, that means documented traceability, controlled processes, and information security for your drawings. Ask for the certificate scope before you place a production order.
Send a drawing, get a machinability answer
Upload your model and drawing. We return a quotation and a free DFM analysis within 12 hours, with the tolerance and finish we can actually hold.
12-hour quote100% inspectionNo minimum order
More from the shop floor
We publish setup notes, tooling trials and inspection data from the factory floor.











