
01
A tolerance no process can hold
You call out ±0.005 mm on a 300 mm aluminum bracket. The machine can hold it. The part will not, because thermal growth and tool deflection eat the budget on a long unsupported section. One re-cut costs a week.
A working reference set for engineers who have to release parts. Setup rules, fixture clamps, tolerance budgets, material choices, and the questions worth asking before a drawing goes to the machine.

Most scrap is decided before the first cut. These are the recurring ones.
You call out ±0.005 mm on a 300 mm aluminum bracket. The machine can hold it. The part will not, because thermal growth and tool deflection eat the budget on a long unsupported section. One re-cut costs a week.
A 0.8 mm wall on a 6061 housing looks fine in CAD. In the vise it springs, and the second op distorts the first. You get oval bores and a scrapped batch instead of a prototype.
A drawing datumed to a theoretical intersection gives the operator nothing to indicate against. Setup time doubles, and the inspection report cannot prove the part is good. Fix the datum before you fix the tolerance.
Low price, then a change order once the shop finds the 5-axis work. Without a DFM pass, the second quote arrives after the schedule is already committed. Ask for the process plan up front.
What we check, what we clamp, and what we hand back with the parts.

A 16-station 5-axis cell still cuts a bad part if the blank moves. Before toolpath work, we look at three things: where the clamp contacts, how many times the part is re-fixtured, and whether the operator can reach the datum with a probe. A part that needs four setups will lose accuracy at every handoff.
For thin walls and long shafts we switch to soft jaws, vacuum plates, or a Ø400 mm rotary table so the part rotates instead of being re-clamped. That keeps one datum for the whole cycle and removes the stack-up from re-indicating.

Every job gets a raw material check, in-process monitoring, and a final inspection before it ships. On tight features we record the actual number, not a pass or fail. That record is what you take into your own assembly, and it is what tells us whether a process is drifting before the next batch starts.
If a feature is hard to inspect, it is usually hard to machine. We flag it during DFM and suggest a change: a wider relief groove, a flat instead of a radius, or a dimension that can be reached with a standard gauge instead of a CMM probe.
Typical capability on stable materials. Long or thin parts shift the number.
| Operation | Typical tolerance | Best for |
|---|---|---|
| 3-axis milling | ±0.01 mm | Prismatic parts, flat faces, open pockets |
| 4-axis milling | ±0.01 mm | Multiple faces, one rotation, fewer setups |
| 5-axis simultaneous | ±0.005 mm | Contoured surfaces, impellers, angled holes |
| CNC turning | ±0.005 mm | Shafts, bushings, threaded bodies |
| Mill-turn | ±0.005 mm | Turned and milled features in one setup |
One shop, one quote, from a single prototype to a 10,000 plus run.
Sixteen simultaneous 5-axis centers for contoured surfaces, deep cavities, and angled holes that would need three setups on a 3-axis mill.
Up to 4,000 mm travel for large frames, and mill-turn centers that finish a turned body and its milled features without re-clamping.
One-off parts in 3 to 5 days. Same inspection standard as production, so the prototype and the run are measured the same way.
Brackets, enclosures, and chassis parts where the geometry is flat and the volume is higher than a milled version would justify.
For fit checks and low-stress covers before tooling. Useful when a machined version would be wasted on a shape that is still changing.
Anodizing, plating, powder coat, bead blasting, and laser marking. We run the finish after the final inspection, not before.
If your grade is not here, ask. The answer is usually still yes.
| Group | Grades | Notes |
|---|---|---|
| Aluminum | 6061-T6, 7075, 2024, 6082 | Best all-round machinability |
| Stainless | 303, 304, 316L, 17-4PH | 17-4PH for strength and corrosion |
| Steel | 1018, 4140, 4340, A36 | 4140 for shafts and tooling bodies |
| Titanium | TC4 (Ti-6Al-4V), TA2 | Slow speeds, tight tool control |
| Plastics | POM, PEEK, PC, ABS | PEEK for high-temperature parts |
Six things a buyer or engineer can check before placing an order.
On stable materials and reachable features. We will say so in the DFM note when a callout is not realistic, instead of quoting it and missing it.
3-axis, 4-axis, 5-axis, and mill-turn under one roof, so a part that needs several operations does not travel between suppliers.
Quotation and a free DFM analysis within 12 hours of a drawing and a quantity. Production can start within 24 hours after approval.
Typical lead time on standard parts. Historical late-delivery probability is below 2 percent.
We run a single prototype on the same equipment as a production batch, so the first article and the run match.
Quality and information security systems audited to the standard your industry asks for. NDA available on request.
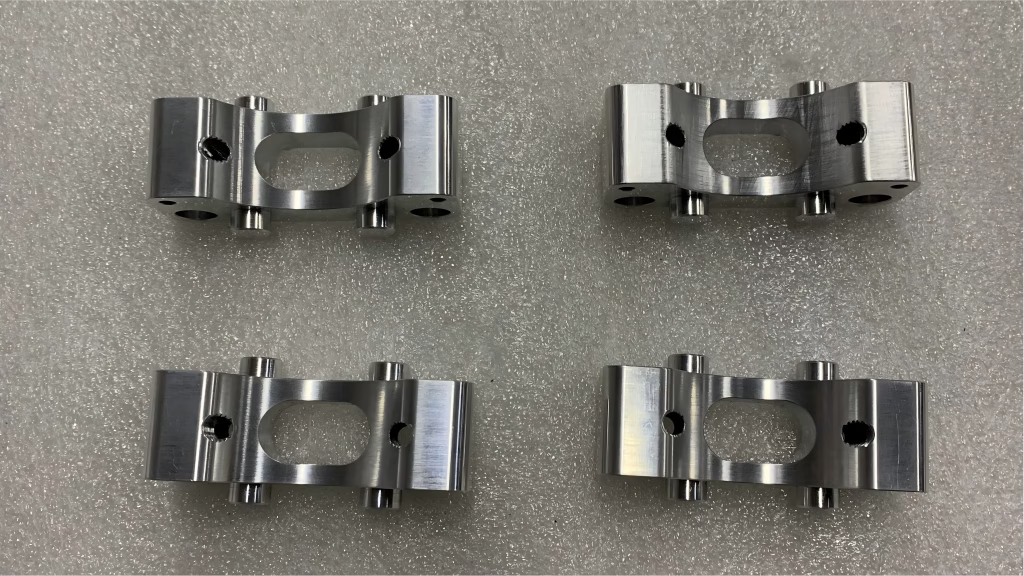
Thin-wall housings and brackets where weight and stiffness both matter.

Motor housings, busbars, and fixtures that repeat across a build cycle.
Instrument bodies and manifolds with cleanable surfaces and traceable stock.

Large frames and plates up to 4,000 mm, machined in one setup where possible.
STEP and IGES for 3D, PDF or DXF for the 2D drawing with tolerances and datums. A drawing matters more than the model. The model shows the shape, the drawing shows what has to be measured.
If you only have a model, send it. We will state the tolerances we plan to hold and ask you to confirm them before cutting.
Yes. There is no minimum order quantity, so a single prototype is a normal order. Prototypes typically ship in 3 to 5 days after drawing approval.
The prototype is inspected to the same standard as a production lot, so the report you receive is the report you will keep getting.
Send the drawing, the quantity, the material, and any finish requirement. We return a quotation and a free DFM analysis within 12 hours.
If a feature will drive cost or risk, we say so in that reply, with the alternative. You decide before anything is cut.
Three gates: raw material certificates before the first cut, in-process monitoring on repeating features, and a final inspection before shipment. Every part is inspected, not sampled.
Inspection reports are available on request. If you need specific data points recorded, tell us on the drawing and we will log them.
Use 5-axis when a part has contoured surfaces, angled holes, or features on five faces that would otherwise need three or more setups. The gain is accuracy from fewer handoffs, not just speed.
For a flat bracket with two drilled holes, a 3-axis mill is cheaper and just as accurate. We will quote the simpler process if it meets the drawing.
Uploads are treated as confidential, and we sign an NDA on request before drawings are shared. Our information security management system is certified to ISO 27001:2022.
If your program requires it, tell us at the quote stage so the paperwork is in place before files move.
Tolerance to ±0.005 mm on reachable features in stable materials. Surface finish from Ra 0.2–0.8 μm on fine work, Ra 0.8–1.6 μm on standard machined surfaces, and Ra 1.6–3.2 μm as-machined.
The limit is usually part geometry, not the machine. A long thin wall will move no matter which spindle cuts it, so we flag that in DFM.
Yes. Send the drawing as issued, including datum structure and any profile callouts. We review whether each datum can be reached in the fixture before quoting.
If a datum is theoretical or unreachable, we propose a practical one and explain the effect on inspection, so the change is documented rather than assumed.
Upload a STEP file and a 2D drawing. We return a quotation and a free DFM analysis within 12 hours, with the operations, tolerances, and risks written out.
12-hour quote100% inspectionNo MOQNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.