
01
The part warps off the bed
Large flat ABS or PP panels cool unevenly and curl at the corners. If the first layer lifts more than 0.5 mm, the whole build is scrap and the assembly will not sit flat.
Pick a plastic, a process, and a layer height that survive real use. We print prototypes and small runs, then machine the same geometry in POM, PEEK, or ABS when the plastic part has to hold tolerance.
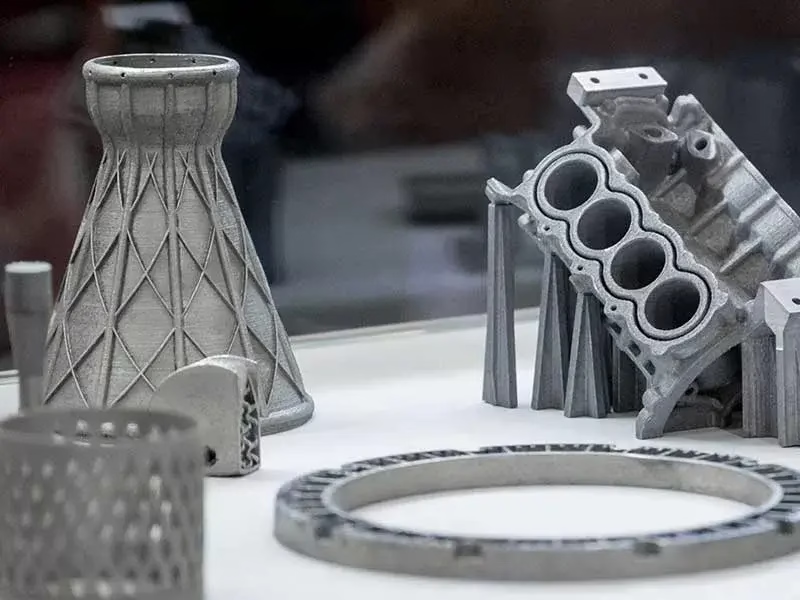
Most plastic print problems are decided before the file is uploaded. Here is what we see on incoming jobs.
Large flat ABS or PP panels cool unevenly and curl at the corners. If the first layer lifts more than 0.5 mm, the whole build is scrap and the assembly will not sit flat.
Printed threads below M4 shear when a screw is torqued. The fix is a metal insert or a machined boss, not a finer layer height.
A PLA bracket that holds 20 kg for a week will bend and stay bent. Load-bearing parts need a different polymer, or a machined part.
FDM parts shrink as they cool. Without a shrink factor dialed in, holes come out 0.2–0.4 mm undersized and pins will not fit the mating plate.
Seven processes under one roof, plus CNC when the print cannot hold the tolerance.
PLA is the easiest to print and the cheapest per part, but it creeps under load and softens near 60 °C. Use it for form checks and display models. PETG adds toughness and a wider working range, and it prints almost as easily.
ABS and ASA bring low-temperature impact resistance, dimensional stability, and good chemical resistance, so they suit enclosures and functional housings. Nylon is strong, wear-resistant, and low in density, which makes it the usual choice for living hinges, clips, and gears.

FDM lays a thermoplastic filament down in layers from 0.1 mm to 0.3 mm. It is the workhorse for brackets, housings, and fixtures, and it takes inserts and tapped holes well if you design enough wall.
SLA and DLP cure liquid resin with light, so they hold detail that FDM cannot. Resin parts come out smooth and dimensionally tight, which is why dental models, surgical guides, and small connectors go that route. SLS sinters nylon powder with no support marks, so it handles nested geometry and small production batches.
Mechanical values vary by supplier and print orientation. Use this to narrow the list, then confirm with a test part.
| Material | Heat resistance | Best for |
|---|---|---|
| PLA | Low, softens near 60 °C | Form checks, jigs, display models |
| PETG | Moderate, about 70 °C | Tough covers, transparent parts |
| ABS / ASA | Moderate, about 90 °C | Enclosures, housings, interior trim |
| Nylon PA12 | Moderate to high | Clips, gears, living hinges |
| Resin (SLA) | Low to moderate | Dental, surgical guides, fine detail |
| POM (machined) | Moderate, about 90 °C | Tight-tolerance moving parts |
| PEEK (machined) | High, above 250 °C | High-temperature and chemical service |
Print, machine, finish, and inspect from one shop. That removes the handoff where tolerance usually gets lost.
FDM, SLA, DLP, and SLS in PLA, ABS, PETG, nylon, and resin. One part or a small production batch.
Printed form and fit models, then a machined version of the same geometry for functional testing.
POM, PEEK, ABS, PC, PMMA, and PA machined to ±0.005 mm when a printed part cannot hold size.
Silicone molds from a printed master for 10–50 polyurethane parts with a consistent surface.
Bead blasting, tumbling, painting, and laser marking with a minimum character height of 1.5 mm.
Metal frames and enclosures that the printed plastic covers, brackets, and guides mount onto.
Every job follows the same route, whether it is one part or a thousand.
| Item | What we do | Output |
|---|---|---|
| File review | Check wall thickness, draft, and hole size | DFM notes within 12 hours |
| Material | PLA, ABS, ASA, PETG, PA12, resin | Matched to load and temperature |
| Build | FDM 0.1–0.3 mm, SLA, DLP, or SLS | Parts plus support removal |
| Machining | Holes, faces, and threads cut after printing | Critical features to ±0.005 mm |
| Inspection | Raw material check, in-process, final | Reports on request |
| Shipping | Protected packs, batch labels | Parts ship in 3–5 days |
The reason most plastic printing projects stall is that no one can fix the geometry. We can.
Operating since 2011 across three wholly-owned plants and 7,600 m² of floor space, with 150 technicians on staff.
When a printed plastic part needs a flat face or a true bore, it moves to a mill instead of waiting on a new supplier.
Printed parts hold roughly ±0.1 mm. Critical features can be cut after printing to ±0.005 mm, or ±0.0002 in.
Quotation and free DFM analysis within 12 hours. Production can begin within 24 hours of approval.
Parts ship in 3–5 days, and the historical probability of a late shipment sits below 2%.
Raw material check, in-process monitoring, and final inspection on every order. Reports on request.
Snap fits and cosmetic covers need a clean surface and repeatable wall thickness. ABS and ASA hold the shape; printed masters feed vacuum casting for 10–50 units.
Cases must close flush and survive a drop. We print the shell, then machine the mating faces and hinge bores so the lid lines up.
Moving joints need clearance, wear resistance, and no creep. Nylon or machined POM replaces PLA, and pivot holes are reamed after printing.
Internal channels and lattice shapes rule out milling. SLS nylon prints them without support marks, and we inspect wall thickness before the run.
Start with the load and the temperature. PETG covers most general functional parts with better toughness than PLA.
For clips, gears, and living hinges, use nylon. For enclosures that see heat or chemicals, use ABS or ASA. PLA stays on the shelf as a form-check material.
Expect roughly ±0.1 mm on a well-oriented FDM part, and better on SLA or DLP for small features. Hole diameters drift undersized because the material shrinks as it cools.
If a bore, face, or thread must be true, we print oversize and cut it after printing. That gets critical features to ±0.005 mm.
Switch when the part carries a sustained load, sees more than 90 °C, or needs a tolerance tighter than ±0.1 mm.
Printed plastics also creep. If a bracket holds a constant load for weeks, a machined POM or PEEK part is the safer route. We quote both so the comparison is direct.
Printed threads below M4 tend to strip. Use a heat-set insert or a machined boss for anything that gets assembled more than once.
We can tap the printed part where the wall is thick enough, or cut the thread after printing on a mill.
Aim for 1.5–2.5 mm walls on FDM parts, with at least three perimeters. Thinner walls flex and print with gaps.
Layer height runs 0.1–0.3 mm. Use 0.1 mm for visible or mating surfaces and 0.2–0.3 mm for large non-critical shapes.
We print in the standard colors the material comes in, then finish from there. Options include bead blasting, tumbling, painting, and polishing.
Laser marking is available with a minimum character height of 1.5 mm.
Uploads are secure and confidential, and we can sign an NDA on request. Files are used only for quoting and producing your parts.
We hold ISO 27001:2022 for information security, so document handling follows a documented process.
There is no minimum order quantity. We run one prototype or a 10,000+ part batch.
For a batch above a few hundred units, we compare printing against vacuum casting and machining and quote the cheaper route.
Upload your file and we return a quotation with free DFM analysis within 12 hours. If printing is the wrong process for that part, we will say so and quote the alternative.
12-hour quote100% inspectionNo minimum orderNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.