
Aylesbury CNC Machining Service: A Process Guide for Engineers
This page explains how our machining service works, what part geometry and materials suit 5-axis and mill-turn work, and where the limits sit. It is written for design and manufacturing engineers who need to judge whether outsourced precision machining fits a project. After reading, you should know which questions to ask a supplier and how to read a quote.
What an Aylesbury CNC machining service actually covers
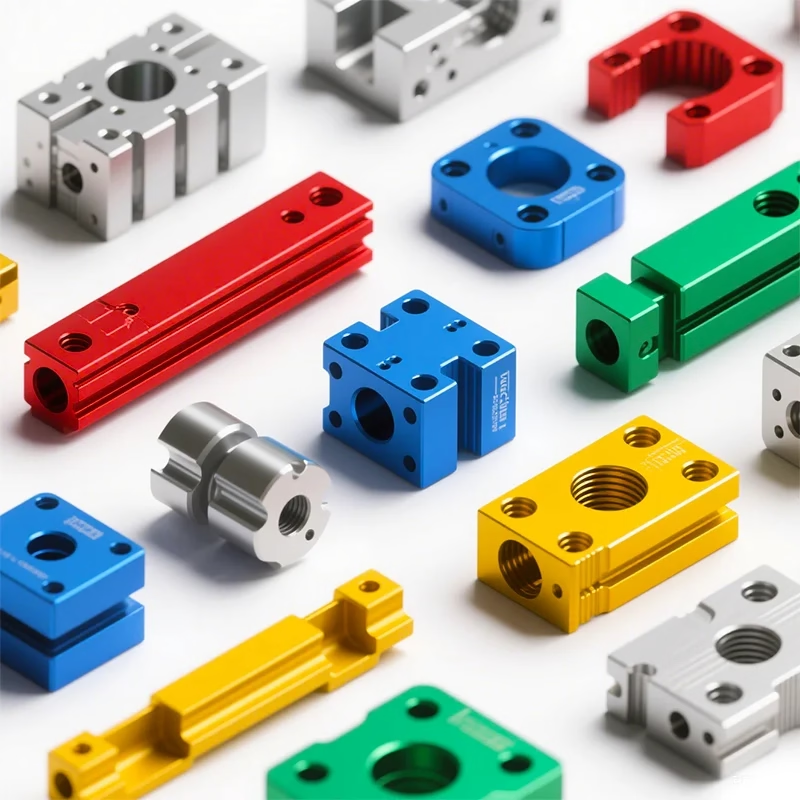
Machining turns a CAD model into a metal or plastic part by removing material on controlled machine tools. The scope is wider than milling a block. It includes turning, mill-turn work, drilling, tapping, boring, thread milling and surface finishing, plus the inspection that proves each feature is in tolerance.
Most buyers in Aylesbury come to us with a drawing and a deadline. They want to know whether the geometry can be held, which material suits the load case, and how many setups the part will need. Those three answers drive cost more than the machining itself.
We run 127 high-precision CNC machines across three wholly-owned plants, with 16 simultaneous 5-axis machining centers and 16 mill-turn centers. Maximum processing size reaches 4,000 mm. Parts ship in 3–5 days once production starts, and no minimum order quantity applies, so a single prototype and a 10,000-part run use the same process route.
When 5-axis helps and when it does not
A 5-axis machine adds two rotation axes to the usual X, Y and Z. The tool can reach the workpiece from almost any angle in one setup. That matters on parts with compound angles, deep pockets, thin walls or features on five faces. Fewer setups means fewer datums stacked on top of each other, so position error stays lower.
Not every part needs it. A flat plate with holes on one face runs faster and cheaper on a 3-axis mill. Simple round parts belong on a lathe. We keep 27 three-axis machines and 12 four-axis mills for exactly that reason, and we will say so when the geometry does not justify the higher rate.
The parts that benefit most are structural brackets, housings, impellers, manifolds, medical instruments and robot arm joints. Contour accuracy improves because the tool stays in contact with the surface at a consistent angle. Setup count drops from four or five to one, which shortens lead time and removes re-fixturing error.
- 1Use 5-axisCompound angles, five-face access, thin walls, tight true position between faces.
- 2Use 3-axisSingle-face geometry, flat plates, prismatic parts with simple tolerances.
- 3Use mill-turnRound parts with milled flats, cross holes or slots on the same axis.
- 4Use 4-axisCylindrical parts needing features indexed around the circumference.
Matching machine type to part geometry
Use this as a first filter before you request a quote. Travel figures are the working envelope, not the part size limit.
| Machine type | Best for | Typical travel | Watch out for |
|---|---|---|---|
| 3-axis mill | Flat plates, single-face pockets | 500 × 500 × 450 mm | Multiple setups on angled faces |
| 4-axis mill | Indexed features on round parts | 500 × 310 × 200 mm | No simultaneous contouring |
| 5-axis center | Compound angles, five-face access | 750 × 1,150 × 550 mm | Higher hourly rate than 3-axis |
| 5-axis center | Large structural parts | 4,000 × 400 × 150 mm | Long parts need support planning |
| Mill-turn | Turned parts with milled features | Ø400 mm rotary table | Bar stock size limits the blank |
| Compact 5-axis | Small medical and electronic parts | 600 × 600 × 600 mm | Small tools wear faster |
Materials, tolerances and surface finish
Aluminium 6061-T6 is the default for prototypes and brackets. It machines fast, holds ±0.005 mm on most features and takes anodizing well. Where strength matters more, 7075 and 2024 give higher yield but cut slower and can move after stress relief, so we rough, relieve and finish in separate operations.
Stainless 303 and 304 cover most general work. For medical and food equipment, 316L and 17-4PH hold up better against corrosion and can be passivated. Titanium Ti-6Al-4V (TC4) and Inconel are common in aerospace and energy parts, but tool wear is high and cycle times run three to five times longer than aluminium.
Surface finish depends on the process, not just the machine. As-machined surfaces land around Ra 1.6–3.2 μm. A finishing pass gets to Ra 0.8–1.6 μm. Where Ra 0.2–0.8 μm is specified, we add a controlled finishing operation or a secondary process. Laser marking has a minimum character height of 1.5 mm, which matters for part numbering on small components.
- 1Aluminium6061, 6061-T6, 2024, 5052, 5083, 6063, 6082, 7075, ADC12.
- 2Stainless303, 304, 316, 316L, 420, 430, 431, 440C, 17-4PH.
- 3Titanium and nickelTA1, TA2, TC4, Inconel, magnesium AZ31B and AZ91D.
- 4PlasticsABS, PC, PMMA, POM, PA, PEEK, PP, HDPE, carbon fibre.
How we hold tolerance and prove it
Tolerance is only useful if it is measured. Every job gets a raw material check, in-process monitoring and a final inspection before shipment. We inspect 100% of parts, not a sample, and we send inspection reports when the drawing calls for them.
Our qualification rate sits at 99.99%. That number comes from the inspection record, not a marketing claim. When a feature is marginal, we flag it during the DFM review rather than after the first article, because changing a tolerance on a drawing is cheaper than scrapping a batch.
The plants hold ISO 9001:2015, IATF 16949:2016 for automotive, ISO 13485:2016 for medical devices and ISO 27001:2022 for information security. The last one matters if your drawings are confidential. Uploads stay secure and confidential, and we sign an NDA on request.
What to send and what comes back
Send a STEP or IGES file plus a 2D drawing with tolerances, material, finish and quantity. The drawing carries the GD&T and the notes the model cannot express. Without it, we have to guess which features are critical, and guessing adds cost on both sides.
A quotation and free DFM analysis come back within 12 hours. The DFM notes list any feature we think will be hard to hold, any tolerance that looks tighter than the function needs, and any setup that could be removed by a small design change. Production can start within 24 hours of approval.
Delivery runs 3–5 days for most parts. Our historical late-delivery probability is below 2%, which reflects scheduling and capacity rather than a promise about any single order. Volumes range from one prototype to 10,000+ parts with no minimum order quantity.
Aylesbury buyers usually care about two things: whether the part will fit, and whether the schedule will hold. Both answers depend on the drawing and the process route, so we would rather discuss them before the quote than after the shipment.
Common questions about CNC machining
What is the difference between 3-axis and 5-axis machining?
A 3-axis machine moves the tool along X, Y and Z only. The workpiece stays fixed, so any feature on a different face needs a new setup.
A 5-axis machine adds two rotation axes, usually A and B. The tool reaches the workpiece from almost any angle in one setup. That improves contour accuracy, cuts setup time and often gives a better finish on curved surfaces.
Which materials can you machine?
Aluminium alloys including 6061, 2024, 5052, 6082 and 7075, stainless steels 303 through 17-4PH, carbon and alloy steels, brass and copper, titanium grades TA1, TA2 and TC4, Inconel, magnesium, and engineering plastics such as POM, PEEK and PC.
If your material is not on the list, send the specification. We will tell you whether we can hold the tolerance in it.
How tight a tolerance can you hold?
We work to ±0.005 mm (±0.0002 in) on critical features, depending on material, feature size and geometry. Very thin walls, deep bores and long unsupported sections are harder to hold than a bore in a solid block.
Send the drawing and we will confirm which features can hold that tolerance and which need a wider band.
What surface finishes are available?
As-machined surfaces run Ra 1.6–3.2 μm. A finishing pass reaches Ra 0.8–1.6 μm, and Ra 0.2–0.8 μm is possible with an added finishing operation.
Secondary finishes include anodizing in clear, colour, hardcoat and conductive types, electroless nickel, zinc, silver and gold plating, powder coating, black oxide, bead blasting, tumbling, brushing and polishing.
How do I get a quote and how fast?
Upload a STEP or IGES file with a 2D drawing showing tolerances, material, finish and quantity. The drawing is what lets us quote accurately.
You get a quotation and free DFM analysis within 12 hours. Production can start within 24 hours of approval, and most parts ship in 3–5 days.
Is there a minimum order quantity?
No. We run from a single prototype to 10,000+ part runs on the same process route.
Prototypes and production parts use the same machines and inspection steps, so the first article tells you what the production run will look like.
Send your drawing, get a process answer
Upload a STEP file and 2D drawing for a quotation and free DFM analysis within 12 hours. An engineer will tell you which machine fits the geometry and where the tolerance risk sits.
12-hour quoteFree DFM analysis100% inspectionNDA on request









