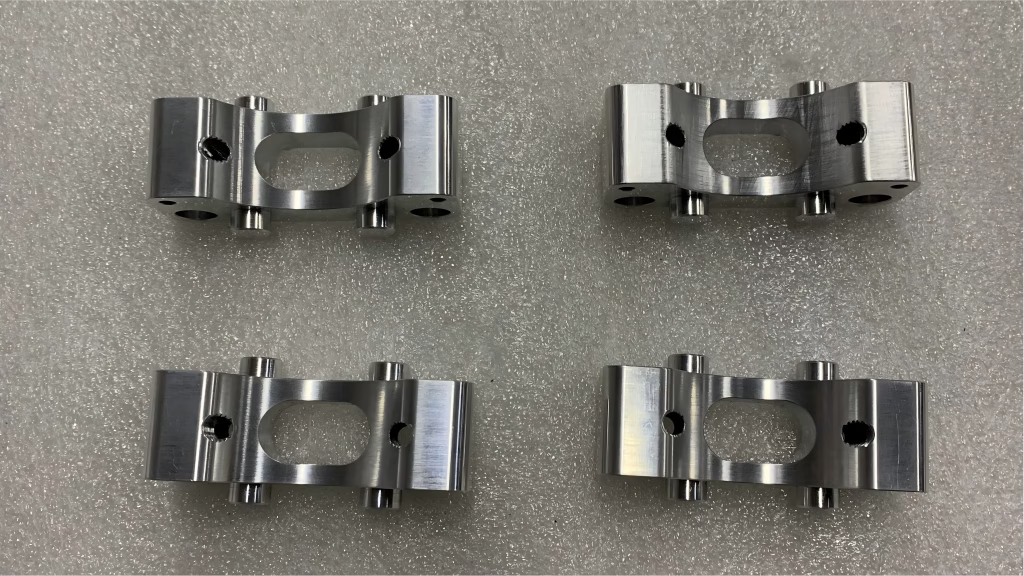
Surface and inspection
The wetted surface is a function, not a cosmetic
In chloride and hypochlorite service, pits start at machining marks. We hold Ra 0.8–1.6 μm as the working finish for sealing and wetted faces, and reach Ra 0.2–0.8 μm where the drawing asks for it. Polishing follows the direction of flow, not the direction that is easiest on the lathe.
Every lot gets a material check, in-process monitoring on critical features, and a final inspection before shipment. Reports come on request. If a bore or a seal face has a tolerance tighter than the process can hold repeatedly, we say so at the DFM stage rather than after the first article.
- 1
Ra 0.8–1.6 μmStandard finish for wetted and sealing faces
- 2
Ra 0.2–0.8 μmFine finish for critical seal surfaces
- 3
100% inspection before shipmentRaw material check, in-process, final