GreatLight CNC Machining Factory logo
CNC Machining
Rapid Prototyping
Materials
Industries
News
About GL

Get Instant Quote

Sheet Metal Bending & CNC Machining

Custom Metal Bracket Metal Bending

We bend, machine and finish custom metal brackets for mounting, framing and load-bearing joints. Cut from aluminum, stainless or steel, formed on press brakes, then anodized or powder coated to your drawing.

Bend angle controlAnodizing & powder coating±0.005 mm machiningOne-off to 10,000+ parts
custom-sheet-metal-fabrication-services1
127High-precision CNC machines
±0.005 mmMachining tolerance
12 hQuote and free DFM analysis
99.99%Qualification rate
Where brackets go wrong

Bracket Problems That Show Up After Assembly

Most bracket failures are not design failures. They are bending, hole and finish problems that only appear when the parts are bolted together.

01

Holes do not line up at the frame

Bend deduction was taken from a nominal thickness, so the hole center shifts after forming. The bracket reaches the assembly line and the bolt pattern fights the mating frame. Rework means drilling oversized holes or scrapping the batch.

02

Springback changes the angle

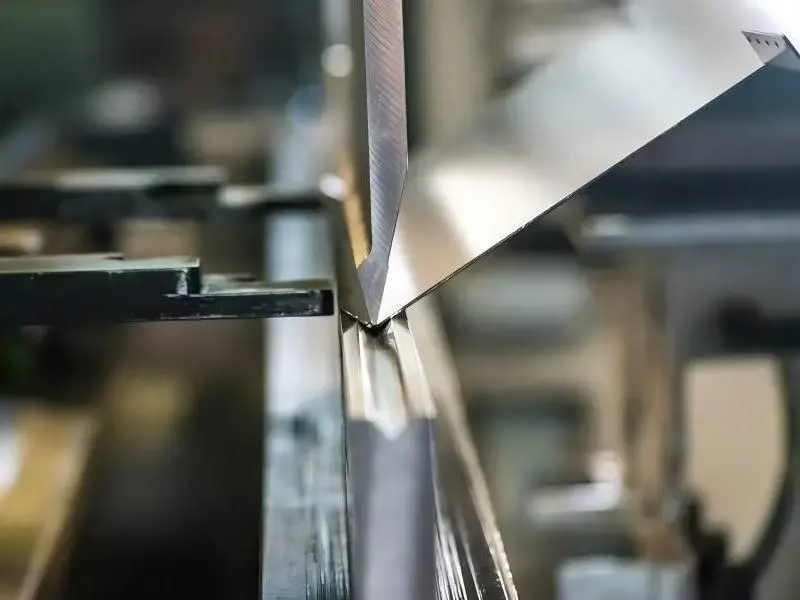
Aluminum 5052 and 6061 spring back differently, and a 90° bend comes off the press brake at 92° or 88°. The bracket rocks on the mounting face, torque pulls the joint loose, and the whole assembly needs shimming.

03

Coating builds up on the threads

Powder coating adds 60–100 μm per side. Masking is skipped, so the coated bracket no longer accepts a screw and the masking job moves to your assembly line. Threads get chased by hand and the finish chips around the hole.

04

The finish fails outdoors in one season

A clear anodize seal that was too thin, or a powder coat cured below spec, shows up as chalking and white corrosion on brackets that sit outside. Replacement parts cost more than the original order.

How we build brackets

One Drawing, One Route, From Coil to Coated Bracket

We quote the process route, not just the part.

aluminum-alloy-industrial-control-chassis-sheet-metal-processing
Forming

Press brake work set from the material, not the drawing nominal

Bend deduction and K-factor are calculated per material lot. We measure the actual sheet thickness, then set the tooling so the flat pattern produces the hole spacing your assembly needs. For 6061-T6 we adjust the radius and use a larger die opening to avoid cracking on the outside of the bend.

Holes closer than 2.5× material thickness to a bend line get moved or the part gets a relief slot. That is a DFM note, not a surprise at assembly. We flag it in the free DFM report that comes back with the quote.

  • 1
    Angle control±0.5° on formed bends, verified against the first article
  • 2
    Thickness range0.5 mm to 6 mm sheet, harder alloys machined instead
  • 3
    Flat pattern checkFirst-off part measured before the run continues

Get Instant Quote

cnc-machining-metal
Machining

When the bracket needs a machined face, we do it in the same shop

Bent brackets often need a flat mounting pad, a counterbore or a slot that a punch cannot hold. Those features go on a 3-axis or 4-axis mill after forming, using the formed part as the datum so the machined face stays parallel to the frame.

For brackets with tight hole-to-hole tolerance, we machine from solid bar instead of bending sheet. That route costs more per part but removes springback from the tolerance stack. We tell you which route fits before you commit.

  • 1
    Machined tolerance±0.005 mm on critical bores and pads
  • 2
    Max part size4,000 mm on the large-travel machines
  • 3
    InspectionCMM report on request for the first article

Talk to an Engineer

Route selection

Bent Sheet vs Machined Solid: Which Bracket Route Fits

Both routes are run in-house. The choice depends on quantity, tolerance and how the bracket carries load.

ConditionBent sheetMachined solid
Quantity 1–50Setup cost spread over few partsUsually cheaper per part
Quantity 500+Low cost per part, fast cycleCost per part stays high
Hole-to-hole below ±0.1 mmSpringback adds variationHeld directly on the machine
Thickness over 6 mmBending force and cracking riskCut from plate, no forming
Large flat panelsEfficient, low material wasteHeavy stock removal
Outdoor anodized finishGood, edges take dye evenlyGood, sharper edges
What we run

Services Behind a Finished Metal Bracket

A bracket usually needs more than one process. These are the ones we keep under one roof.

01

Sheet Metal Fabrication

Laser cutting, press brake forming and hardware insertion for brackets, panels and enclosures.

02

3 Axis CNC Machining

Flat pads, slots and counterbores on formed brackets, or full machining from plate.

03

4 Axis CNC Machining

Angled faces and multi-side features on brackets that cannot be reached in three axes.

04

CNC Milling & Turning

Spacers, bosses and threaded studs that pair with the bracket in the same assembly.

05

Part Surface Finishing

Anodizing, powder coating, plating, bead blasting and laser marking of part numbers.

06

Rapid Prototyping

One-off brackets for fit checks before the production tooling or flat pattern is locked.

Scope

Bracket Fabrication Scope and Limits

Numbers we can hold without a special review.

ItemCapabilityNote
Sheet thickness0.5 – 6 mmHarder alloys machined instead
Bend angle±0.5°Measured on first article
Machined tolerance±0.005 mmCritical bores and pads
Maximum part size4,000 mmOn large-travel machines
Anodize buildType II and hardcoatClear, color, conductive
Powder coat build60–100 μm per sideMasking on request
Order quantity1 to 10,000+No minimum order quantity
Inspection100% before shipmentReports on request
Why GreatLight

What You Get on a Bracket Order

15Y

Forming and machining since 2011

Three wholly-owned plants in Dongguan and a Singapore factory, 7,600 m² of manufacturing space and 150 technicians.

±0.005 mm

Machining tolerance held in-house

Critical bores, pads and slots are cut and measured on the same site, so the tolerance stack is not split across suppliers.

12 h

Quote and free DFM analysis

You get the price, the process route and any bend or hole warnings within 12 hours of sending the drawing.

24 h

Production can start within a day

Once the drawing and finish are confirmed, material is released and the first operation starts within 24 hours.

3–5 d

Parts ship in three to five days

Standard bracket runs leave the shop in 3–5 days. Historical late-delivery probability is under 2%.

100%

Inspection before shipment

Raw material check, in-process monitoring and final inspection. CMM and roughness reports on request.

7,600 m²Manufacturing space
150Technicians on staff
3Wholly-owned plants
ISO 9001IATF 16949 and ISO 13485
Where brackets go

Bracket Work by Industry

large-die-cast-metal-part-back-19

Automotive and EV

Brackets that hold torque under vibration. IATF 16949 process control, hardness and coating thickness recorded per lot.

  • IATF 16949
  • Torque joints
  • 3–5 day ship
large-die-cast-metal-part-back-5

Robotics and Automation

Sensor and axis brackets where hole position sets alignment. Machined pads keep the mounting face flat and parallel.

  • ±0.005 mm pads
  • CMM report
  • Aluminum 6061
metal-3d-printing-1801

Electronics and Enclosures

Internal chassis brackets with cable routing. Bead blasted and anodized so edges do not cut wire insulation.

  • Bead blast
  • Anodize Type II
  • Edge deburr
FAQs

Questions Engineers Ask Before Ordering Brackets

Should my bracket be bent sheet or machined from solid?

Bent sheet wins on cost once quantity passes a few hundred pieces and the hole tolerance is looser than about ±0.1 mm.

Machined solid wins when hole-to-hole position is tight, when the wall is thicker than about 6 mm, or when the bracket carries load through a machined face. Send the drawing and we will price both routes.

What material should I pick for an outdoor bracket?

5052 or 5083 aluminum bends without cracking and takes anodize well. 6061-T6 is stronger but needs a larger bend radius.

For salt air or washdown, 316 or 316L stainless is the safer choice, with electropolishing if the surface has to stay clean. Zinc plating on plain steel is the low-cost option but the coating is sacrificial.

How do you keep bend angles consistent across a run?

We measure the actual sheet thickness of the material lot and set the bend deduction from that, not from the nominal callout.

The first-off part is checked for angle and hole position before the run continues. Angle tolerance on formed bends is ±0.5°.

Can you mask threads and mating faces before coating?

Yes. Tell us which holes and faces must stay bare and we will plug or tape them before powder coating or anodizing.

Masking is added at the quote stage. If a thread is coated by accident, chasing it by hand removes material from the thread flanks, so masking is the cheaper route.

What finish options do you offer on brackets?

Anodizing in clear, color, hardcoat and conductive types; electroless nickel, zinc, silver and gold plating; powder coating and black oxide; bead blasting, tumbling, brushing and polishing.

Laser marking is available for part numbers and revision codes, with a minimum character height of 1.5 mm.

How fast can I get a bracket order?

Quotation and DFM feedback come back within 12 hours. Production can start within 24 hours of drawing release, and parts ship in 3–5 days.

Historical late-delivery probability is below 2%. If your schedule is tighter than that, say so in the RFQ and we will tell you what is possible instead of promising a date.

Do you have a minimum order quantity?

No minimum order quantity. We run from one prototype to 10,000+ part runs on the same equipment.

Prototype brackets are often a good way to check the flat pattern and hole fit before a production batch is committed.

How do you handle my drawing and NDA?

Uploads are secure and confidential. We can sign your NDA or provide ours before you send files.

Files are used only for quoting and manufacturing the parts you order.

Send Your Bracket Drawing

Upload the drawing and we will return a price, a process route and any bend or hole warnings within 12 hours.

12-hour quote100% inspectionNo minimum order quantityNDA on request

Trusted by engineers and manufacturers worldwide

Tesla Ford Motor Company BYD Auto Denso Magna International Boeing Airbus Medtronic KUKA FANUC