
01
The model is not watertight
Open edges and flipped normals confuse the slicer. It either refuses to slice or fills the part with a shell that leaks powder. We repair the mesh, but a model built as a solid from the start saves a day.
Upload a model and we print it in resin, nylon or metal. Our engineers read the file before printing and tell you where the part will fail, so the first article is worth testing.
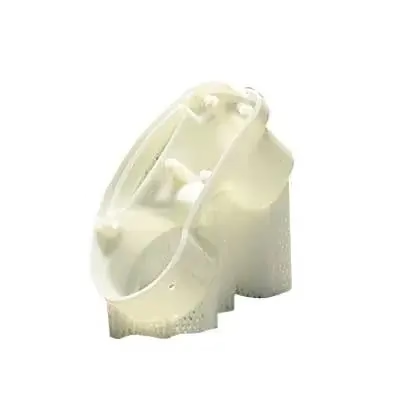
Most failures show up before the printer runs. These four come up in almost every file we review.
Open edges and flipped normals confuse the slicer. It either refuses to slice or fills the part with a shell that leaks powder. We repair the mesh, but a model built as a solid from the start saves a day.
An SLA wall under 0.5 mm curls during post-cure. An SLS wall under 0.8 mm warps in the build chamber. The feature looks fine in CAD and arrives bent. We flag thin walls in the DFM check before anything is built.
As-built surfaces carry layer steps and residual powder. A face that has to seal against an O-ring or a gasket will weep unless it is machined or polished after printing. Decide the sealing face early, not at assembly.
SLS holds around ±0.3 mm on a 100 mm span, and that is before moisture and cooling move the part. If a drawing calls for ±0.05 mm everywhere, the print will not pass inspection. Machine only the critical features.
One file, one review, one route to the printer that fits the geometry.

A print starts with a manufacturability review, not a queue. We open your STL or STEP, check wall thickness, draft, minimum feature size and build orientation, then send a DFM note with the quote. You get the note within 12 hours of upload.
The review is where cost comes out. Rotating a part in the build chamber can cut support volume, and splitting a large housing into two printed halves can remove a support structure that would otherwise need hand work. Small changes to the model usually beat changes to the process.
SLA gives the sharpest detail and the smoothest surface, which suits form-and-fit models, jigs and clear parts. SLS needs no support, so it handles interlocking geometry and living hinges that resin cannot. Metal printing suits small, stiff parts where a machined billet would waste material.
We run all three. That matters when a part changes stage: a housing might be SLA for the first review, SLS for the twenty units used in testing, then machined from aluminium once the design freezes. Same CAD file, different route.
Match the geometry and the load case to the process.
| Process | Use it when | Avoid it when |
|---|---|---|
| SLA resin | Smooth skins, fine detail, fit checks | The part sees heat above 60 °C |
| SLS nylon | Interlocking shapes, no support allowed | You need a glass-like surface |
| Metal printing | Stiff small parts, complex internal channels | The part is large and simple |
| CNC after printing | Critical faces need tight tolerance | The whole part is already in spec |
One shop for printed parts and the machining that finishes them.
Resin parts with fine feature detail and a smooth surface. Used for fit models, clear covers, jigs and small enclosures.
Nylon parts built without supports. Handles snap fits, living hinges and small production batches for test rigs.
Titanium and stainless parts where stiffness and heat resistance matter more than surface finish.
Printed prototypes paired with machined or sheet metal parts to build a working assembly faster.
Critical faces, bores and threads cut after printing so the mating dimensions hold to ±0.005 mm.
Bead blasting, polishing, painting and laser marking to match the look of the production part.
Numbers you can put in a request for quote.
| Item | Range | Included |
|---|---|---|
| Part size | Up to 4,000 mm on the machining side | Build orientation review |
| Tolerance | ±0.005 mm on machined features | Inspection report on request |
| Batch size | One prototype to 10,000+ parts | No minimum order quantity |
| Lead time | Quote in 12 hours, parts ship in 3–5 days | 100% inspection before shipment |
The reason most printed parts stop being prototypes is that nobody can finish them.
Fifteen years of prototypes and low-volume runs across aerospace, automotive, medical and robotics work.
Printed parts move to a mill or lathe in the same building when a face needs to be flat or a bore needs to be round.
Printed geometry stays as printed. Critical features are cut to ±0.005 mm with surfaces from Ra 0.2 to 0.8 μm.
Files get read within twelve hours. Production can start within 24 hours of approval.
ISO 9001, IATF 16949, ISO 13485 and ISO 27001. Reports issued on request.
One prototype or ten thousand parts. Uploads stay confidential, with an NDA available on request.
Underhood parts need heat resistance and a consistent fit. Printed brackets are used for test builds, then machined once the design freezes.
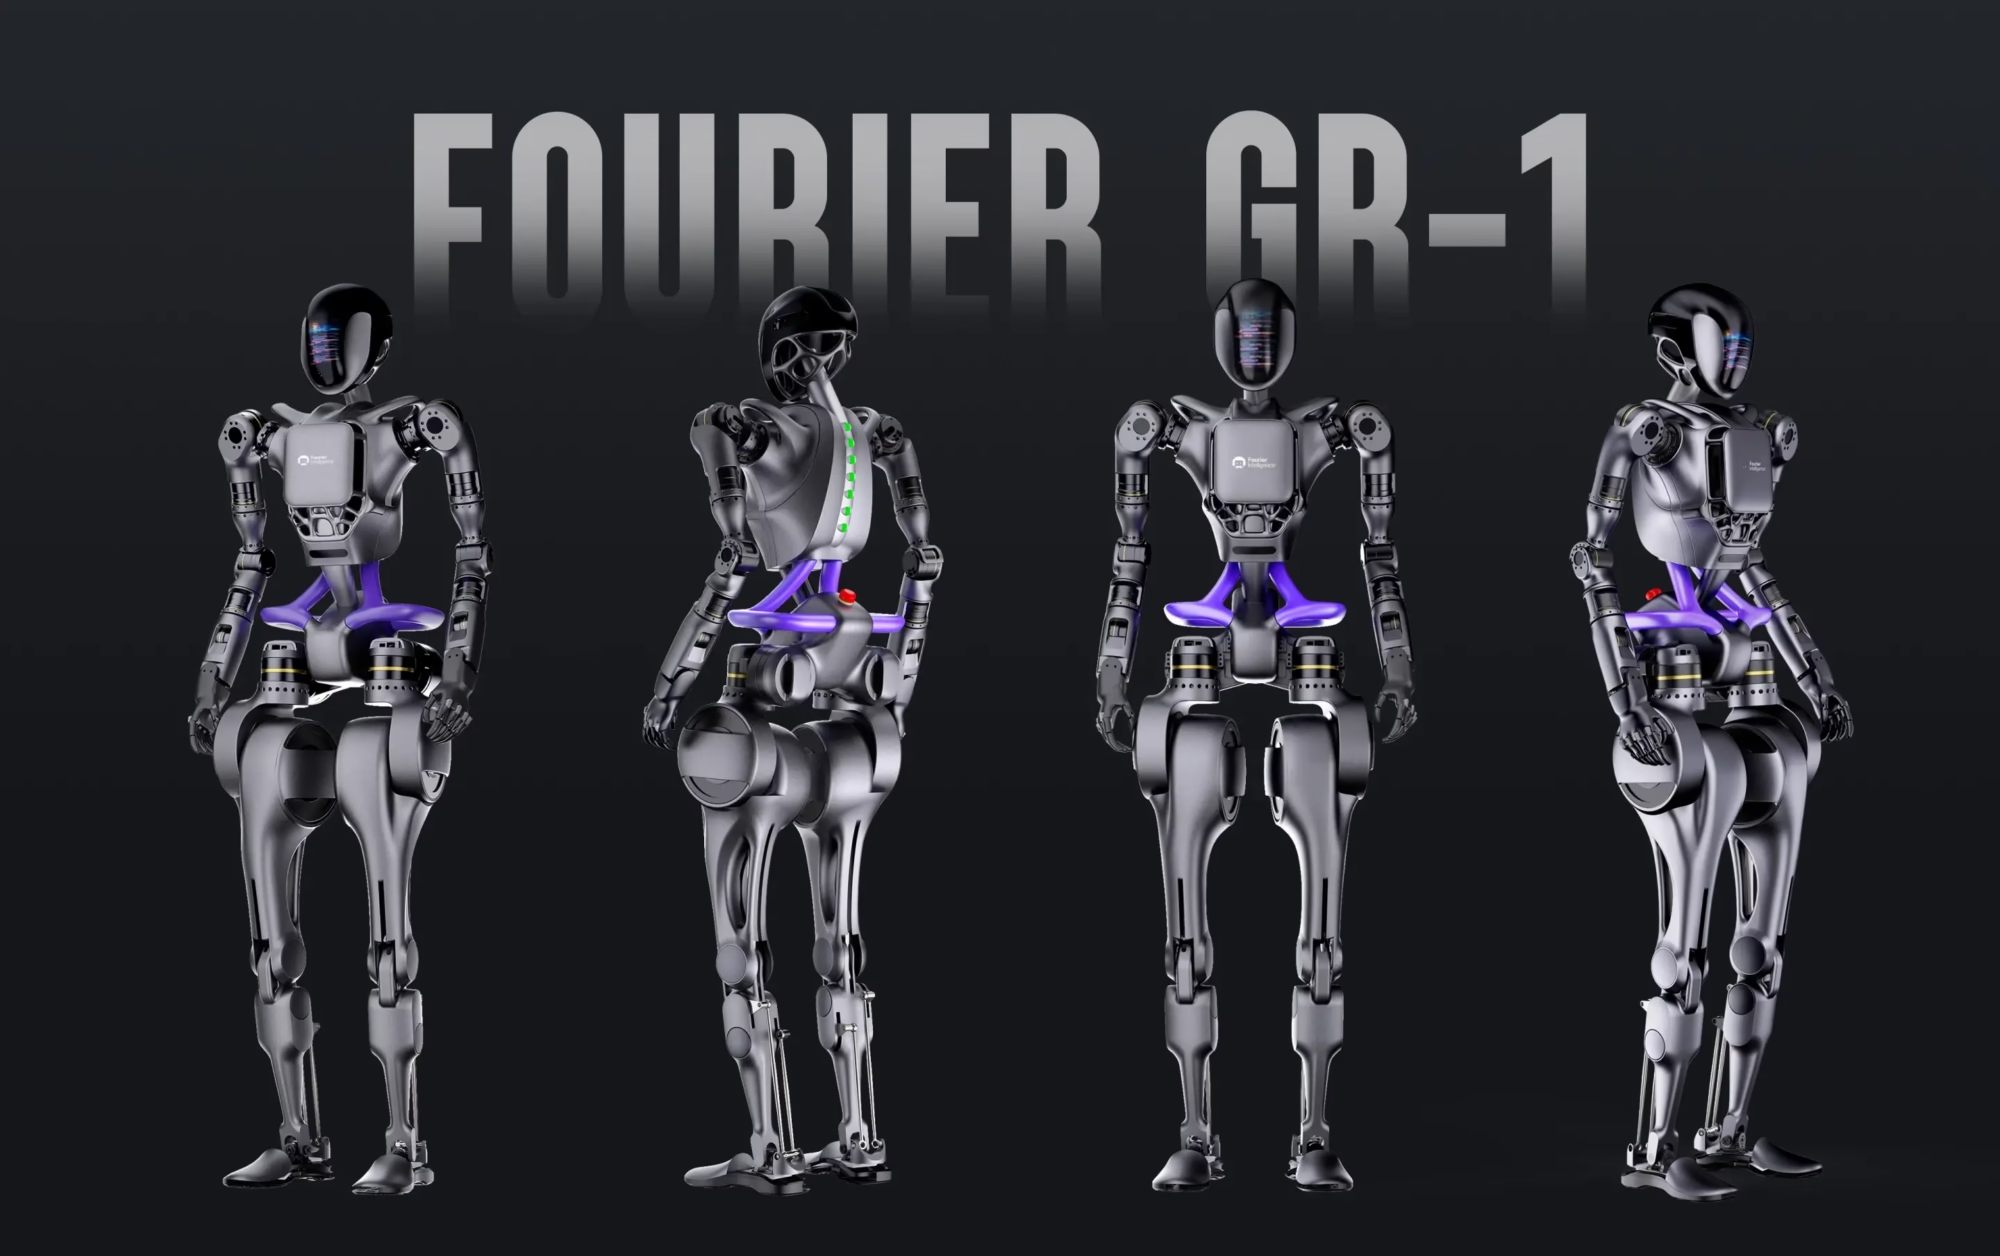
End effectors and gripper jaws change shape every week. SLS nylon keeps a light arm light while the geometry is still moving.

Housings and fixtures need clean surfaces and traceable records. We keep material certificates with the batch.
Print when the geometry is complex, the quantity is low, or the design is not frozen. Internal channels, hollow ribs and organic shapes cost nothing extra to print.
Machine when the load path is heavy, the tolerance is tight, or the material has to be a specific alloy. Printing in metal is slower and rougher than cutting from a billet.
Not as printed. SLS holds roughly ±0.3 mm on a 100 mm span, and resin parts shrink during cure.
We reach ±0.005 mm by machining the critical features after printing. That works when the part has enough wall to take a cut and a face that can be held in a vise or fixture.
STL or STEP. STEP is better when you want us to check exact dimensions rather than a triangulated mesh.
If the mesh has holes or flipped normals, we repair it before slicing. Sending the native CAD file helps us rebuild a feature that is too thin to print.
Strong enough for brackets, housings, snap fits and gripper jaws in low-load use. The part is not solid: layer adhesion makes it weaker across the build direction than along it.
Set the build orientation so the load runs along the layers, not across them. Tell us how the part is loaded and we will orient it that way.
SLA parts are printed on supports, which we cut and sand. SLS parts come out of a powder bed and need bead blasting.
If the part has to look like a production part, we can polish, paint or bead blast it. Tapped holes and sealing faces are cut after printing.
For SLA, walls down to about 0.5 mm and features around 0.2 mm. For SLS, walls down to about 0.8 mm.
Below those numbers the feature prints, but it distorts during cooling or post-cure. We flag it in the DFM note instead of printing something that will not measure.
Quotation and DFM feedback come back within 12 hours. Production can start within 24 hours of approval, and parts ship in 3–5 days.
That timing depends on the process and the post-processing. Machined features and finishing add a step, which we state in the quote.
Yes. Uploads are kept secure and confidential, and we can sign your NDA or provide ours before you send files.
For parts under development, we can restrict the file to the engineers who quote and produce it.
Tell us how the part is used and we will name the process, the tolerance it holds and the cost.
12-hour quote100% inspectionNo minimum orderNDA on request
Trusted by engineers and manufacturers worldwide










Upload your 3D model or 2D drawing and get a quotation with a free DFM analysis. Maximum processing size 4,000 mm.
CNC Metals 13 grades
CNC Plastics 10 grades
Machines & processes 12 options
Surface & post-processing 10 options
Material: not selected Machine: not selected Post-process: not selected
Fill in this short form and we'll open WhatsApp with your message ready to send. We only use these details to reply to you.
Nothing is sent until you press send inside WhatsApp.