
7 CNC Machining Tips to Slash Production Costs
Most of a machined part's cost is fixed before the first chip is cut: geometry, tolerances, material and setup count. This guide walks through seven decisions that lower unit cost without lowering quality, written for design engineers and sourcing teams who review quotes. Read it and you can tell which features on your drawing are driving the price.
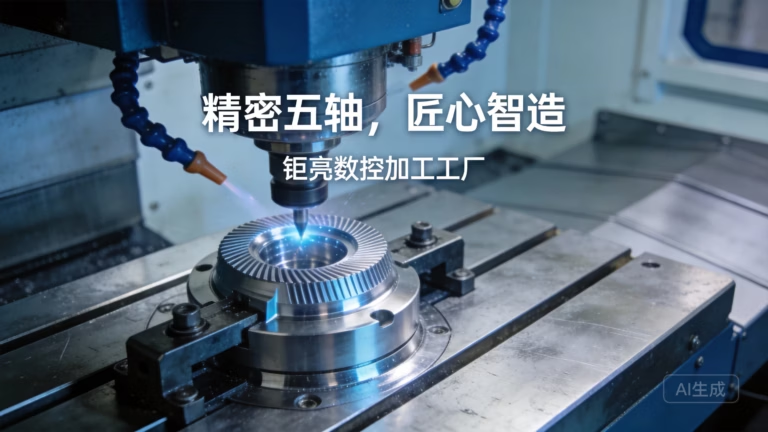
Cost is decided at the drawing, not at the spindle
Machine time, setup, tool wear and inspection all trace back to a handful of choices made before quoting.
Apply DFM before you request a quote
The largest single cost driver in CNC machining is complexity, and complexity usually comes from features that do not need to exist. A deep pocket with a 3 mm corner radius, a tolerance called out on a non-functional face, a hole that needs a custom reamer: each one adds setup time, tool changes and inspection. Standard ±0.1 mm is enough for most mating surfaces. Calling ±0.01 mm everywhere adds measuring time and scrap without adding function.
A useful habit is to mark every dimension on the drawing as critical or reference. Critical means the part fails without it. Reference means the machinist can hold it loosely. When we review a model, the features that jump out are almost always the same: sharp internal corners, threads deeper than twice the diameter, thin walls under 1 mm, and text smaller than the minimum character height of 1.5 mm for laser marking.
Ask for a DFM review before the quote is finalized, not after the first article fails. Our engineering team returns quotation and free DFM analysis within 12 hours, and the feedback lists specific high-cost features with suggested alternatives. Resolving those points on paper costs nothing; resolving them after tooling is cut costs real money.
- 1Corner radiiMatch the radius to the largest cutter that can reach the pocket floor.
- 2Tolerance scopeReserve tight tolerance for functional fits only, not for every face.
- 3Wall thicknessKeep walls above 1 mm in aluminum to avoid chatter and rework.
- 4Thread depthThreads deeper than 2 × diameter need special taps and raise risk.
Pick material by machinability, not by raw price alone
Raw material price is only part of the number. A cheap alloy that cuts slowly, wears tools and forces light feeds can cost more per part than a pricier grade that machines fast and holds tolerance. Aluminum 6061-T6 is the default for good reason: it cuts cleanly, takes anodizing well and holds ±0.005 mm on stable setups. 7075 is stronger and more expensive, and it is noticeably harder on tooling.
Stainless 303 machines far better than 304 or 316, and the cost difference in cycle time often outweighs the material premium. For 17-4PH, expect slower speeds and more frequent insert changes. Titanium TC4 (Ti-6Al-4V) and Inconel sit at the difficult end: low thermal conductivity, high tool wear, and a strong case for near-net-shape preforms before final CNC finishing.
One practical route for expensive alloys is to start close to final shape and machine only the critical surfaces. We run hybrid workflows that combine SLM 3D printing with CNC finishing, and metal die casting for higher volumes, so the expensive material is only removed where the tolerance demands it.
- 1Easy to cut6061-T6, 6082, 2024, brass C36000, POM.
- 2Moderate303 and 17-4PH stainless, 4140, 4340, titanium TA2.
- 3Difficult316L, Inconel, TC4, magnesium AZ91D.
Relative cost index by material and process choice
Indices are relative, not quoted prices. A lower index means less machine time and tool wear per part.
| Material or route | Relative material cost | Relative machining cost |
|---|---|---|
| Aluminum 6061-T6 | Low | Low |
| Aluminum 7075 | Medium | Medium |
| Stainless 303 | Medium | Medium |
| Stainless 316L | Medium | High |
| Steel 4140 | Low | Medium |
| Titanium TC4 | High | High |
| Inconel | High | Very high |
| SLM preform + CNC finish | High | Medium |
| Die casting + CNC finish | Low at volume | Low |
Simplify geometry and cut the number of setups
Cycle time tracks the volume of material removed and the number of tool engagements. Deep pockets, long slender tools and tight internal radii all force light passes. Give the cutter room: a pocket floor radius of 3 mm or more lets a larger tool run at a heavier feed. Design parts so the majority of features are reachable from one direction, and avoid features on five faces if three will do.
Setup is where small batches lose money. Every additional orientation means another fixture, another dial-in, another first-article check. Parts that can be held in a vise or a standard chuck, with a flat datum face and a clear zero point, run far cheaper than parts that need custom soft jaws. When a part needs work on several faces, batch it so all parts get the same operation before the fixture changes.
Keep a consistent datum across operations. If the drawing changes datum between milling and turning, the machinist has to re-establish position, and error stacks up. For turned parts, a Ø400 mm rotary table and mill-turn centers let us complete milling and turning in one setup, which removes a handling step and a re-clamping error source.
- 1Pocket radiusUse at least 1/3 of pocket depth as the corner radius.
- 2Hole depthKeep depth under 4 × diameter where possible.
- 3DatumOne primary datum carried through every operation.
- 4Batch sizeGroup identical operations to share the setup.
Specify only the surface finish the part actually needs
Finish is the easiest line item to over-specify. As-machined surfaces at Ra 1.6–3.2 μm are fine for brackets, housings and internal structure. Ra 0.8–1.6 μm covers most sealing faces and sliding contacts. Ra 0.2–0.8 μm is a lapping or fine-boring operation and belongs only on optical, hydraulic or bearing surfaces. Applying the fine finish across a whole part can multiply the finishing cost for no functional gain.
Add finishing notes per face, not per part. If a shaft journal needs Ra 0.4 μm, say so on that diameter and leave the rest as machined. The same logic applies to coatings: anodizing a whole bracket when only the mounting face needs wear resistance is money spent on appearance. For color and corrosion, clear or colored anodizing is usually enough. Hardcoat adds cost and should be reserved for wear surfaces.
Bead blasting, tumbling and brushing are inexpensive ways to even out tool marks. Laser marking has a minimum character height of 1.5 mm, so plan part numbers and traceability marks around that limit rather than asking for micro-text after the fact.
Use 5-axis where it removes a setup, and consolidate suppliers
Five-axis machining is not automatically cheaper. It pays off when it removes setups, not when it replaces a simple 3-axis job that was already efficient. An angled hole, a contoured pocket on a sloped face, or a part that would otherwise need three fixtures can be cut in one fixturing. For complex geometry, that single setup often removes more cost than the higher hourly rate adds.
We run 16 simultaneous 5-axis machining centers alongside 27 three-axis machines, 12 four-axis mills and 16 mill-turn centers. That mix matters: a shop with only 5-axis equipment will quote everything on 5-axis, and you pay for capability you did not need. Matching the process to the part is part of keeping the price down.
Secondary operations are another hidden multiplier. If milling, turning, finishing and inspection happen at four vendors, you pay for four setups, four freight legs and four quality records. Keeping the work under one roof means one process plan and one inspection report. Our 127 machines across 3 wholly-owned plants cover milling, turning, surface finishing and inspection with 100% inspection before shipment.
- 1Use 5-axisAngled features, contoured surfaces, parts needing three or more orientations.
- 2Stay 3-axisPrismatic parts with features reachable from one or two faces.
- 3ConsolidateOne supplier for machining, finishing and inspection cuts handling.
Questions engineers ask before releasing a quote
How tight a tolerance do I actually need to quote?
Start from function. If a feature does not mate, seal or locate, it does not need a tight callout. Standard ±0.1 mm is sufficient for most non-functional faces.
Where fit matters, we hold ±0.005 mm (±0.0002 in) on stable setups. Tightening tolerance across a whole drawing raises inspection time and scrap rate, so scope it to the features that use it.
Does a small batch cost more per part, and is there a minimum order?
Per-part cost is higher at low volume because setup is spread over fewer parts, but the setup itself does not change much between one part and fifty.
We have no minimum order quantity. Runs go from a single prototype to 10,000+ parts. If you expect volume later, batching the first run at a slightly higher quantity usually lowers your average unit cost.
When should I choose 5-axis over 3-axis?
Choose 5-axis when the part has angled holes, contoured surfaces or features on faces that would need three or more separate fixtures on a 3-axis machine.
If the part is prismatic and most features are reachable from one direction, 3-axis is faster and cheaper. We quote both routes when the geometry sits in between.
How much does surface finish add to the part price?
As-machined surfaces carry no extra operation. Fine finishes such as Ra 0.2–0.8 μm add a separate pass, sometimes hand work, and raise cost per finished area.
Specify finish per face. A single sealing surface at Ra 0.4 μm on an otherwise as-machined part costs far less than the same callout applied across the whole component.
Can you reduce cost by starting from a casting or printed preform?
Yes, for expensive alloys and for parts with a lot of removed volume. A near-net-shape preform leaves less material for the cutter to clear, which cuts cycle time and tool wear.
We support die casting and SLM 3D printing as preform routes, then finish critical surfaces by CNC to the required tolerance.
What do you need from us to return a DFM review?
A 3D model in STEP or IGES plus a 2D drawing with tolerances, material and finish notes. Mark critical dimensions if the drawing is not fully defined.
Quotation and free DFM analysis come back within 12 hours. Uploads are secure and confidential, and an NDA is available on request.
Send the model and see which features are driving the price
Quotation and free DFM analysis within 12 hours. No minimum order quantity, from one prototype to 10,000+ parts.
12-hour quoteFree DFM analysis±0.005 mm100% inspection









